Kundenspezifische Laserzuschnitt-Dienstleistungen für OEM-Metallteile
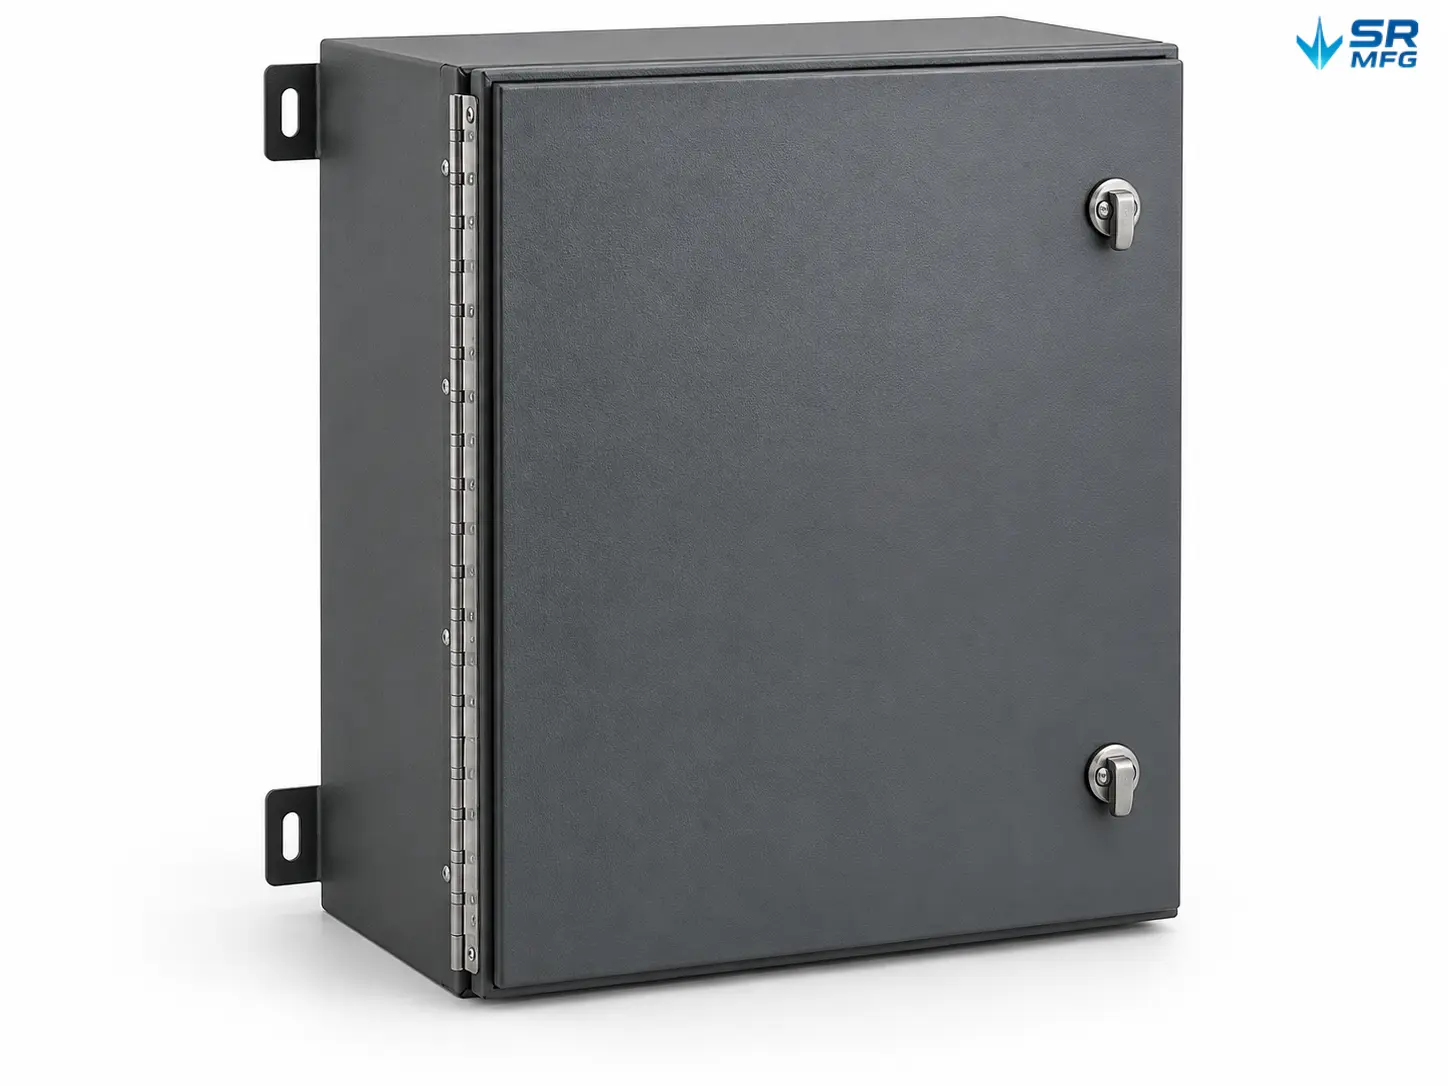
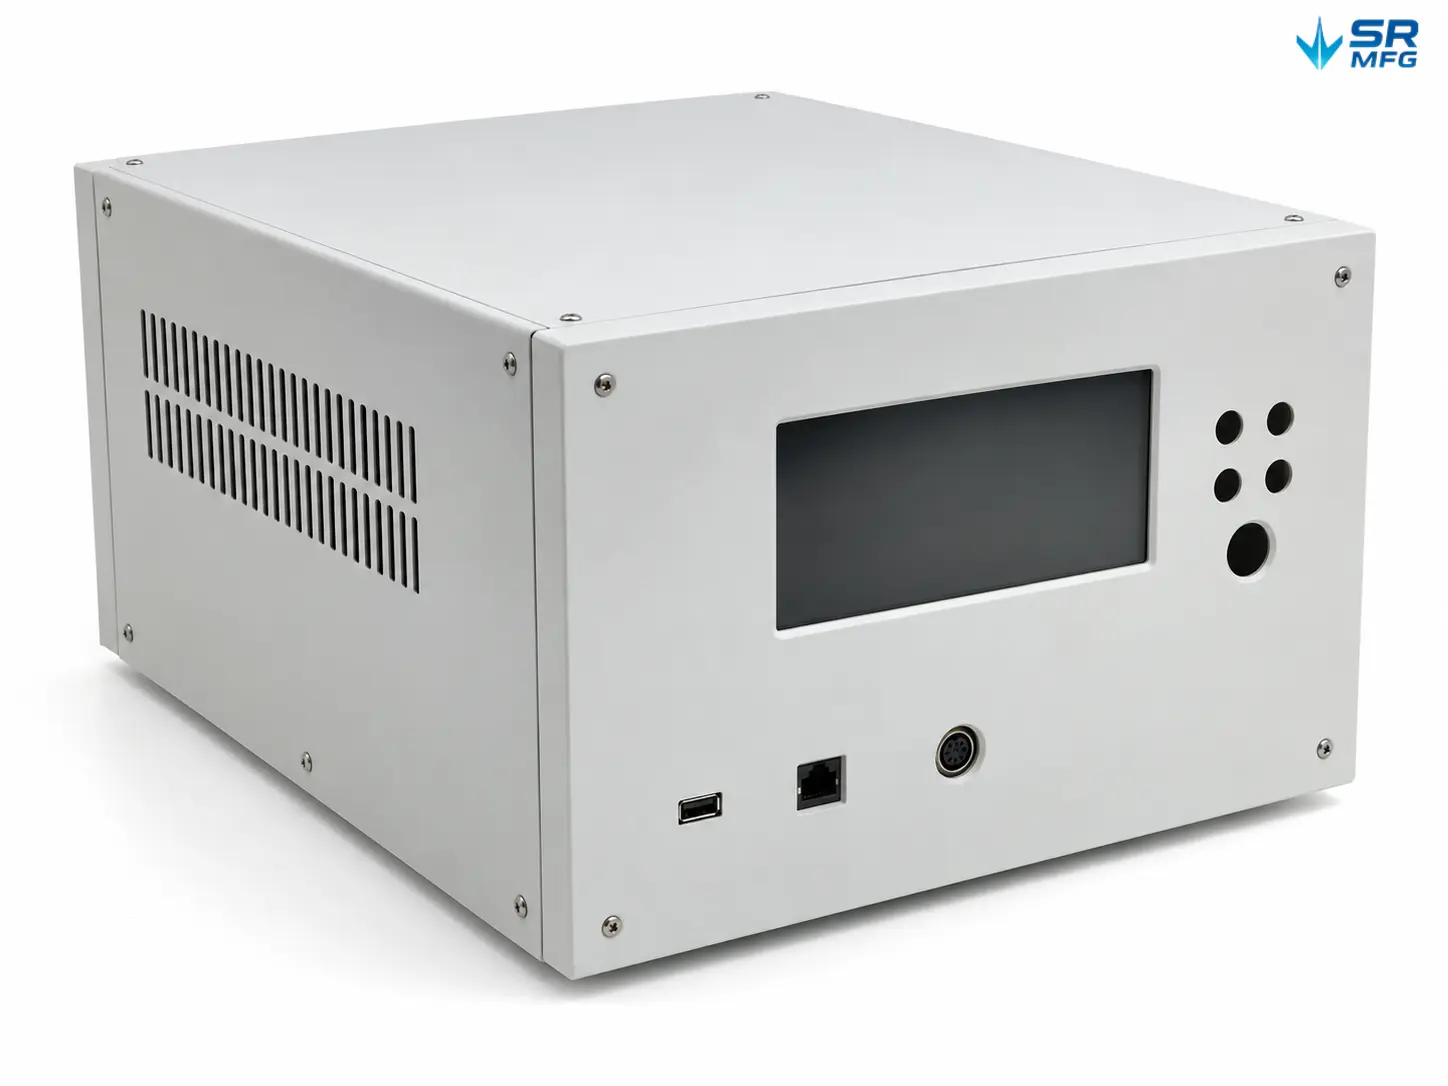
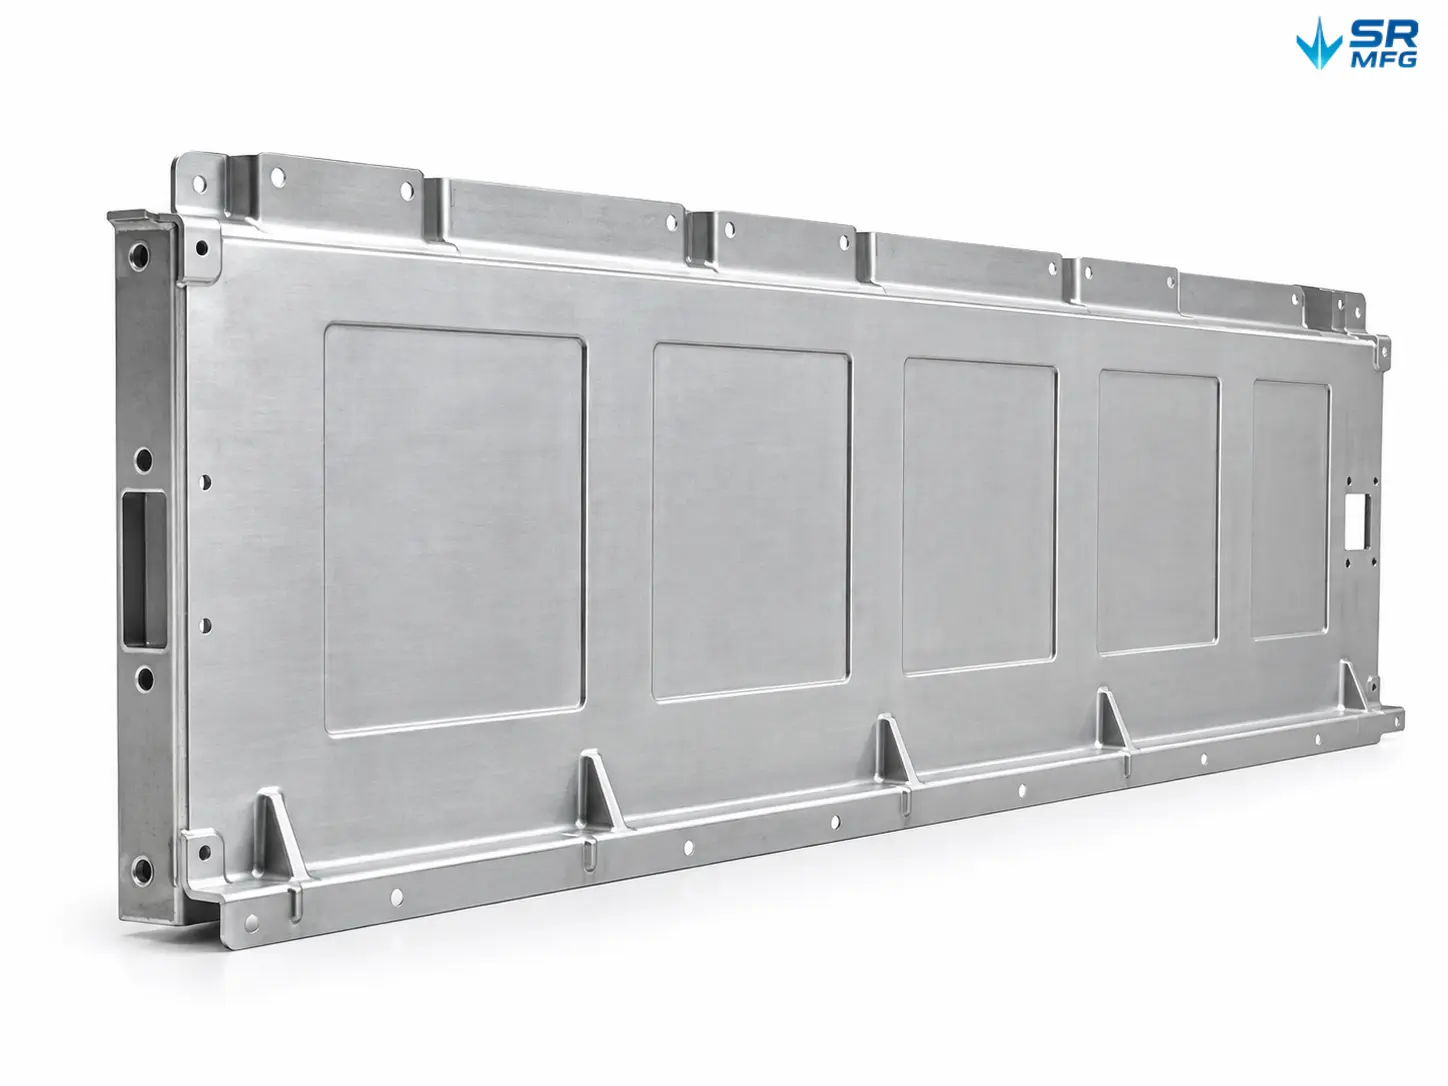
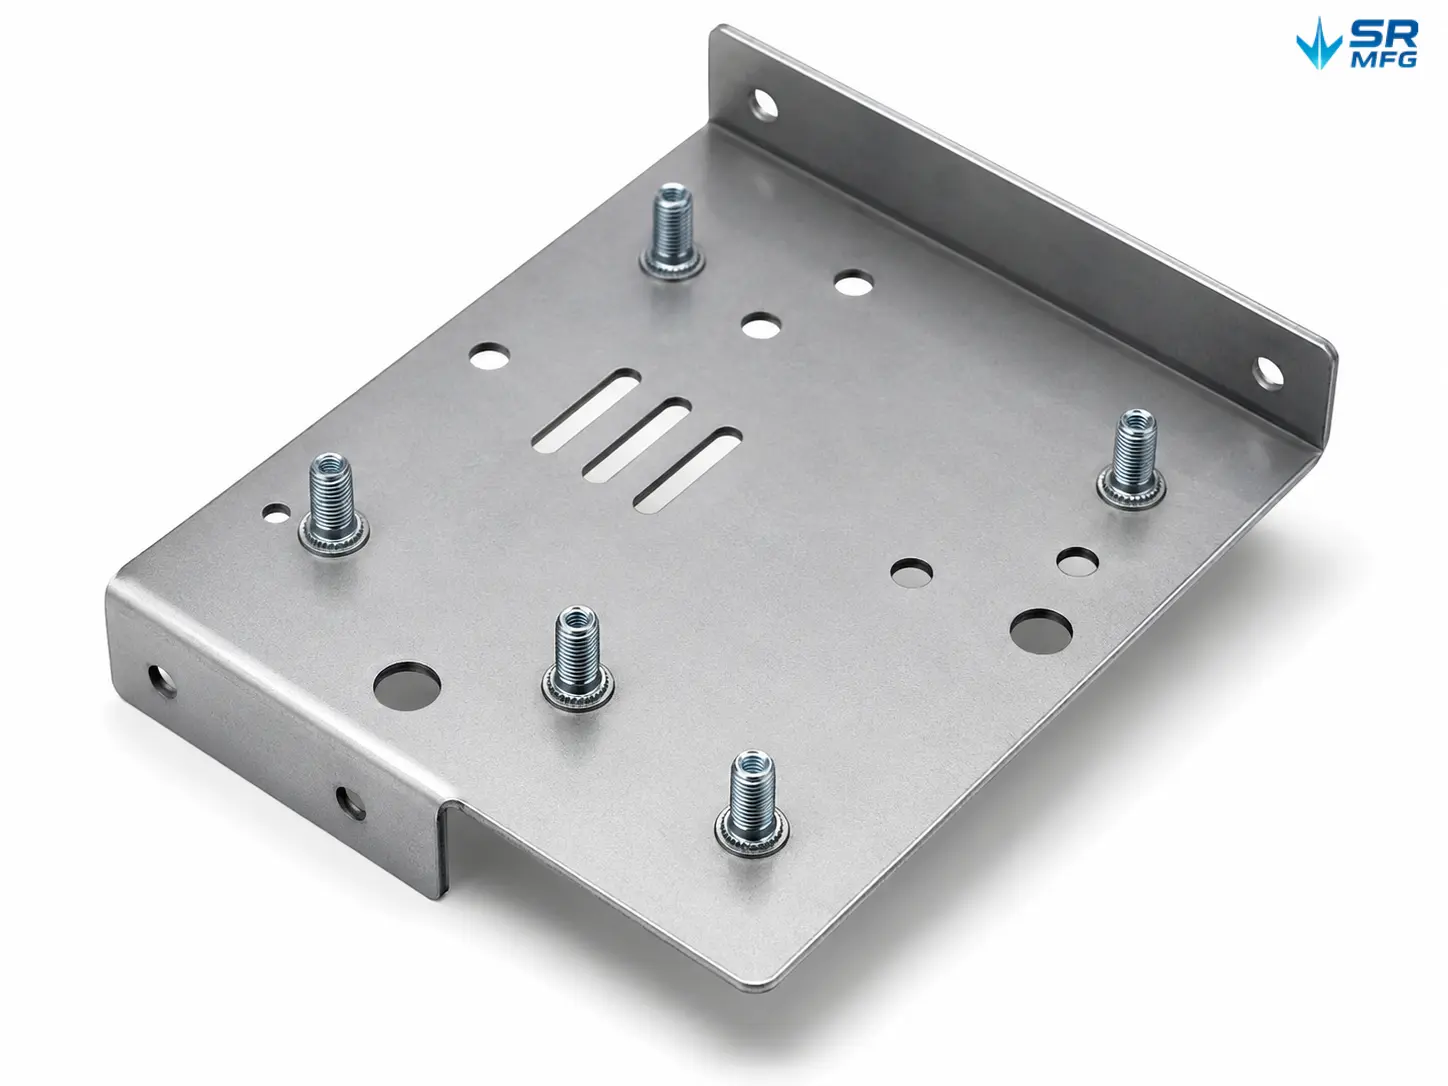
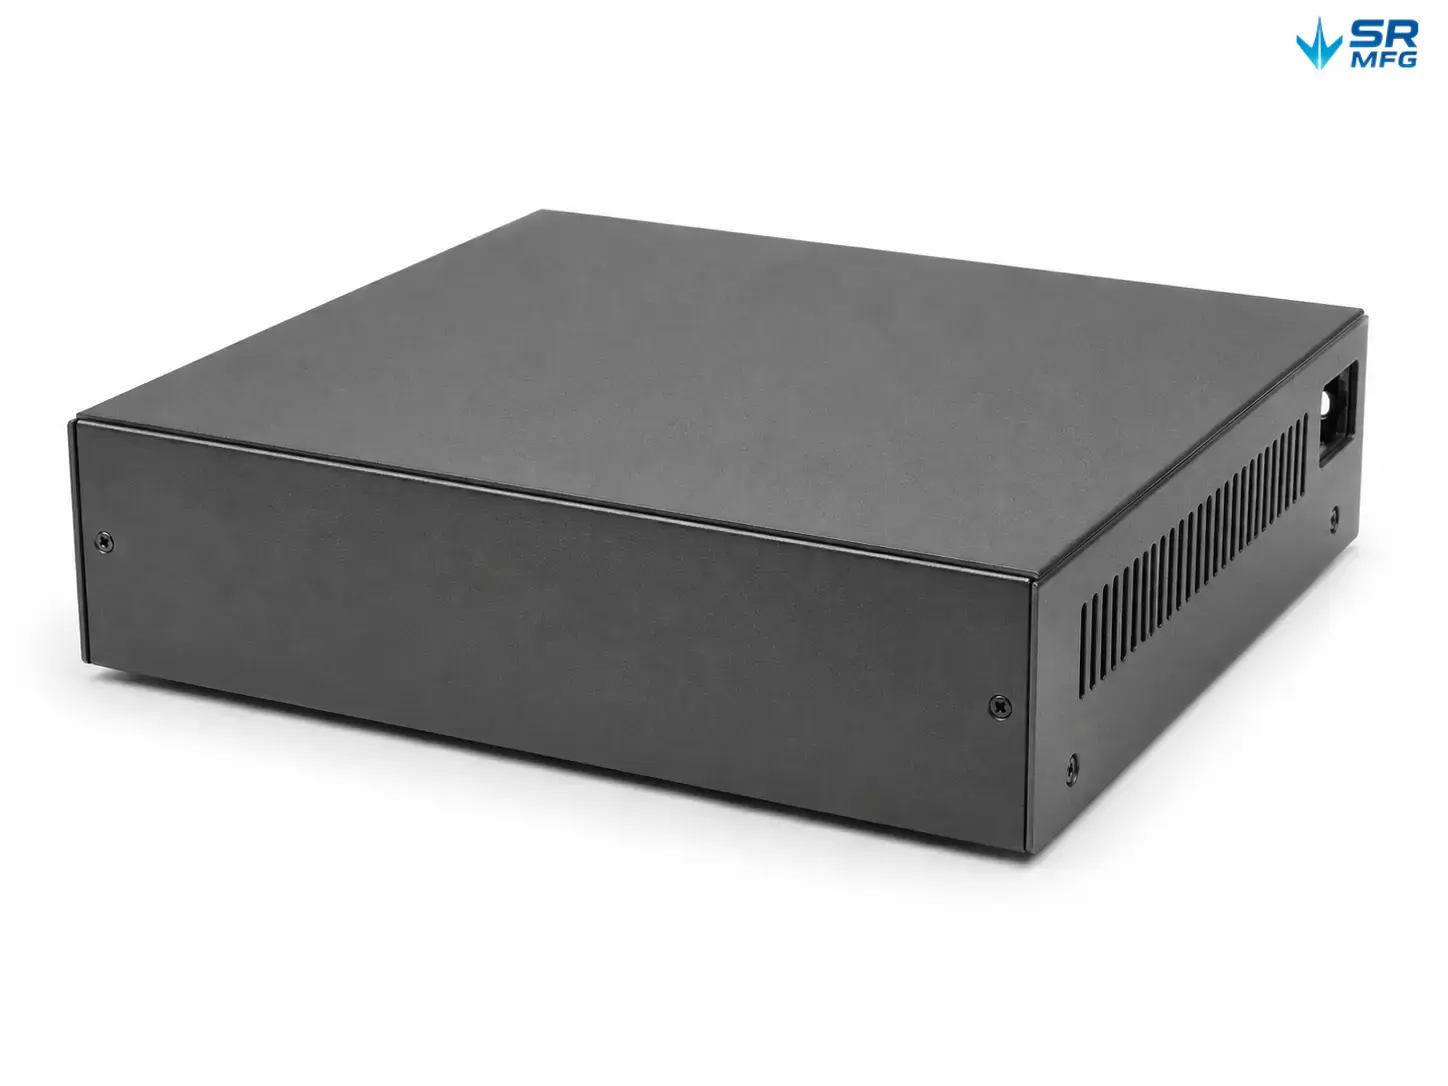
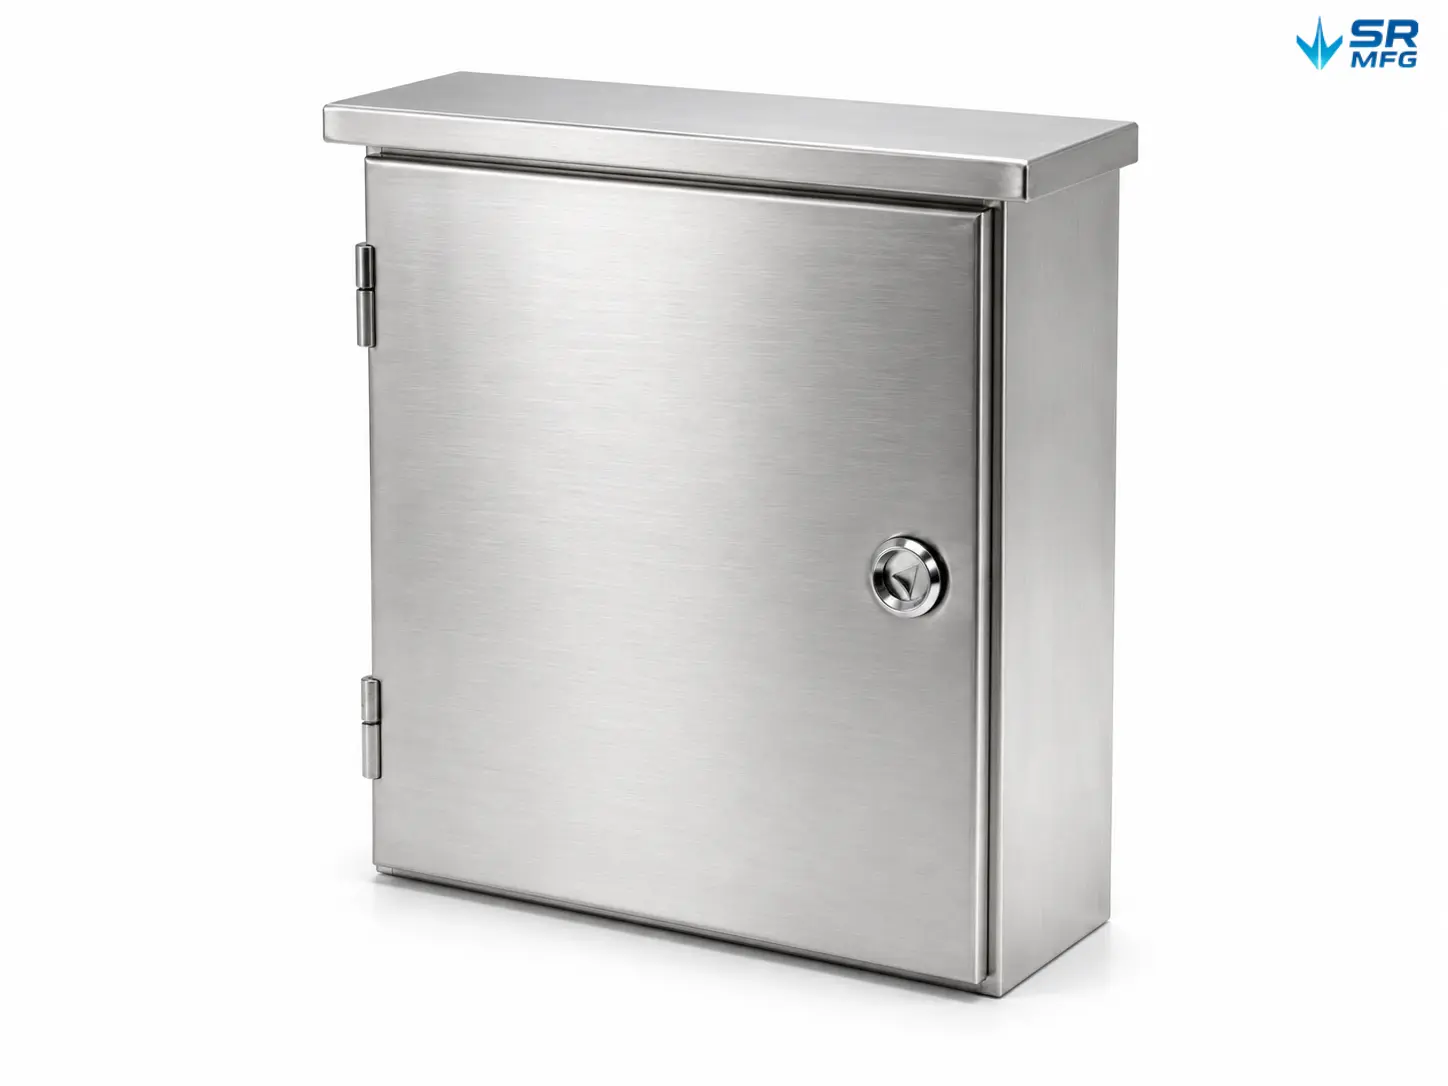
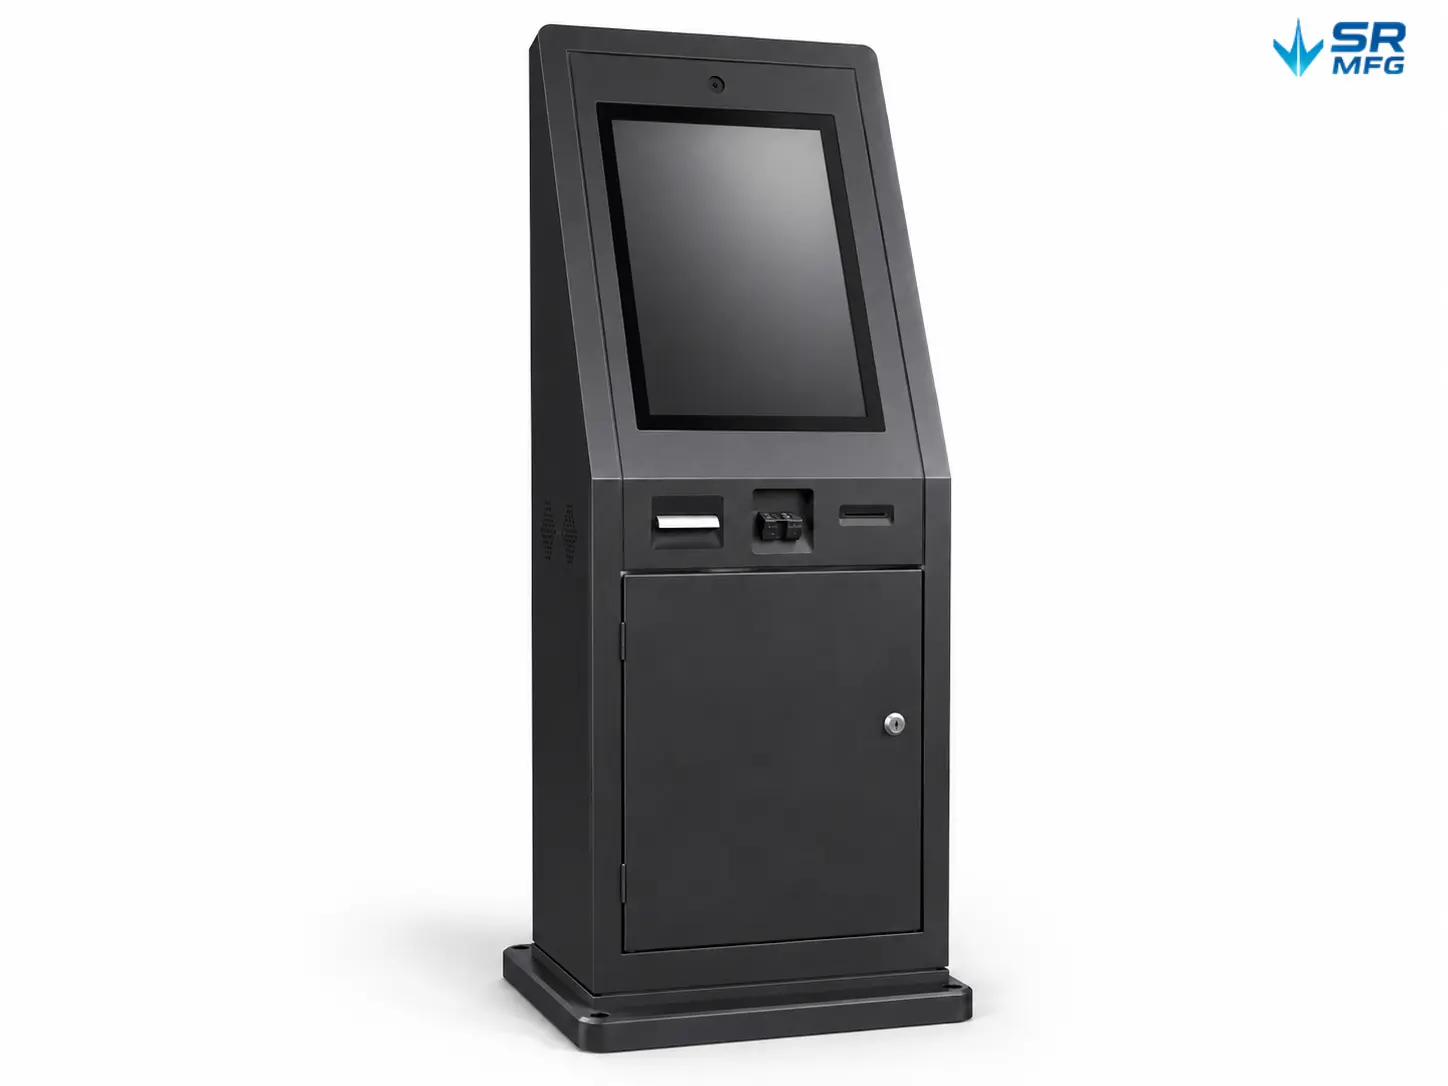
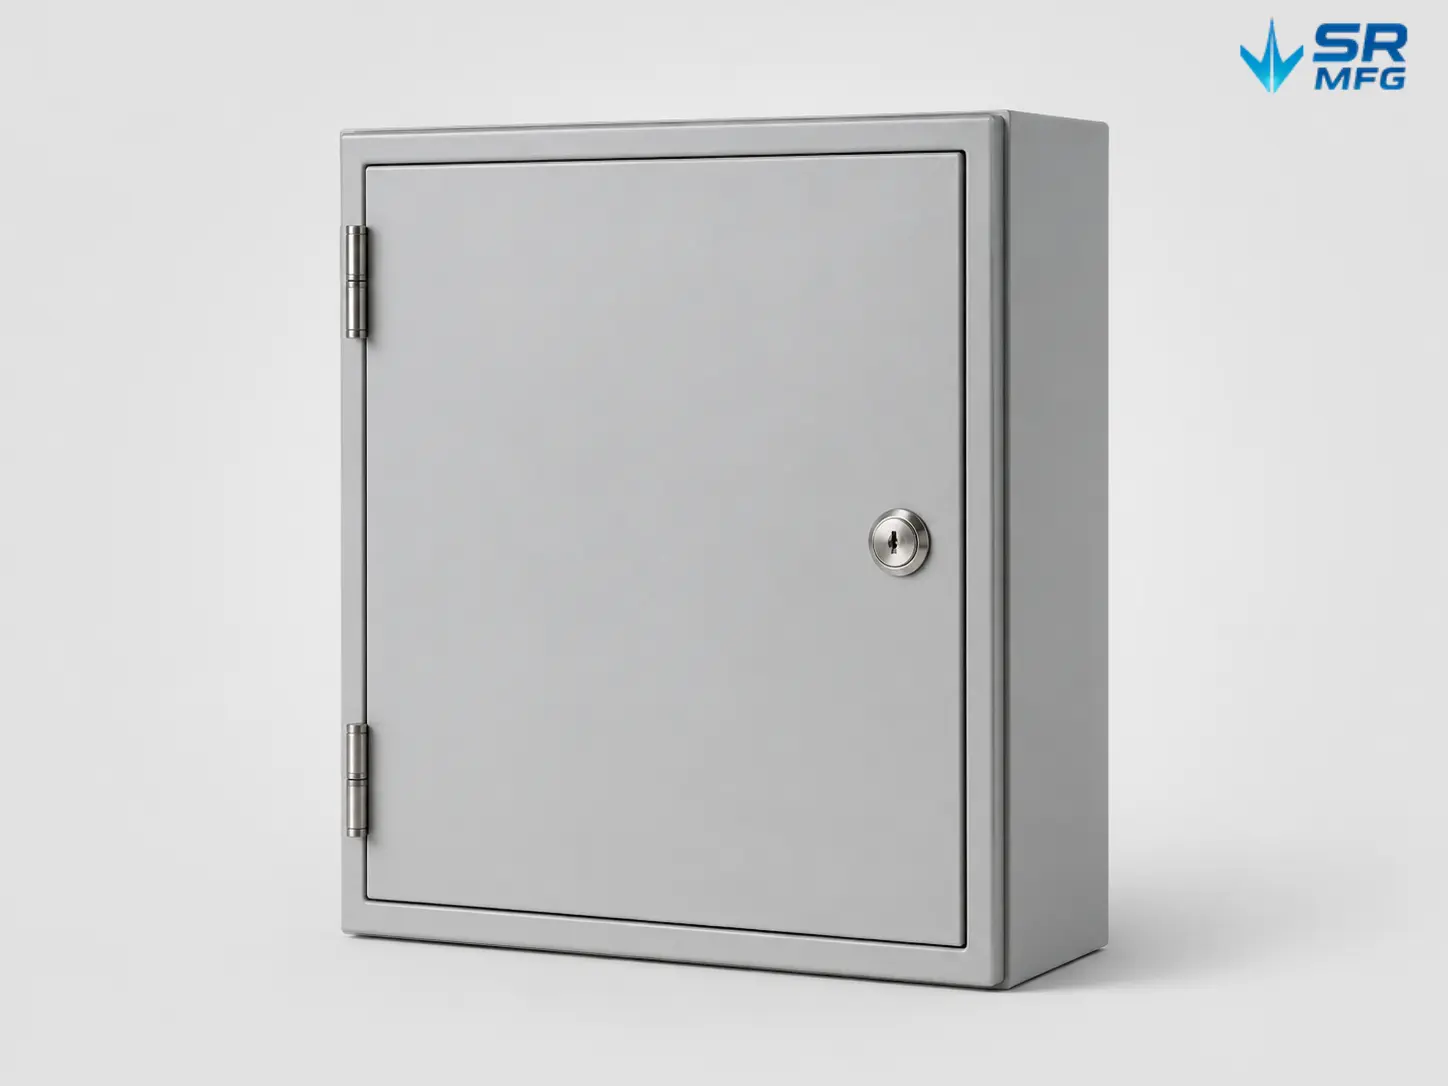
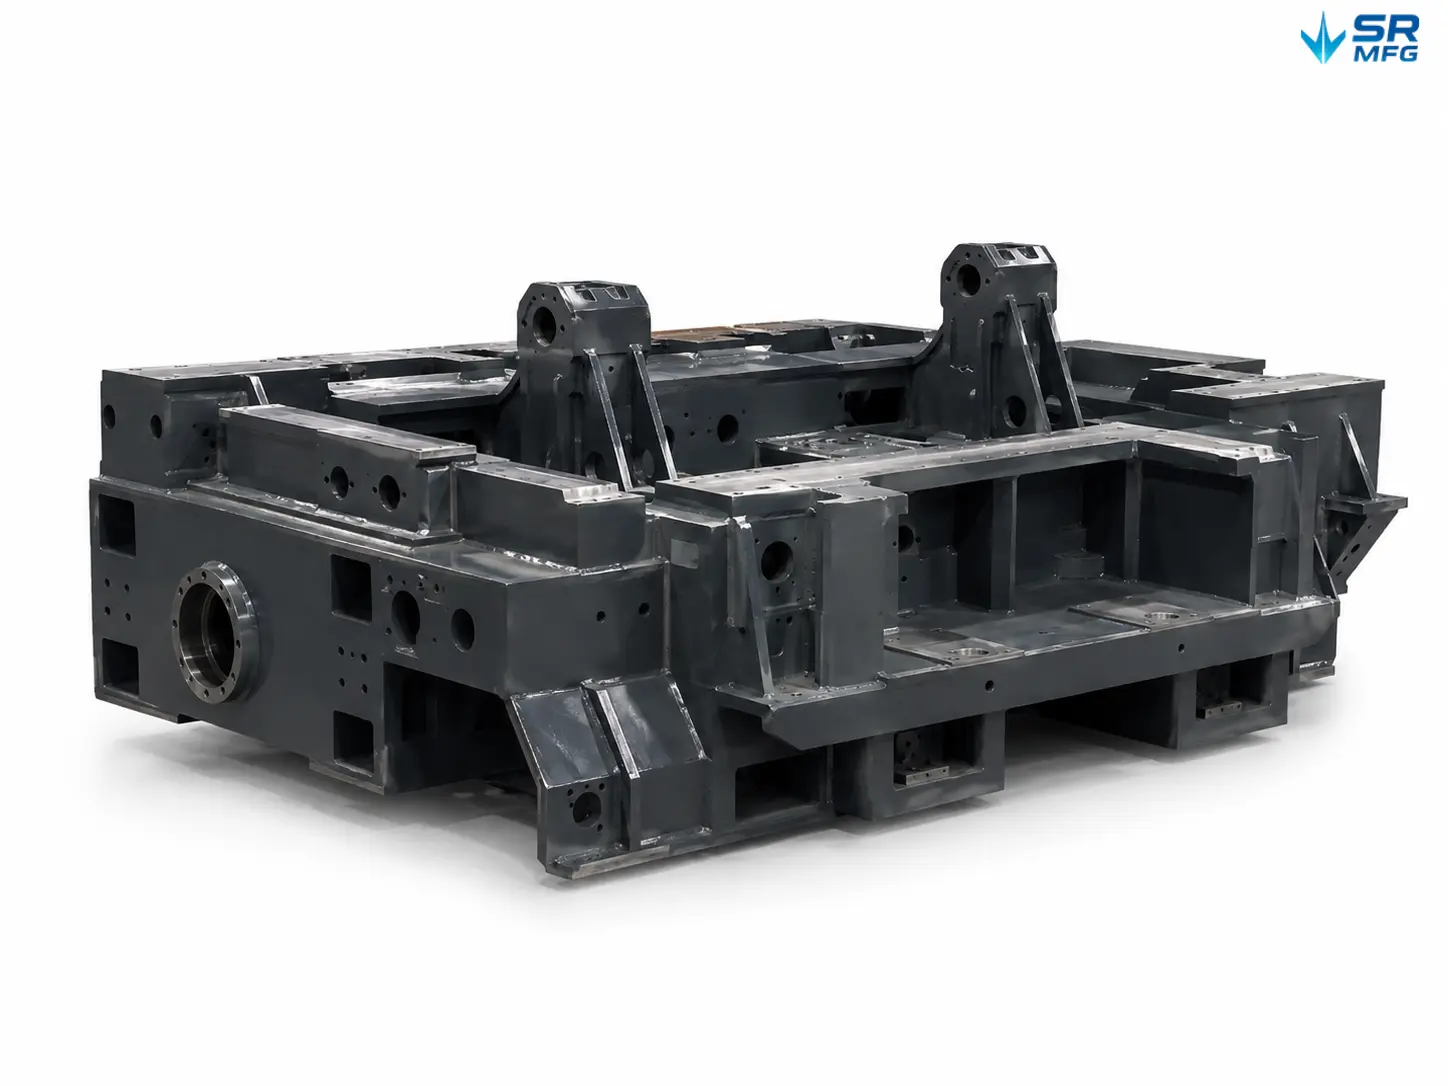
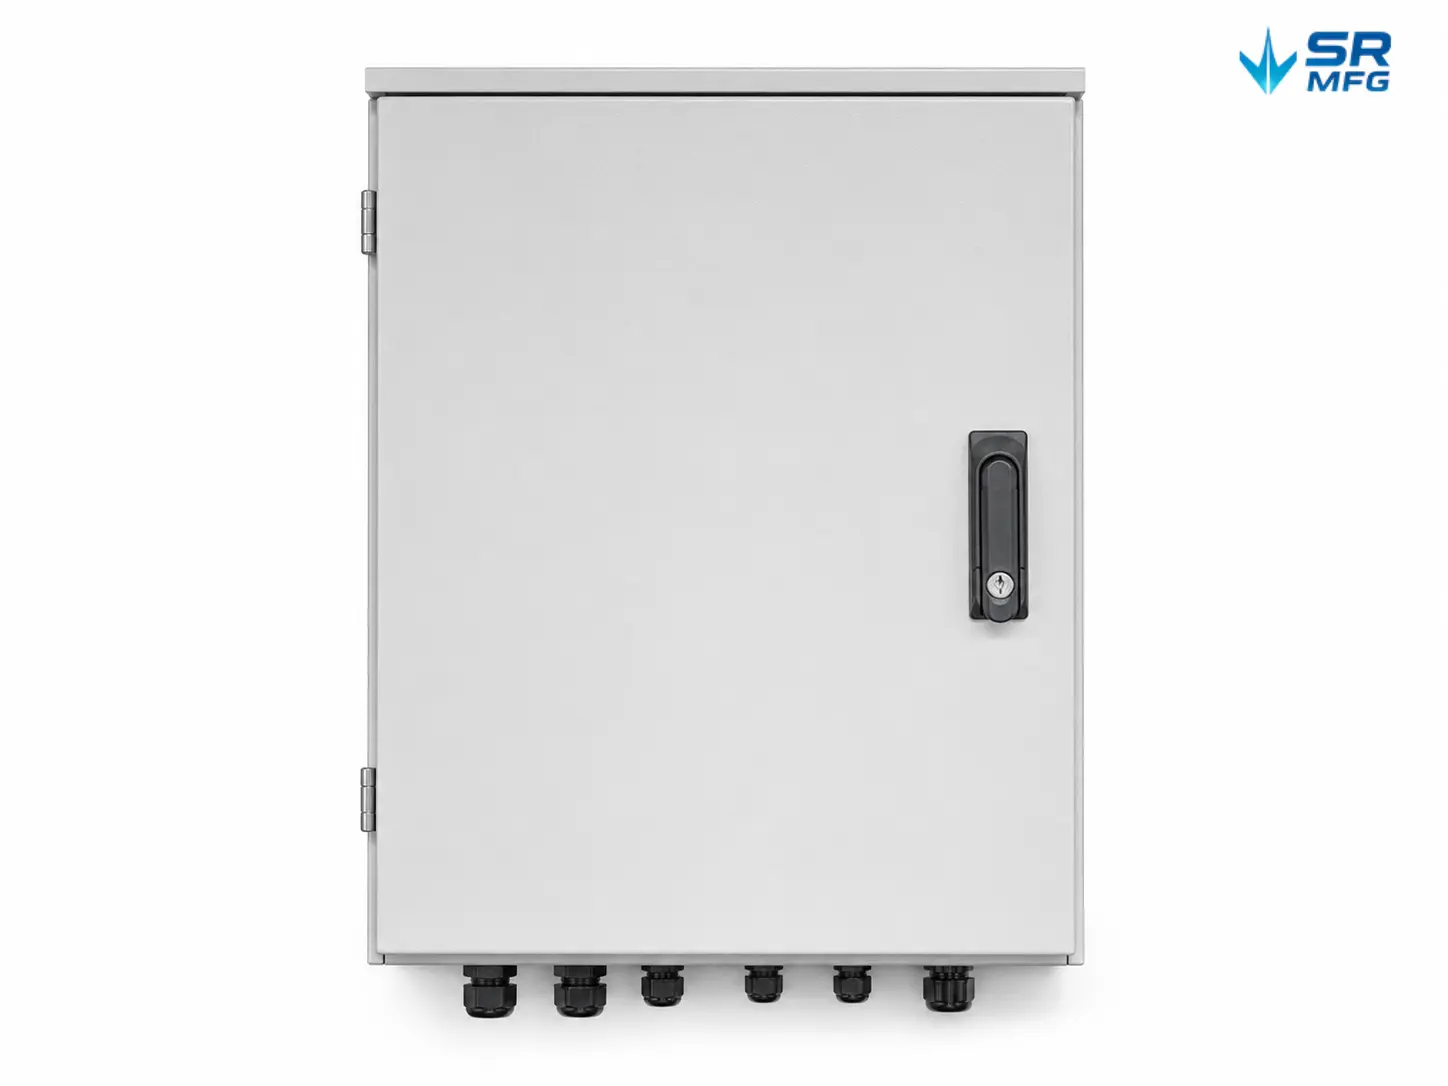
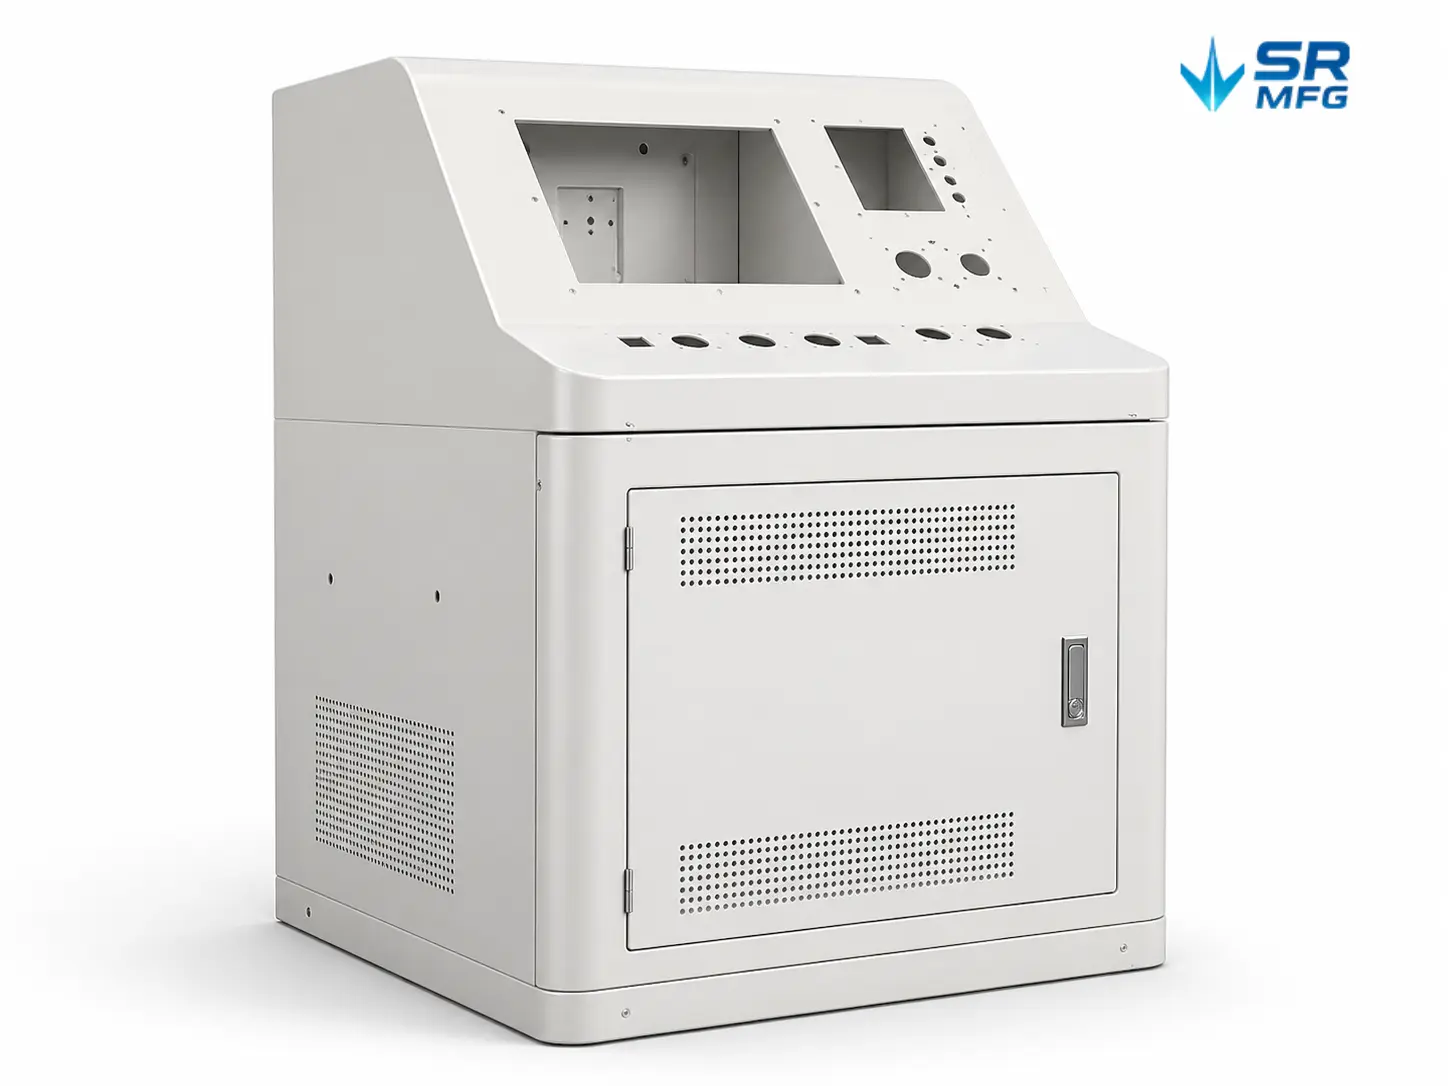
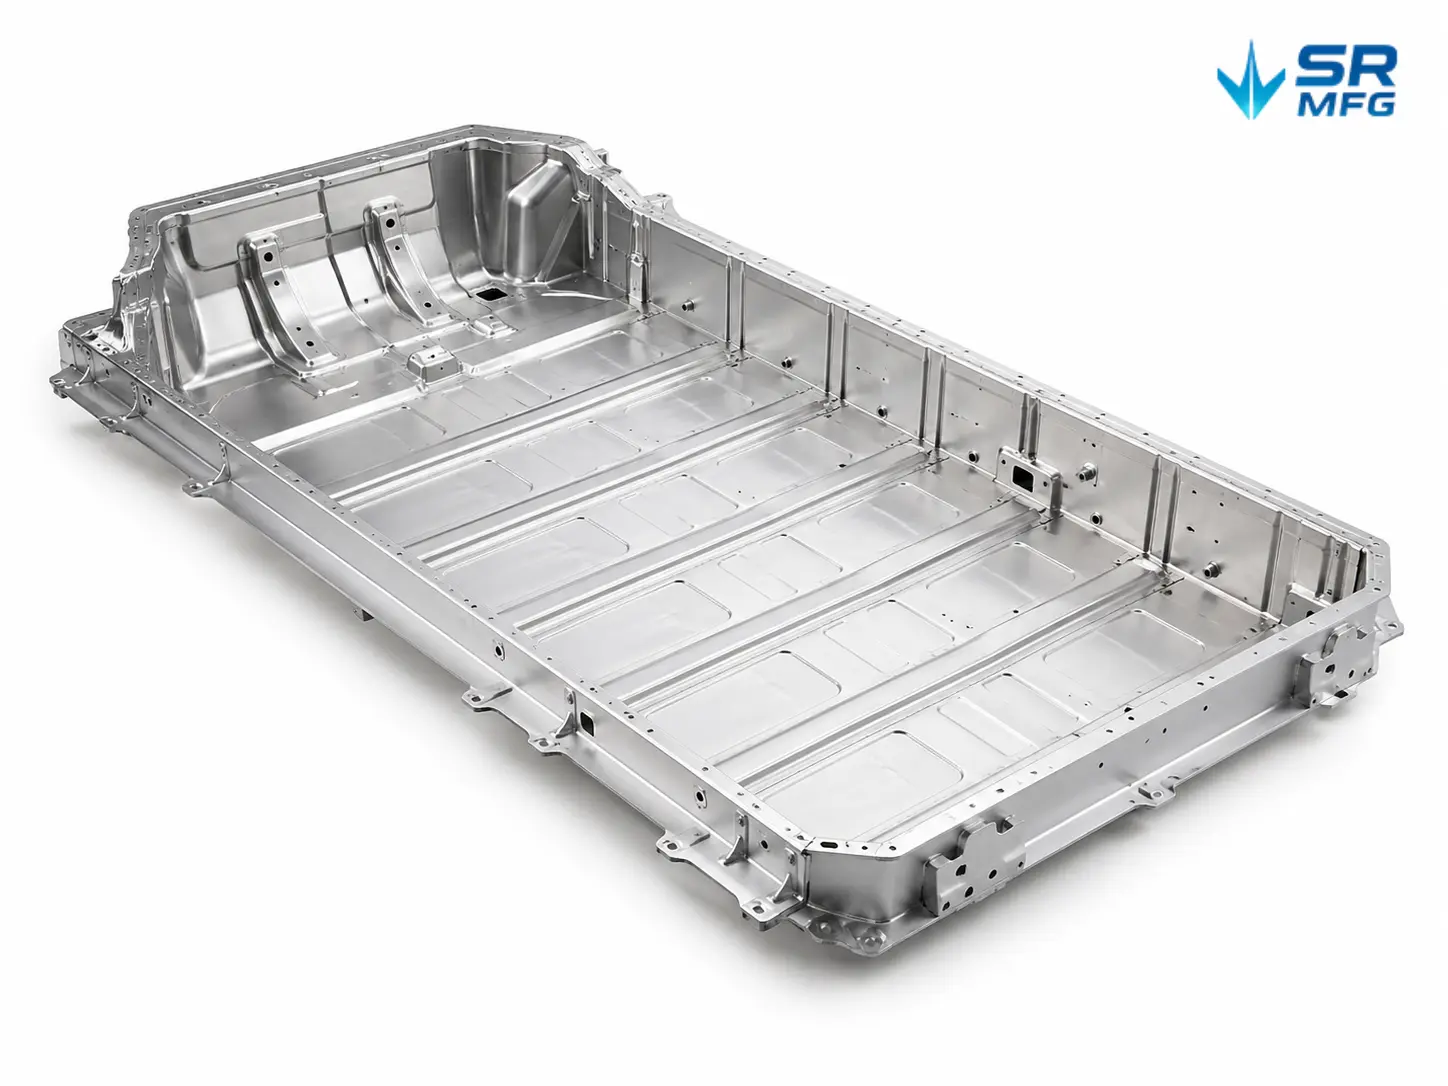
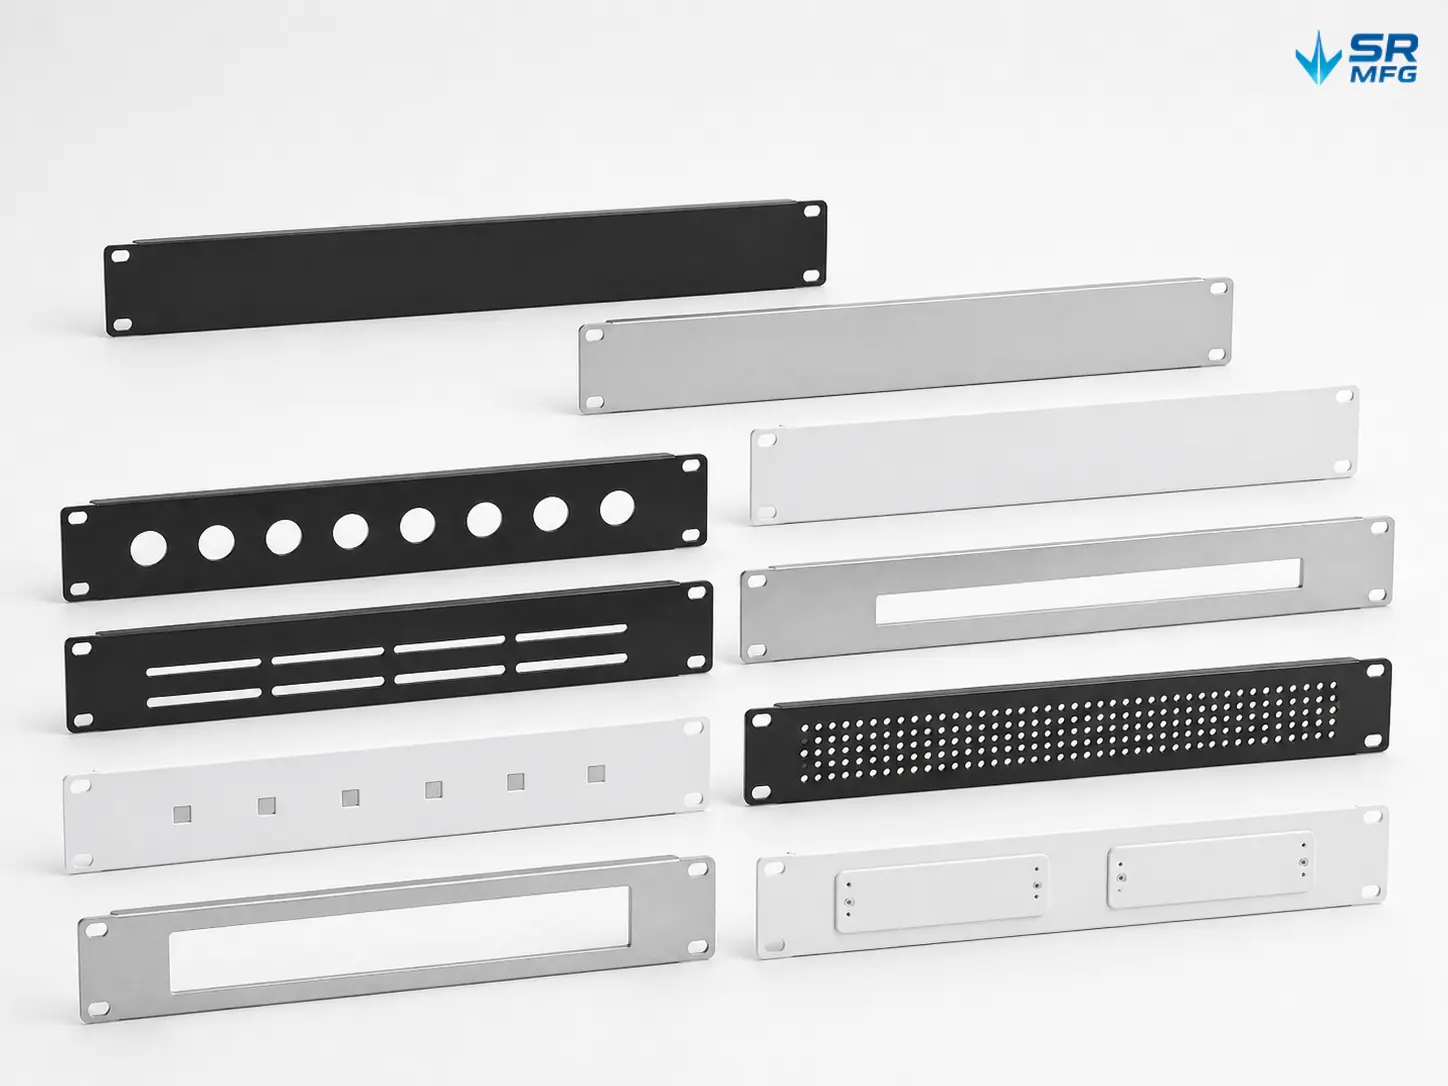
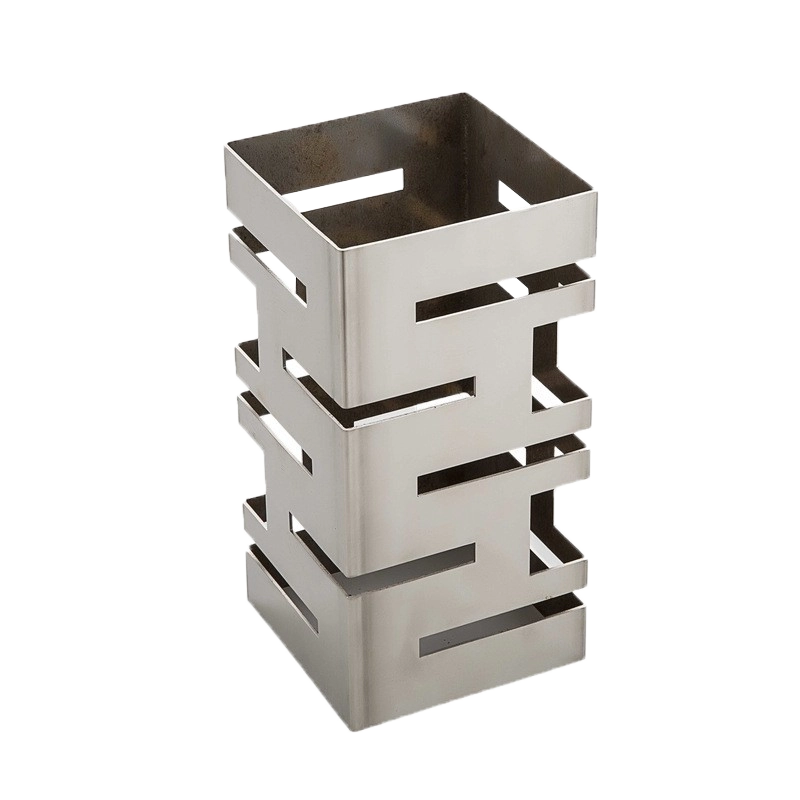
SR MFG bietet Präzisionslaserzuschnitt für kundenspezifische Blechbauteile, Gehäuse, Paneele, Halterungen und Rahmen. Wir unterstützen Prototypen- und Serienfertigung mit sauberen Kanten, engen Profilen und stabiler Wiederholbarkeit.
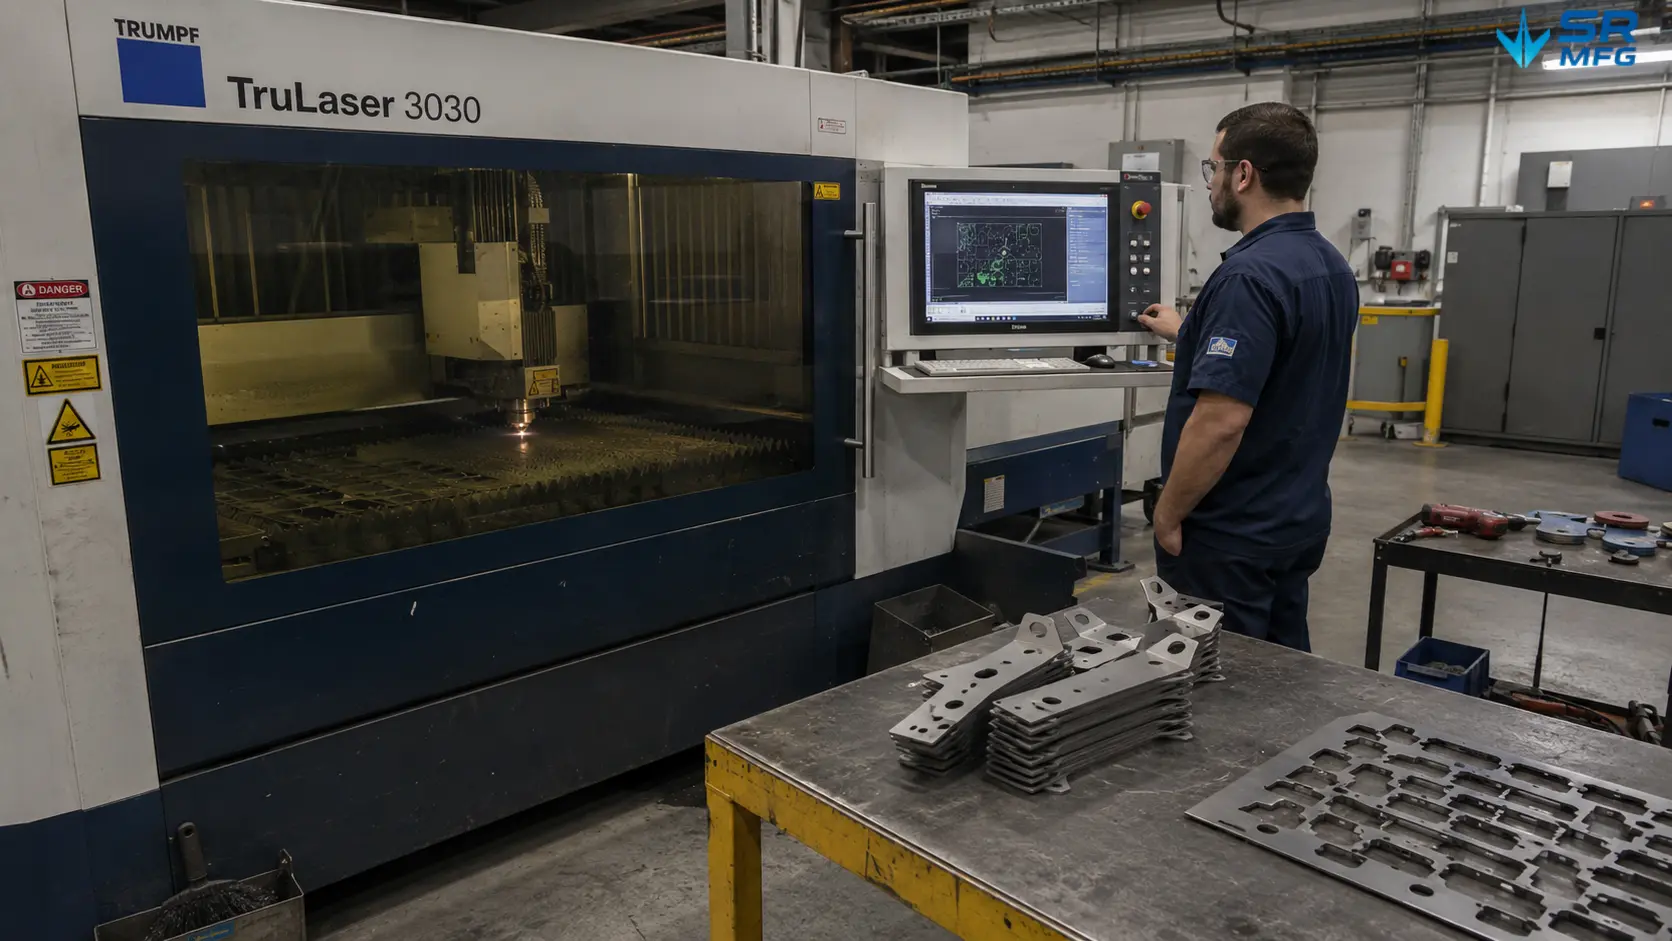
SR MFG's Präzisions-Laserzuschnitt-Fähigkeiten
SR MFG bietet Präzisionslaserzuschnitt für kundenspezifische Blechbauteile, Gehäuse, Paneele, Halterungen und Rahmen.
Mit kontrollierten Schnittparametern und automatisierter Produktionsausrüstung unterstützen wir sowohl Prototypen- als auch Serienfertigung mit sauberen Kanten und stabiler Wiederholbarkeit.
SR MFG Laser-Schneidemaschinentypen
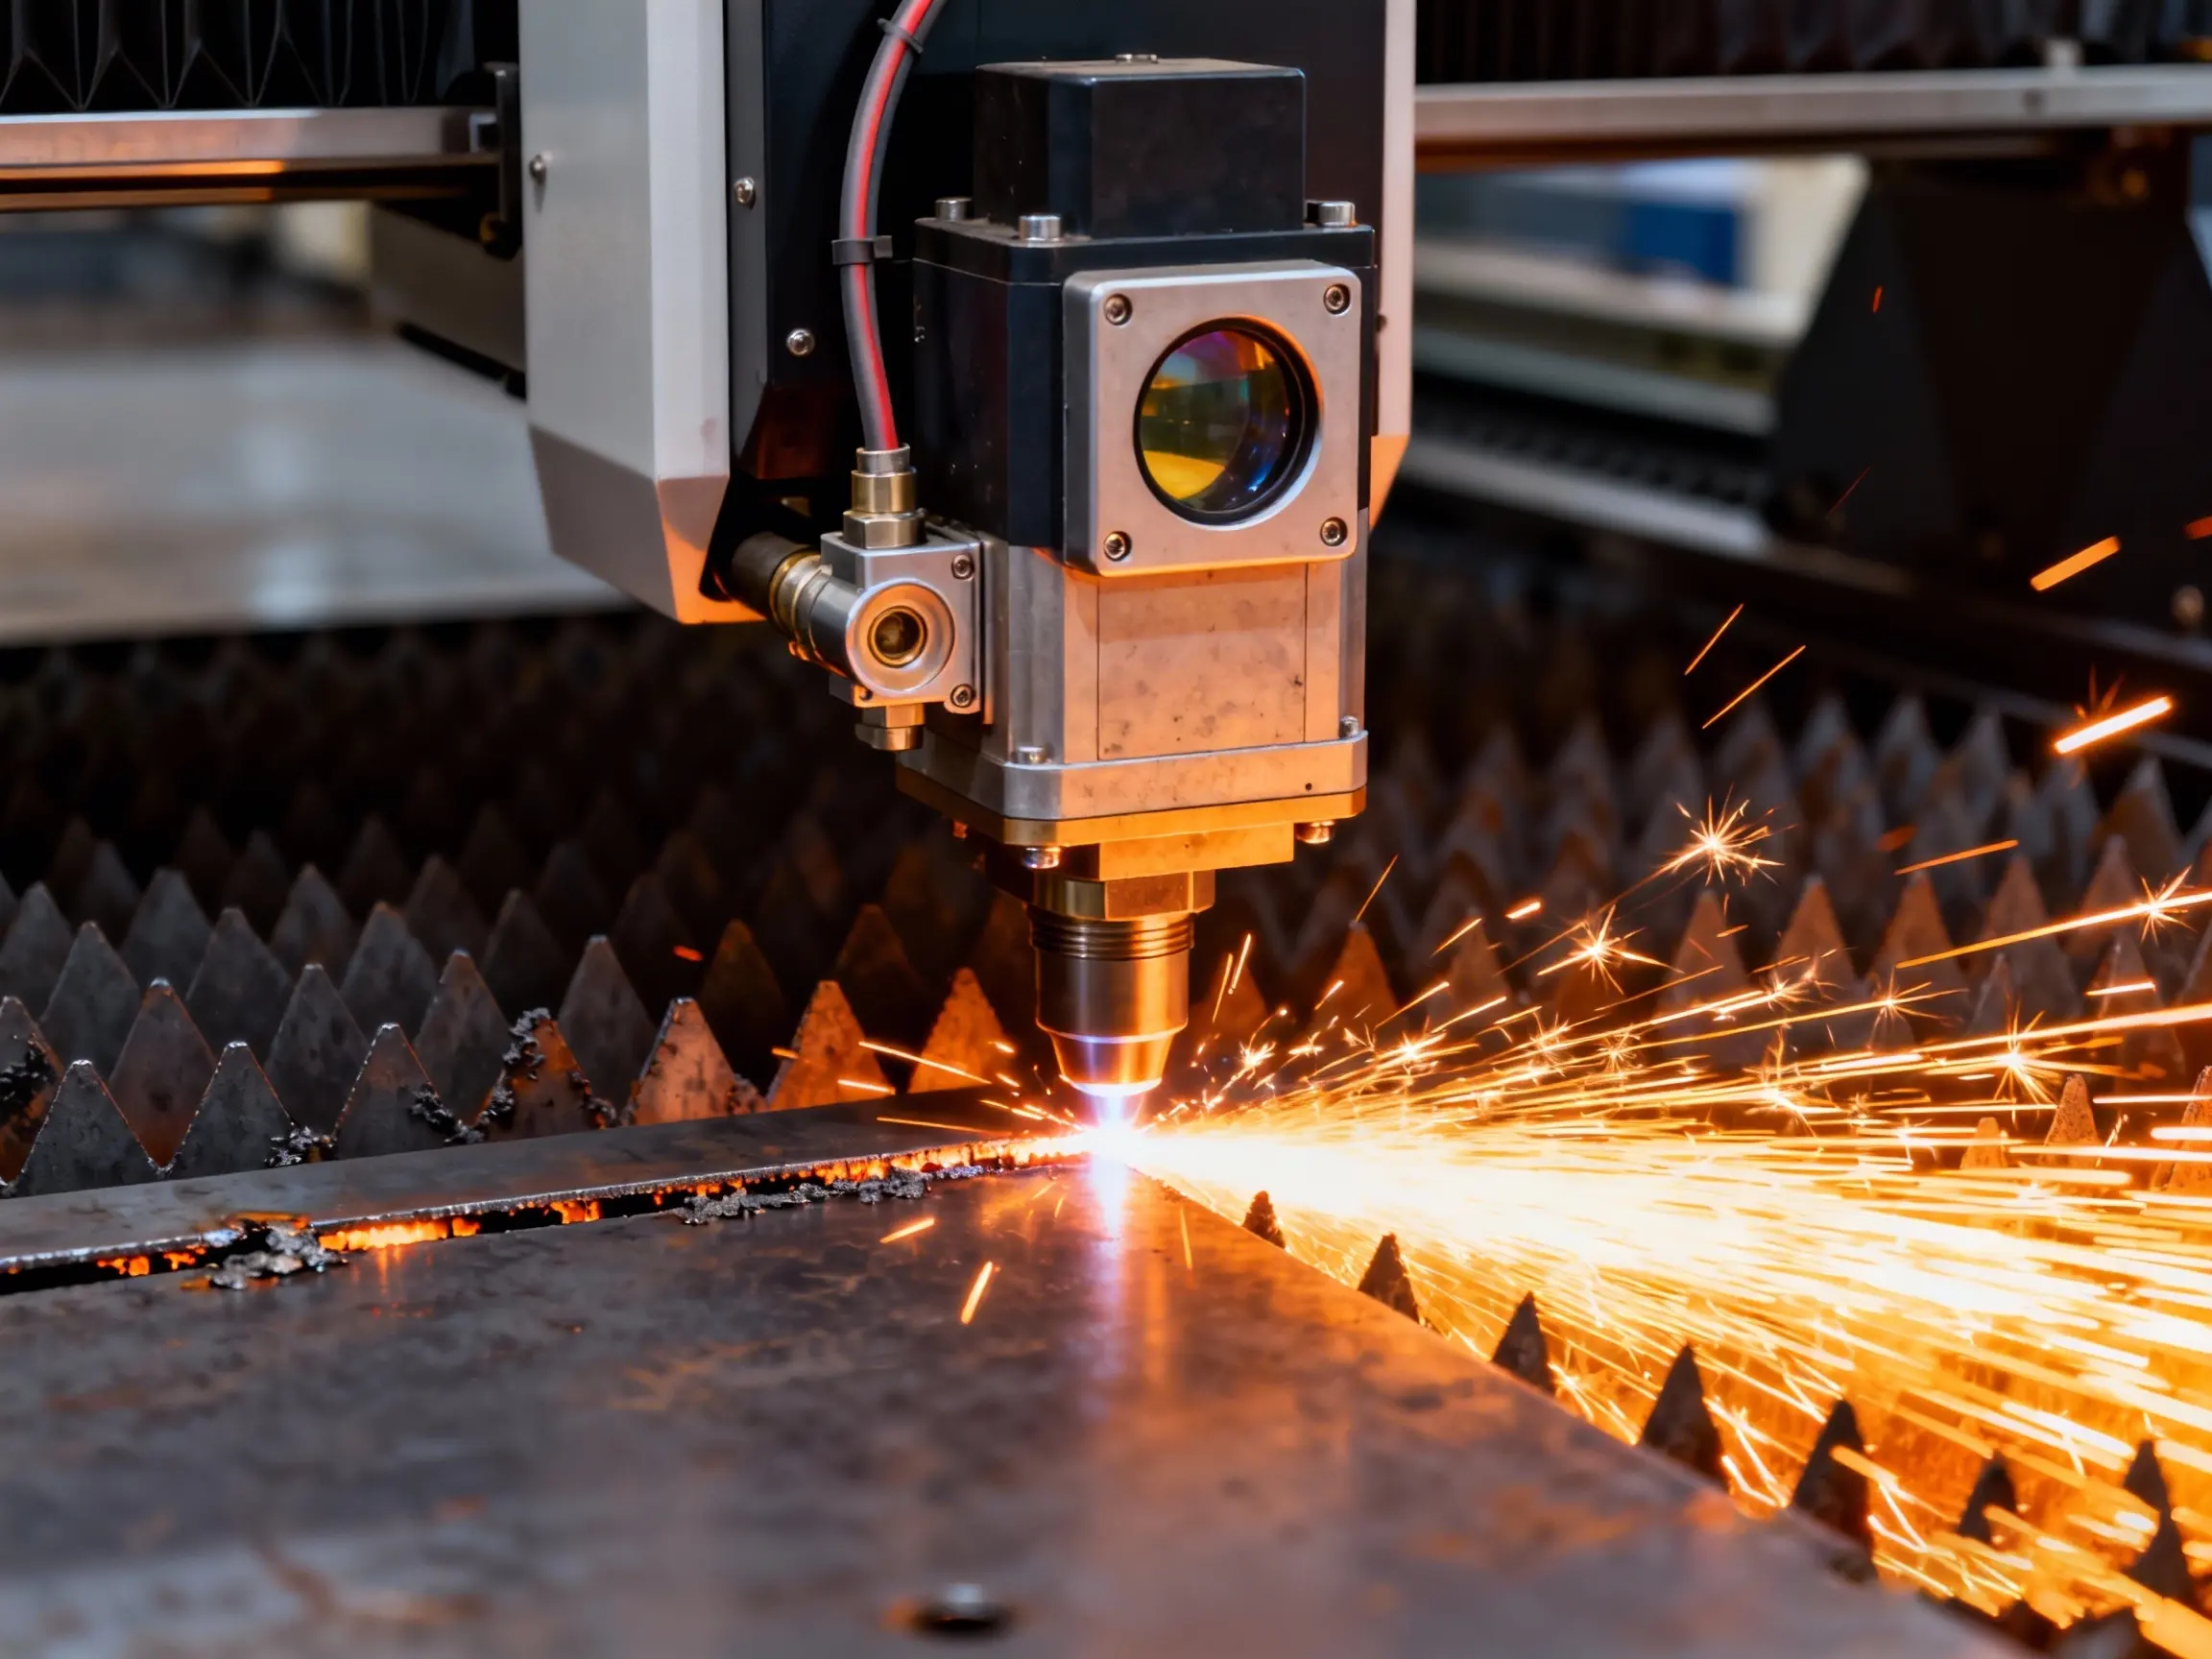
CO₂-Laser-Schneidemaschinen
Obwohl der Großteil der Blechindustrie auf Faserlaser-Schneiden umgestiegen ist, spielen CO₂-Systeme in bestimmten Fällen nach wie vor eine Schlüsselrolle – beispielsweise bei Teilen mit großen Dickenunterschieden, nichtmetallischen Sandwichstrukturen oder Prototypen aus Mischmaterialien. Unsere CO₂-Laser-Schneidsysteme werden für die Blechbearbeitung eingesetzt, wo stabile Schnittqualität und gleichbleibende Kantenleistung gefordert sind – und liefern dabei sanfte Kantenübergänge und feine Details, ohne dass Sie Ihr Design an spezielle Materialeigenschaften anpassen müssen.
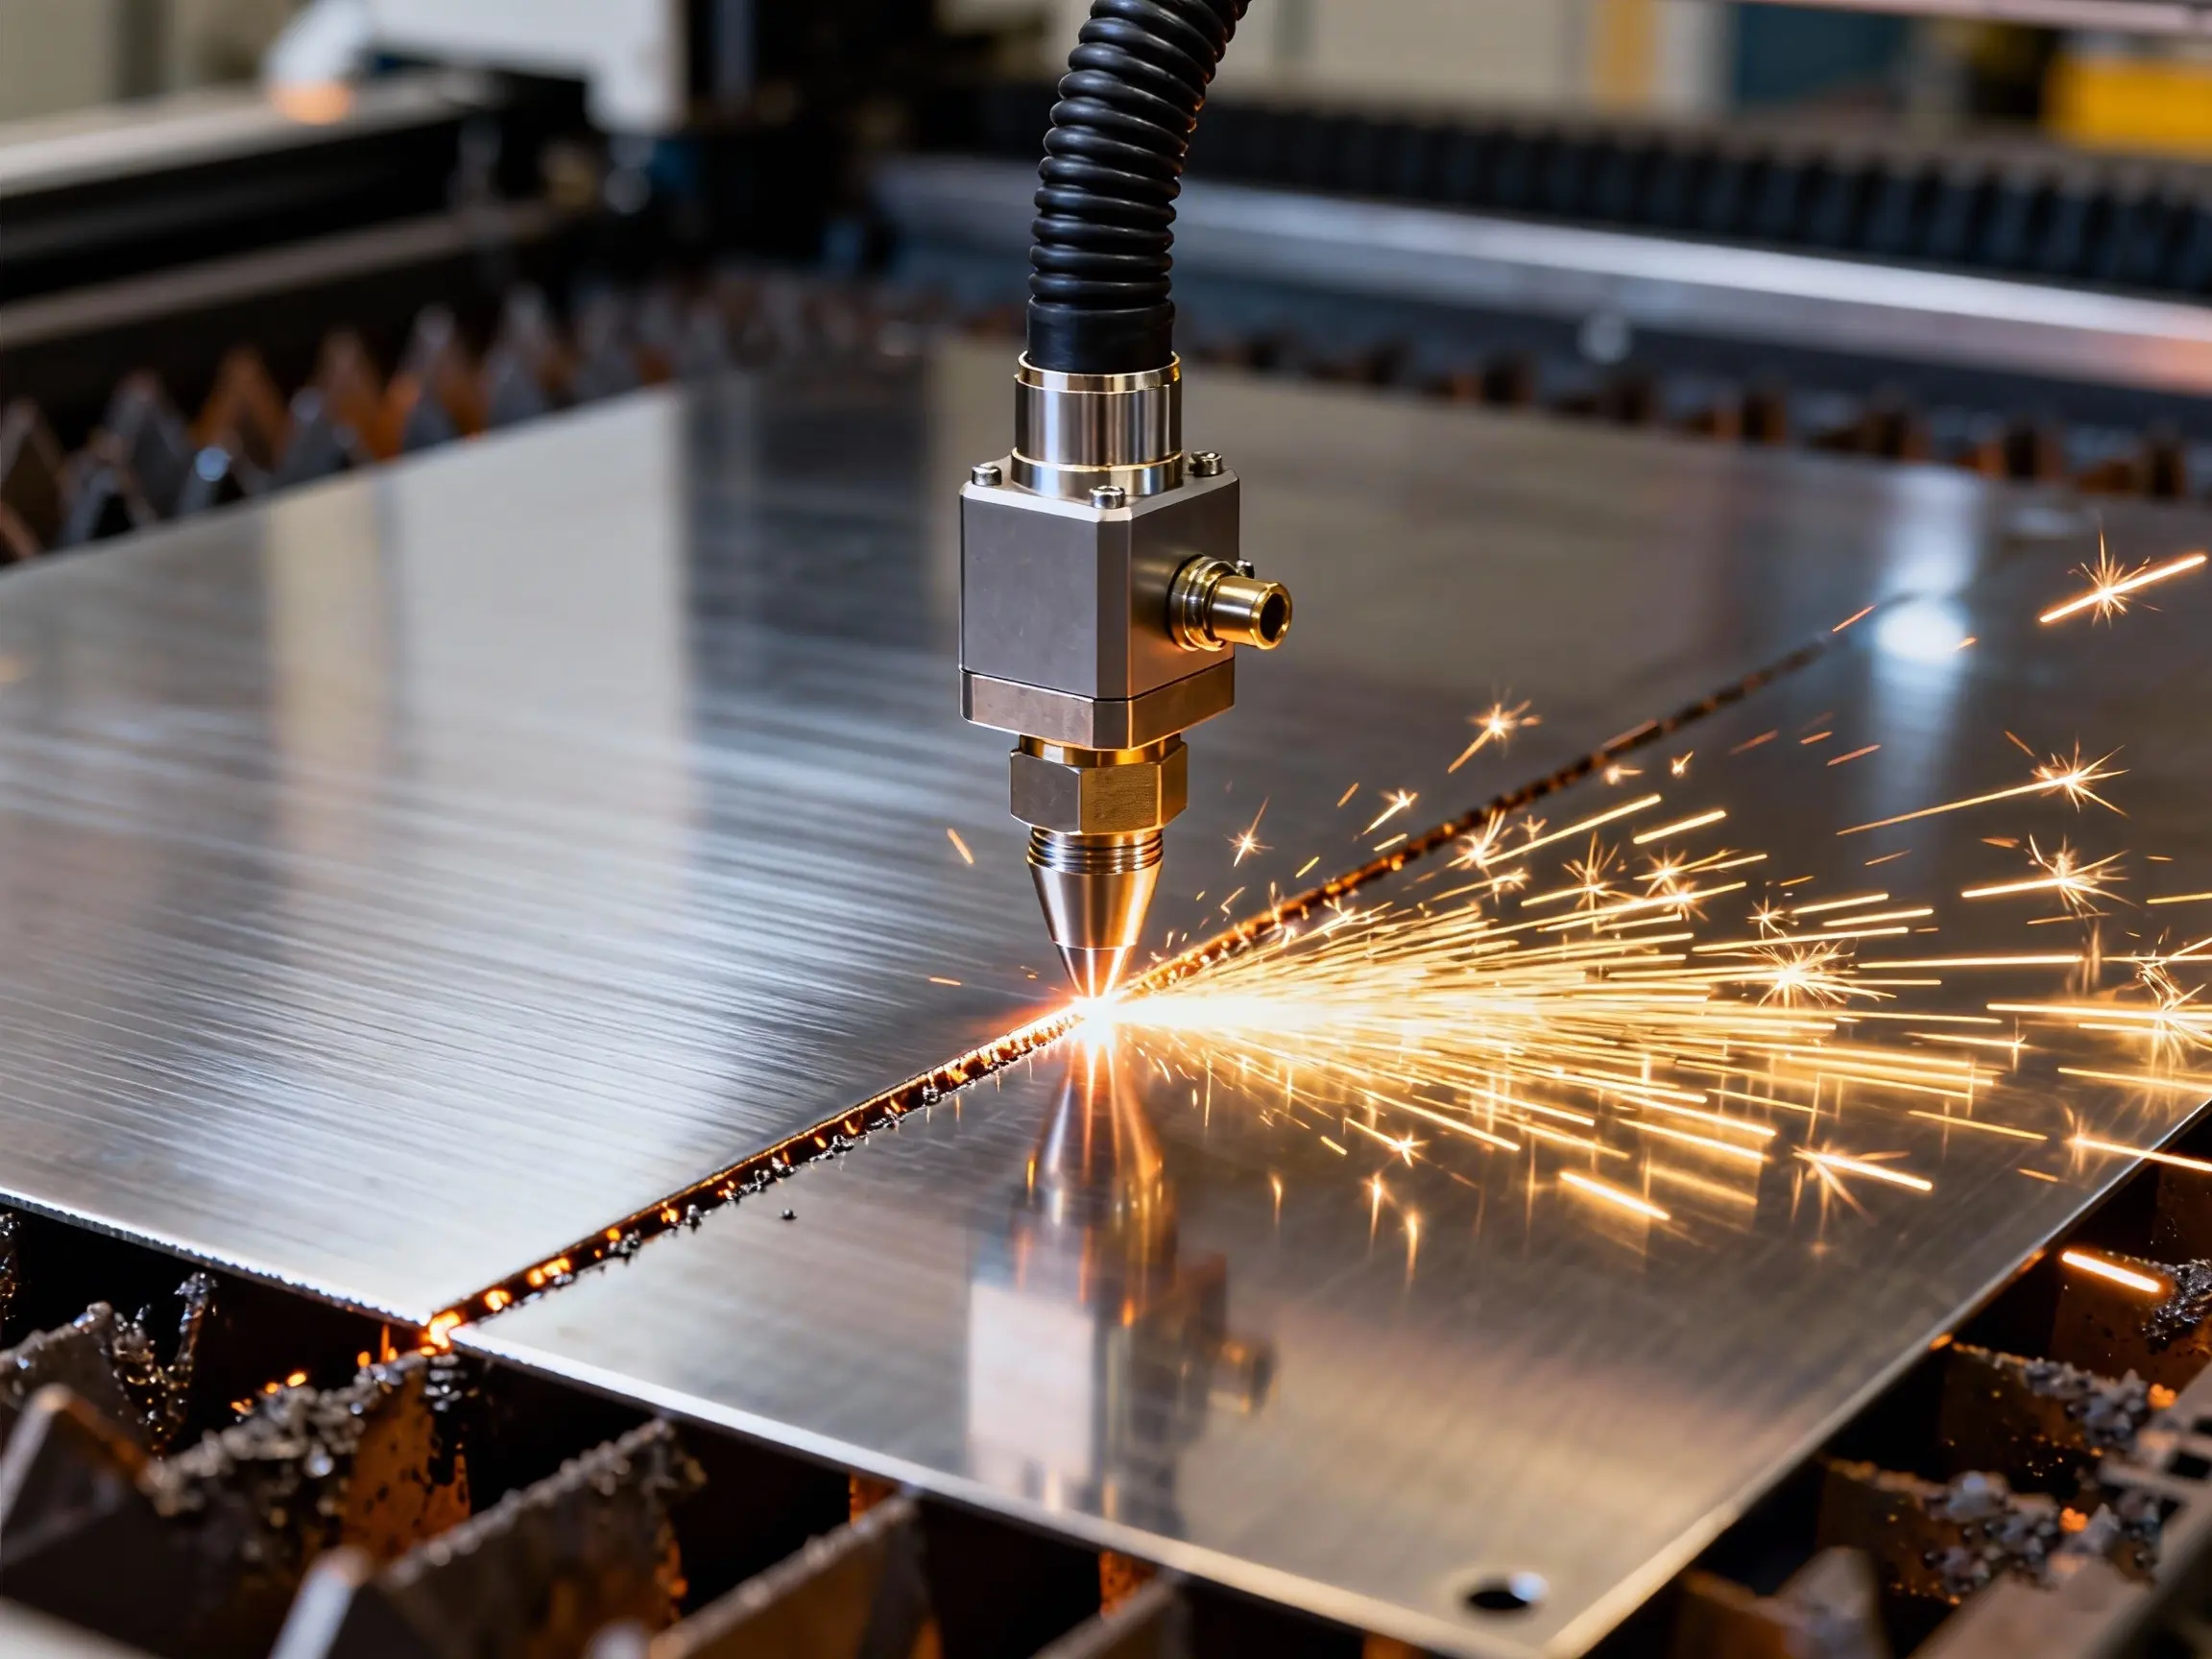
Faserlaser-Schneidemaschinen
Faserlaser-Schneider bei SR MFG liefern effizientes, hochgeschwindigkeits-Schneiden für sowohl Serien- als auch individuelle Metallteile, einschließlich reflektierender Materialien. Mit 3–5 kW Leistung sowie automatisiertem Be- und Entladen und Racking halten unsere Linien stabile Geschwindigkeit, wiederholbare Genauigkeit und gleichbleibende Strahlqualität – selbst im unbeaufsichtigten oder personalreduzierten Betrieb, wo echte Produktivität aus Stabilität und nicht allein aus Leistung entsteht.
Unsere Laser-Schneidanlagen
SR MFG verwendet mehrere Laser-Schneidsysteme, um verschiedene Blechmaterialien, Dicken, Teilegrößen und Produktionsmengen zu unterstützen.
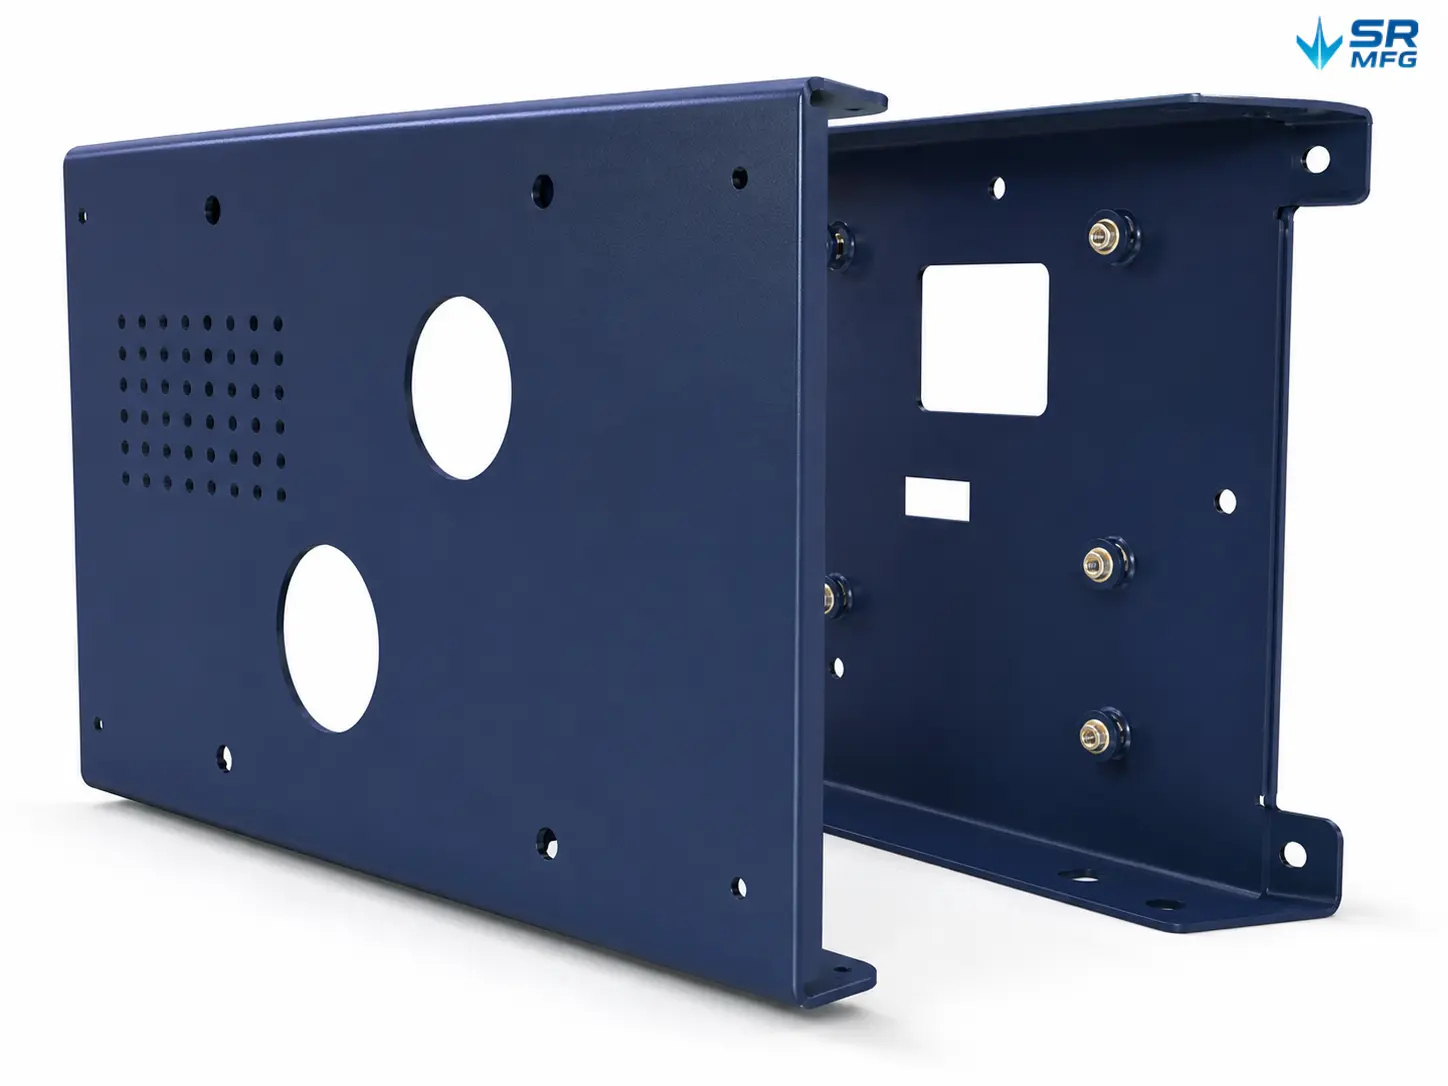
Unsere wichtigsten Laser-Schneidsysteme
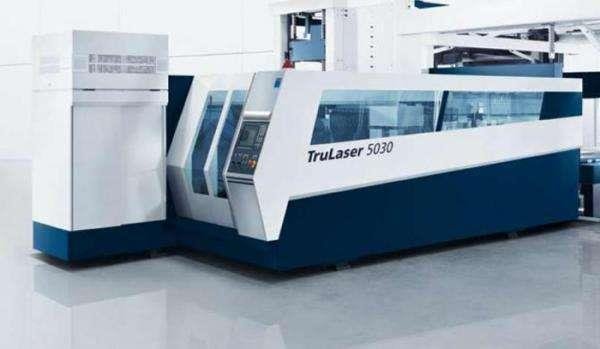
Trumpf TruLaser 5030
Hochleistungs-Präzisionsschneidsystem für großformatige Blechteile und Dickblechanwendungen.
- Großformatiges Schneiden
- Hohe Leistungsstabilität
- Unterstützung von Strukturteilen
Trumpf TruLaser 4030
Vielseitiges CO₂-Laser-Schneidsystem für gleichbleibende Kantenqualität bei verschiedenen Materialien und Dicken.
- CO₂-Lasertechnologie
- Gleichbleibende Kantenqualität
- Unterstützung von Mischmaterialien
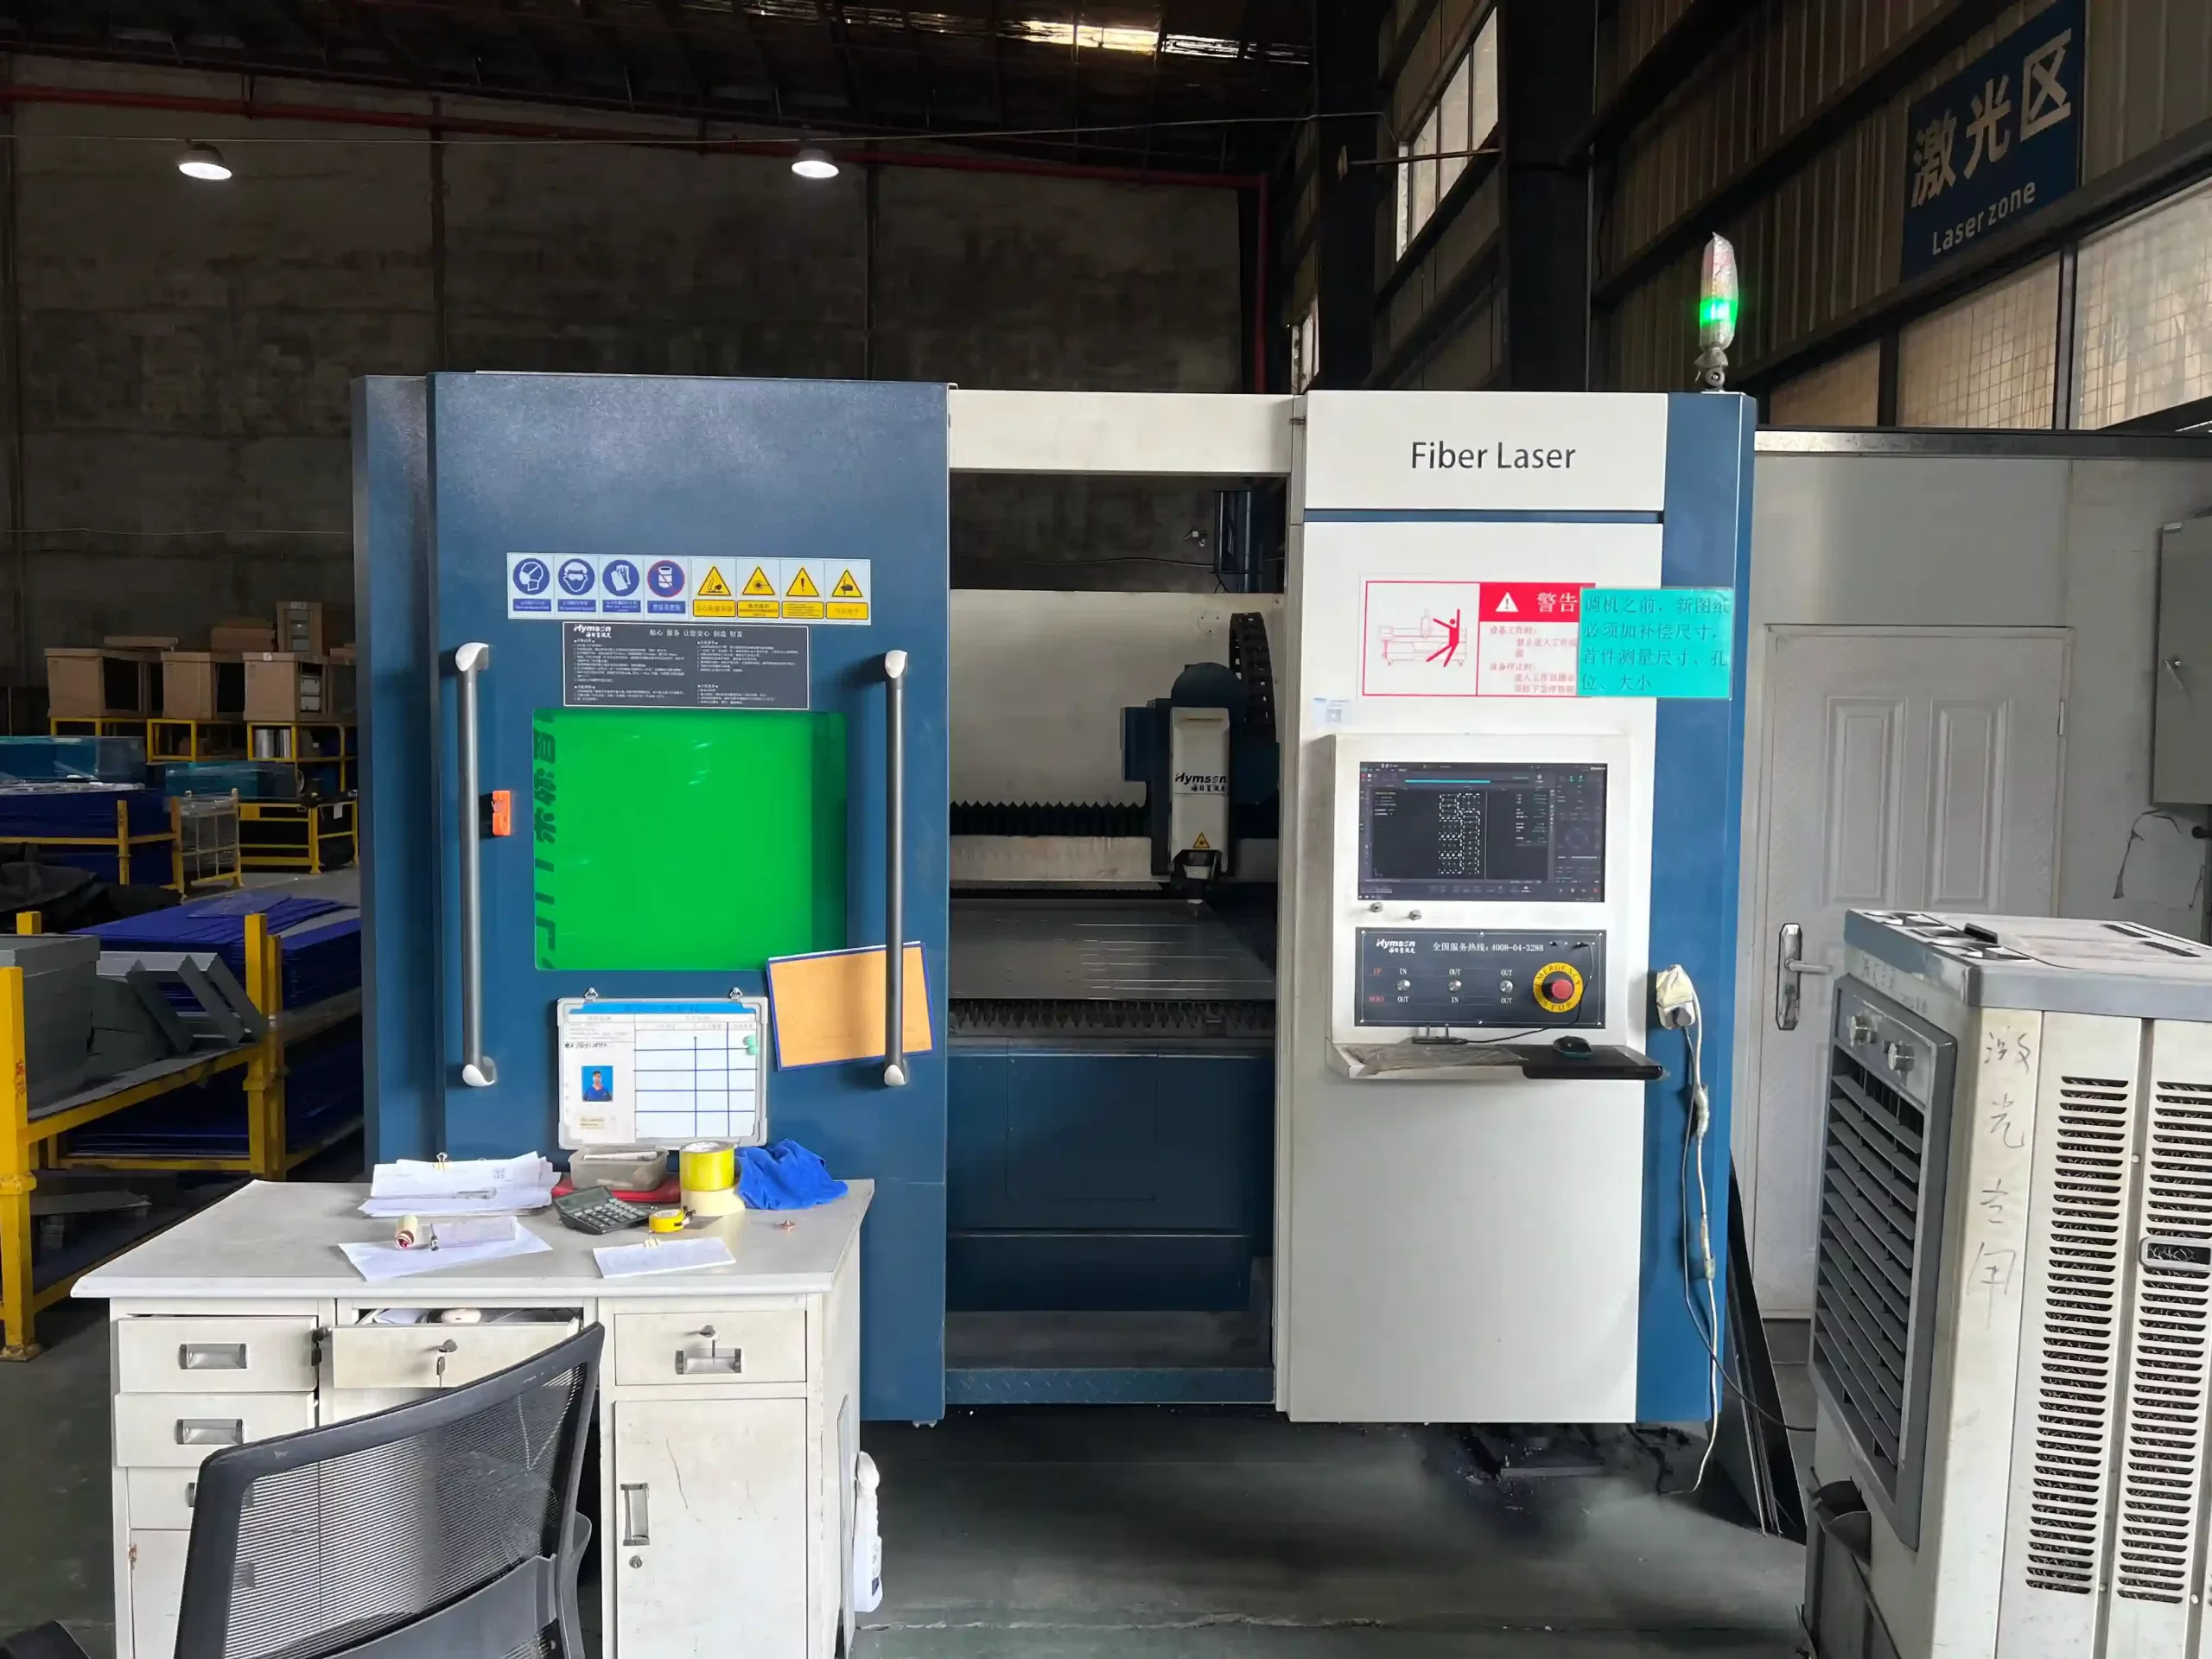
Hymson HF3015B
Zuverlässiges Faserlaser-Schneidsystem, optimiert für Dünnblechbearbeitung, Serienproduktion und schnelle Lieferung.
- Dünnblechschneiden
- Kosteneffizienter Betrieb
- Schnelle Serienabwicklung
Detaillierte Gerätespezifikationen
Laserleistung, Arbeitstischgröße, Schnittdicke, Genauigkeit und Beladeunterstützung.
⌄
Detaillierte Gerätespezifikationen
Laserleistung, Arbeitstischgröße, Schnittdicke, Genauigkeit und Beladeunterstützung.
| Gerätemodell | Lasertyp / Leistung | Arbeitstisch | Max. Schnittdicke | Positioniergenauigkeit | Wiederholbarkeit | Automatisches Beladen |
|---|---|---|---|---|---|---|
| Trumpf TruLaser 5030 | Faserlaser / 5 kW | 3000 × 1500 mm | 25 mm Kohlenstoffstahl / 20 mm Edelstahl | ±0,03 mm/m | ±0,02 mm | Unterstützt |
| Trumpf TruLaser 4030 | CO₂-Laser / 4 kW | 3000 × 1500 mm | 20 mm Kohlenstoffstahl | ±0,03 mm/m | ±0,02 mm | Unterstützt |
| Hymson HF3015B | Faserlaser / 3 kW | 3000 × 1500 mm | 20 mm Kohlenstoffstahl | ±0,03 mm/m | ±0,02 mm | Unterstützt |
Production Capacity Benchmark
Internal capacity reference based on continuous production conditions.
⌄
Production Capacity Benchmark
Internal capacity reference based on continuous production conditions.
| Gerätemodell | Cutting Speed | Utilization Rate | Tagesleistung (Theoretical Cutting Length) |
Typical Part Qty (per day, based on 1m × 1m sheet parts) |
|---|---|---|---|---|
| TruLaser 5030 | 30 m/min | 85% | 36,720 m | ~3,600 parts |
| TruLaser 4030 | 15 m/min | 85% | 18,360 m | ~1,800 parts |
| HF3015B | 25 m/min | 85% | 30,600 m | ~3,000 parts |
Accuracy, Tolerance & Repeatability
SR MFG focuses on stable,consistent quality in mass production. Our laser cutting process ensures
tight tolerances, smooth edges, and excellent repeatability from prototype to large-scale production.
Standard Tolerances for Laser-Cut Metal
View reference tolerance ranges by machine type, thickness, accuracy, roughness, and tolerance grade.
⌄
Standard Tolerances for Laser-Cut Metal
View reference tolerance ranges by machine type, thickness, accuracy, roughness, and tolerance grade.
| Machine Model | Materialstärke | Linear Dimensional Tolerance | Angular Tolerance (per 100 mm) |
Lochpositionstoleranz (Hole Diameter ≤ 50 mm) |
Surface Roughness Ra (μm) |
Tolerance Grade |
|---|---|---|---|---|---|---|
| TRUMPF 5030 (Fiber Laser) |
≤ 3 mm | ±0,05 mm | ±0.1° | ±0,05 mm | 1.6–3.2 | IT8 |
| 3–6 mm | ±0.10 mm | ±0.1° | ±0.10 mm | 1.6–3.2 | IT9 | |
| 6–12 mm | ±0.15 mm | ±0.1° | ±0.10 mm | 3.2–6.3 | IT9 | |
| 12–20 mm | ±0.20 mm | ±0.2° | ±0.15 mm | 3.2–6.3 | IT10 | |
| > 20 mm | ±0.30 mm | ±0.2° | ±0.15 mm | 6.3–12.5 | IT10 | |
| TRUMPF 4030 (CO₂ Laser) |
≤ 3 mm | ±0.08 mm | ±0.1° | ±0.08 mm | 3.2–6.3 | IT8 |
| 3–6 mm | ±0.15 mm | ±0.1° | ±0.12 mm | 3.2–6.3 | IT9 | |
| 6–12 mm | ±0.20 mm | ±0.2° | ±0.15 mm | 6.3–12.5 | IT9 | |
| 12–20 mm | ±0.25 mm | ±0.2° | ±0.20 mm | 6.3–12.5 | IT10 | |
| > 20 mm | ±0.35 mm | ±0.3° | ±0.20 mm | 12.5–25 | IT10 | |
| Hymson HF3015B (Fiber Laser) |
≤ 3 mm | ±0.06 mm | ±0.1° | ±0.06 mm | 1.6–3.2 | IT8 |
| 3–6 mm | ±0.12 mm | ±0.1° | ±0.10 mm | 1.6–3.2 | IT9 | |
| 6–12 mm | ±0.18 mm | ±0.2° | ±0.12 mm | 3.2–6.3 | IT9 |
Small Holes & Complex Contours
⌄
Small Holes & Complex Contours
For small holes, sharp corners, narrow slots, and complex contours, SR MFG adjusts piercing strategy, beam mode, and cutting path to maintain stable edge quality and dimensional accuracy.
- Optimized initial piercing strategy
- Beam mode adjustment for fine features
- Step-cutting for complex contours
- Micro-joints added when needed for stability
HAZ & Edge Quality Control
⌄
HAZ & Edge Quality Control
Edge quality affects later bending, welding, coating adhesion, and assembly. SR MFG controls heat input, assist gas pressure, and cutting paths to reduce burrs, overheating, and deformation.
- Low-heat input path optimization
- Assist gas pressure control
- Segmented toolpaths to avoid localized overheating
- Edge condition review before bending or finishing
Repeatability & Batch Consistency
⌄
Repeatability & Batch Consistency
For batch production, the key challenge is not only making one accurate part, but keeping dimensions consistent across different shifts, machines, and repeat orders.
- Standardized cutting parameters
- Consistent sheet clamping method
- Unified toolpath offset settings
- Nozzle and head wear monitoring across batches
From Prototype to Mass Production
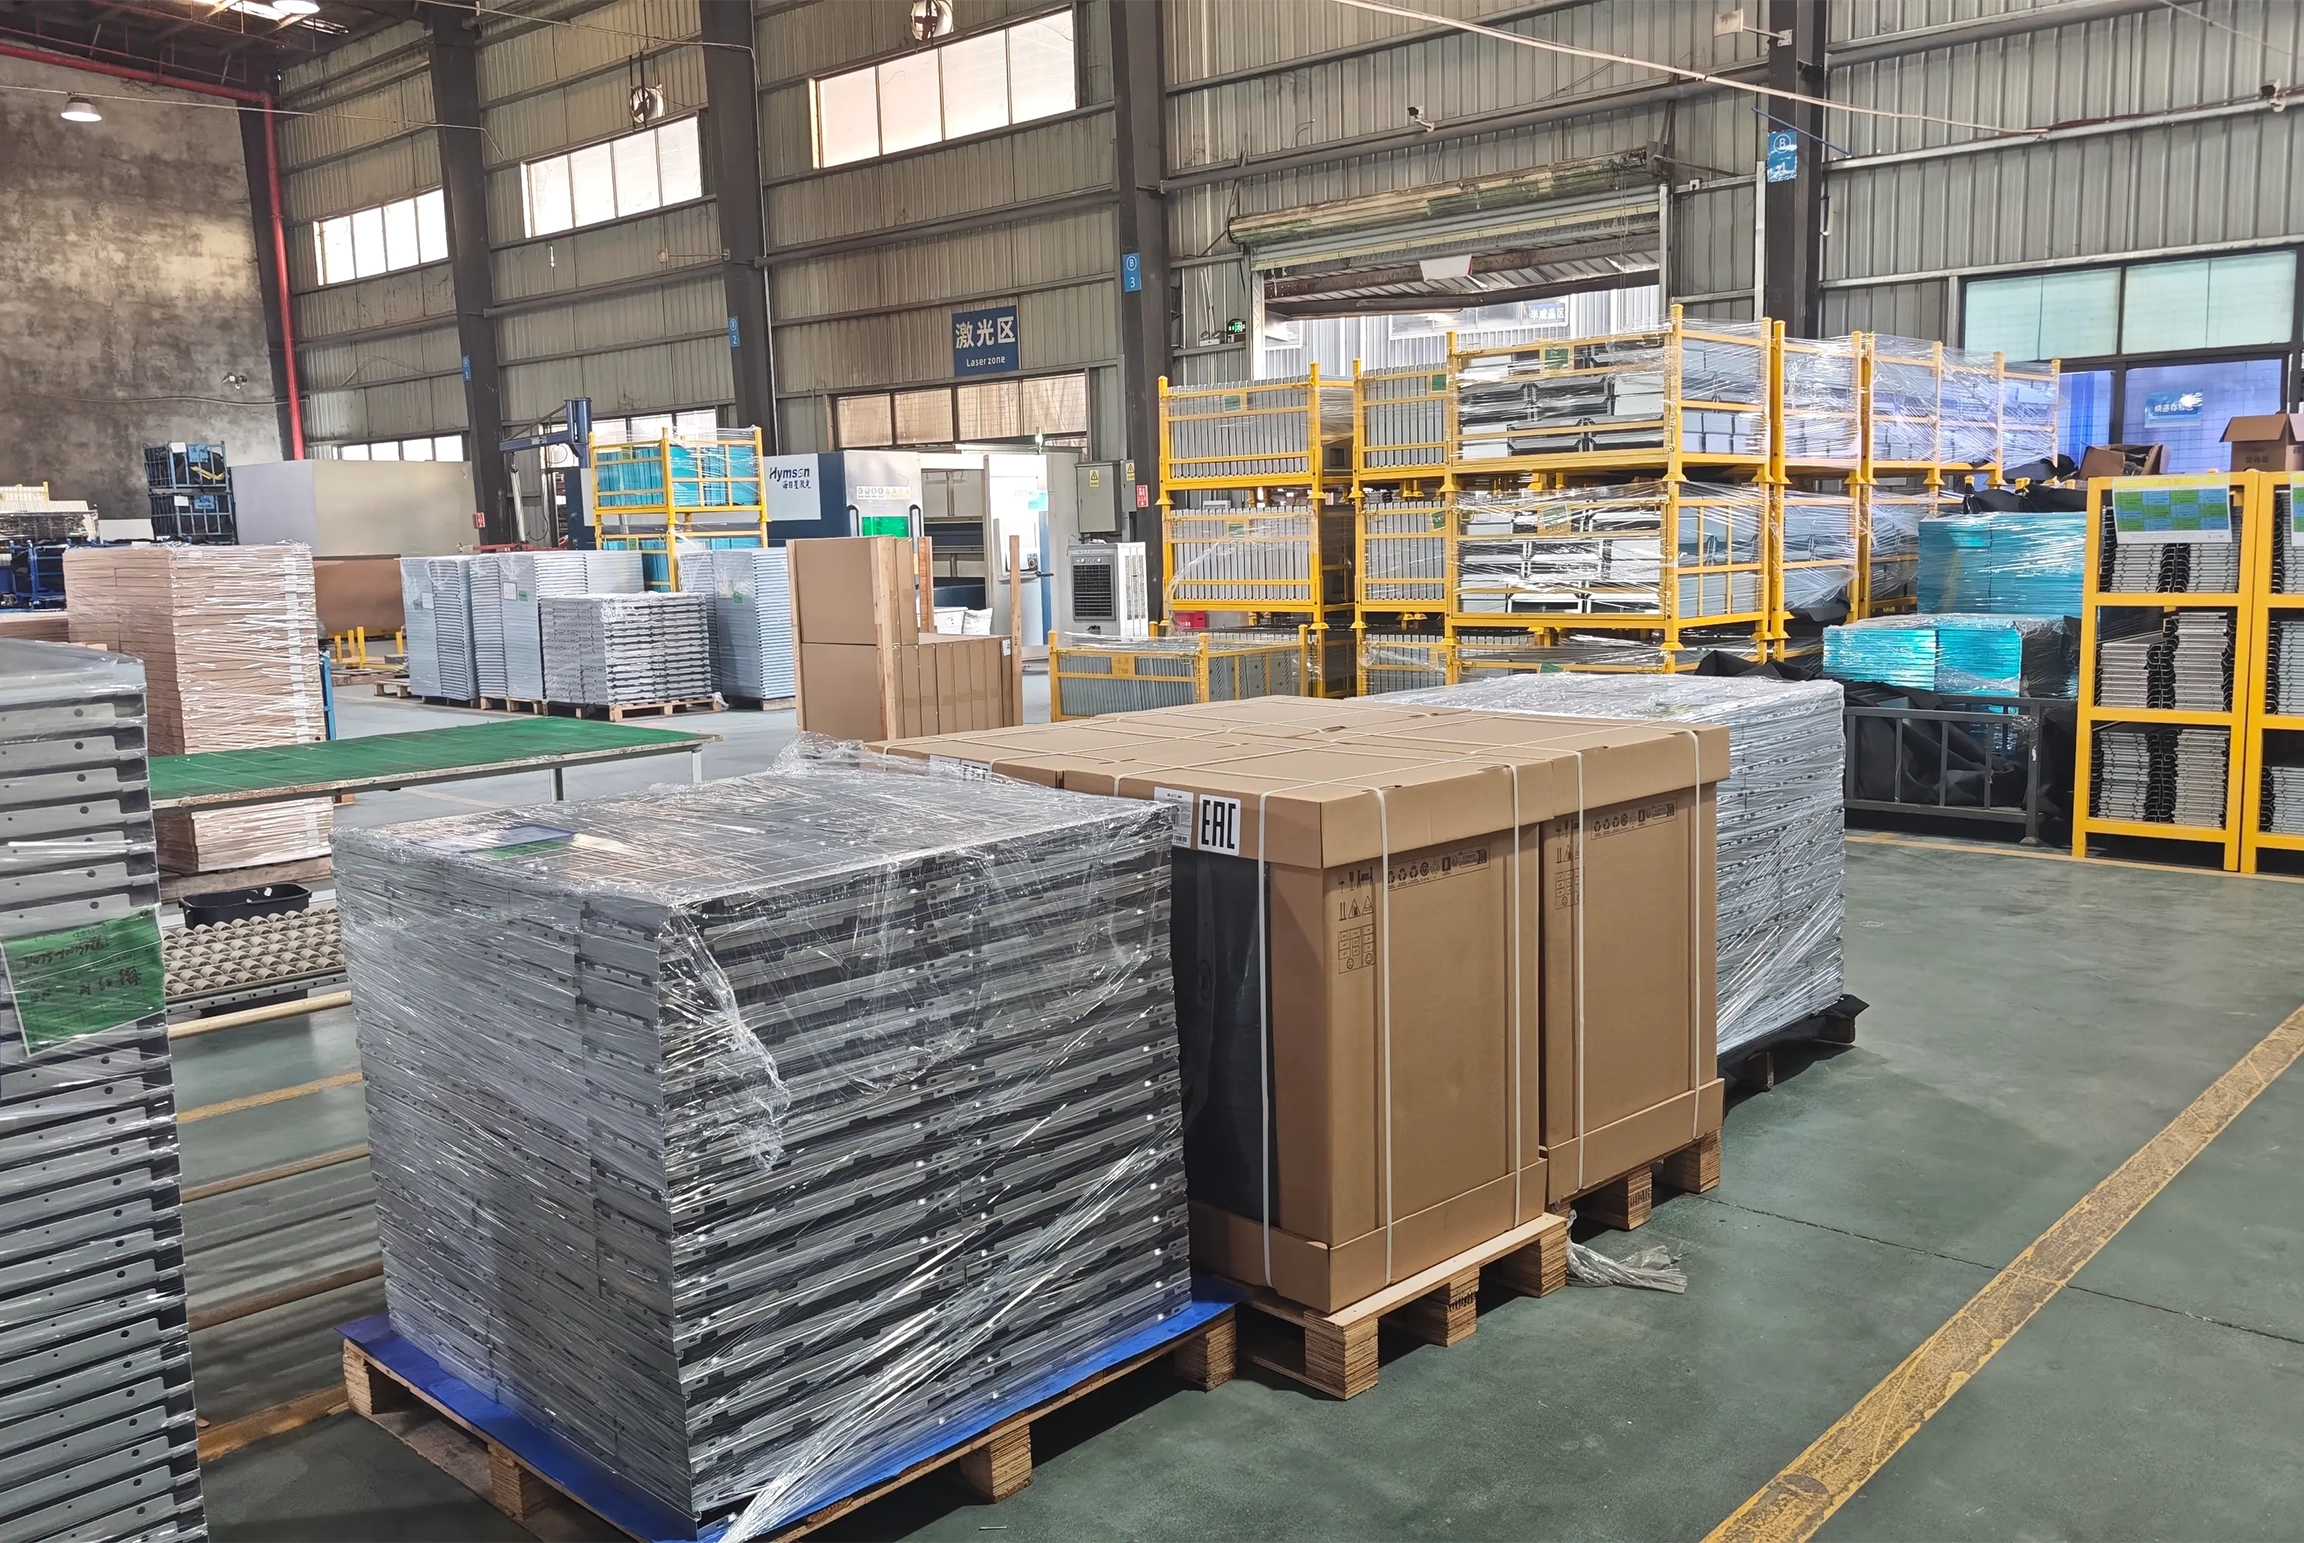
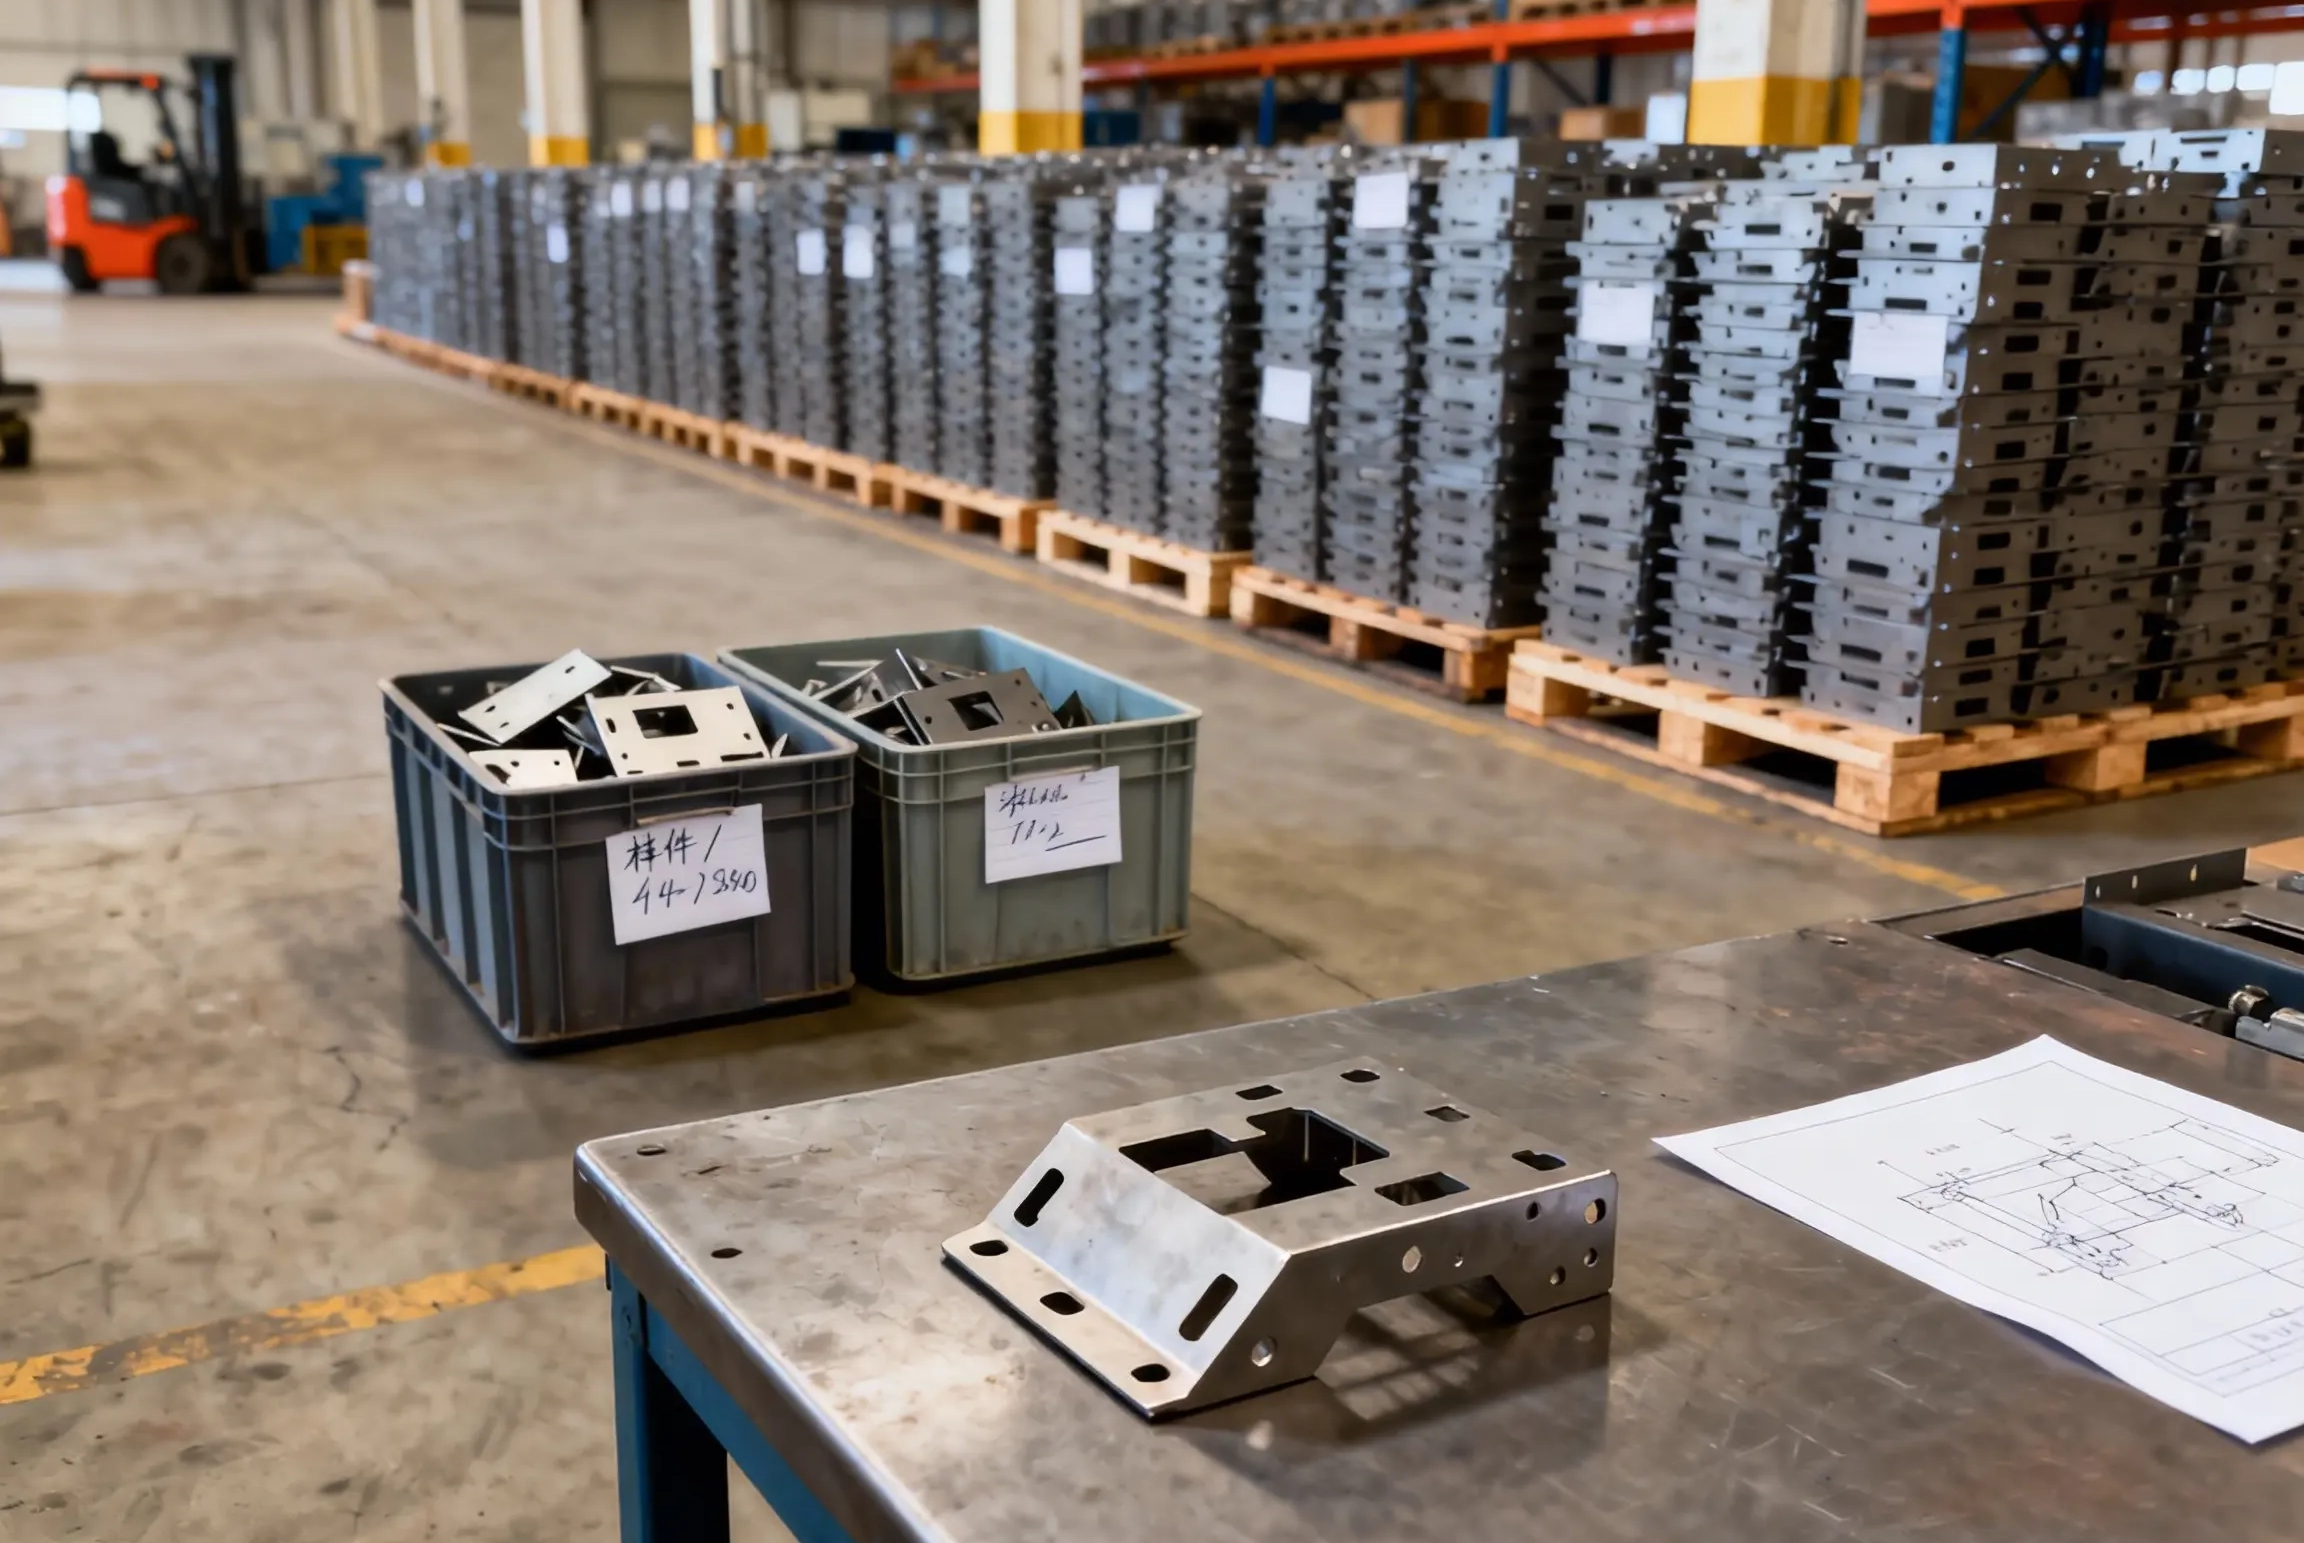
SR MFG supports laser-cut sheet metal projects from rapid samples to repeat batch production.
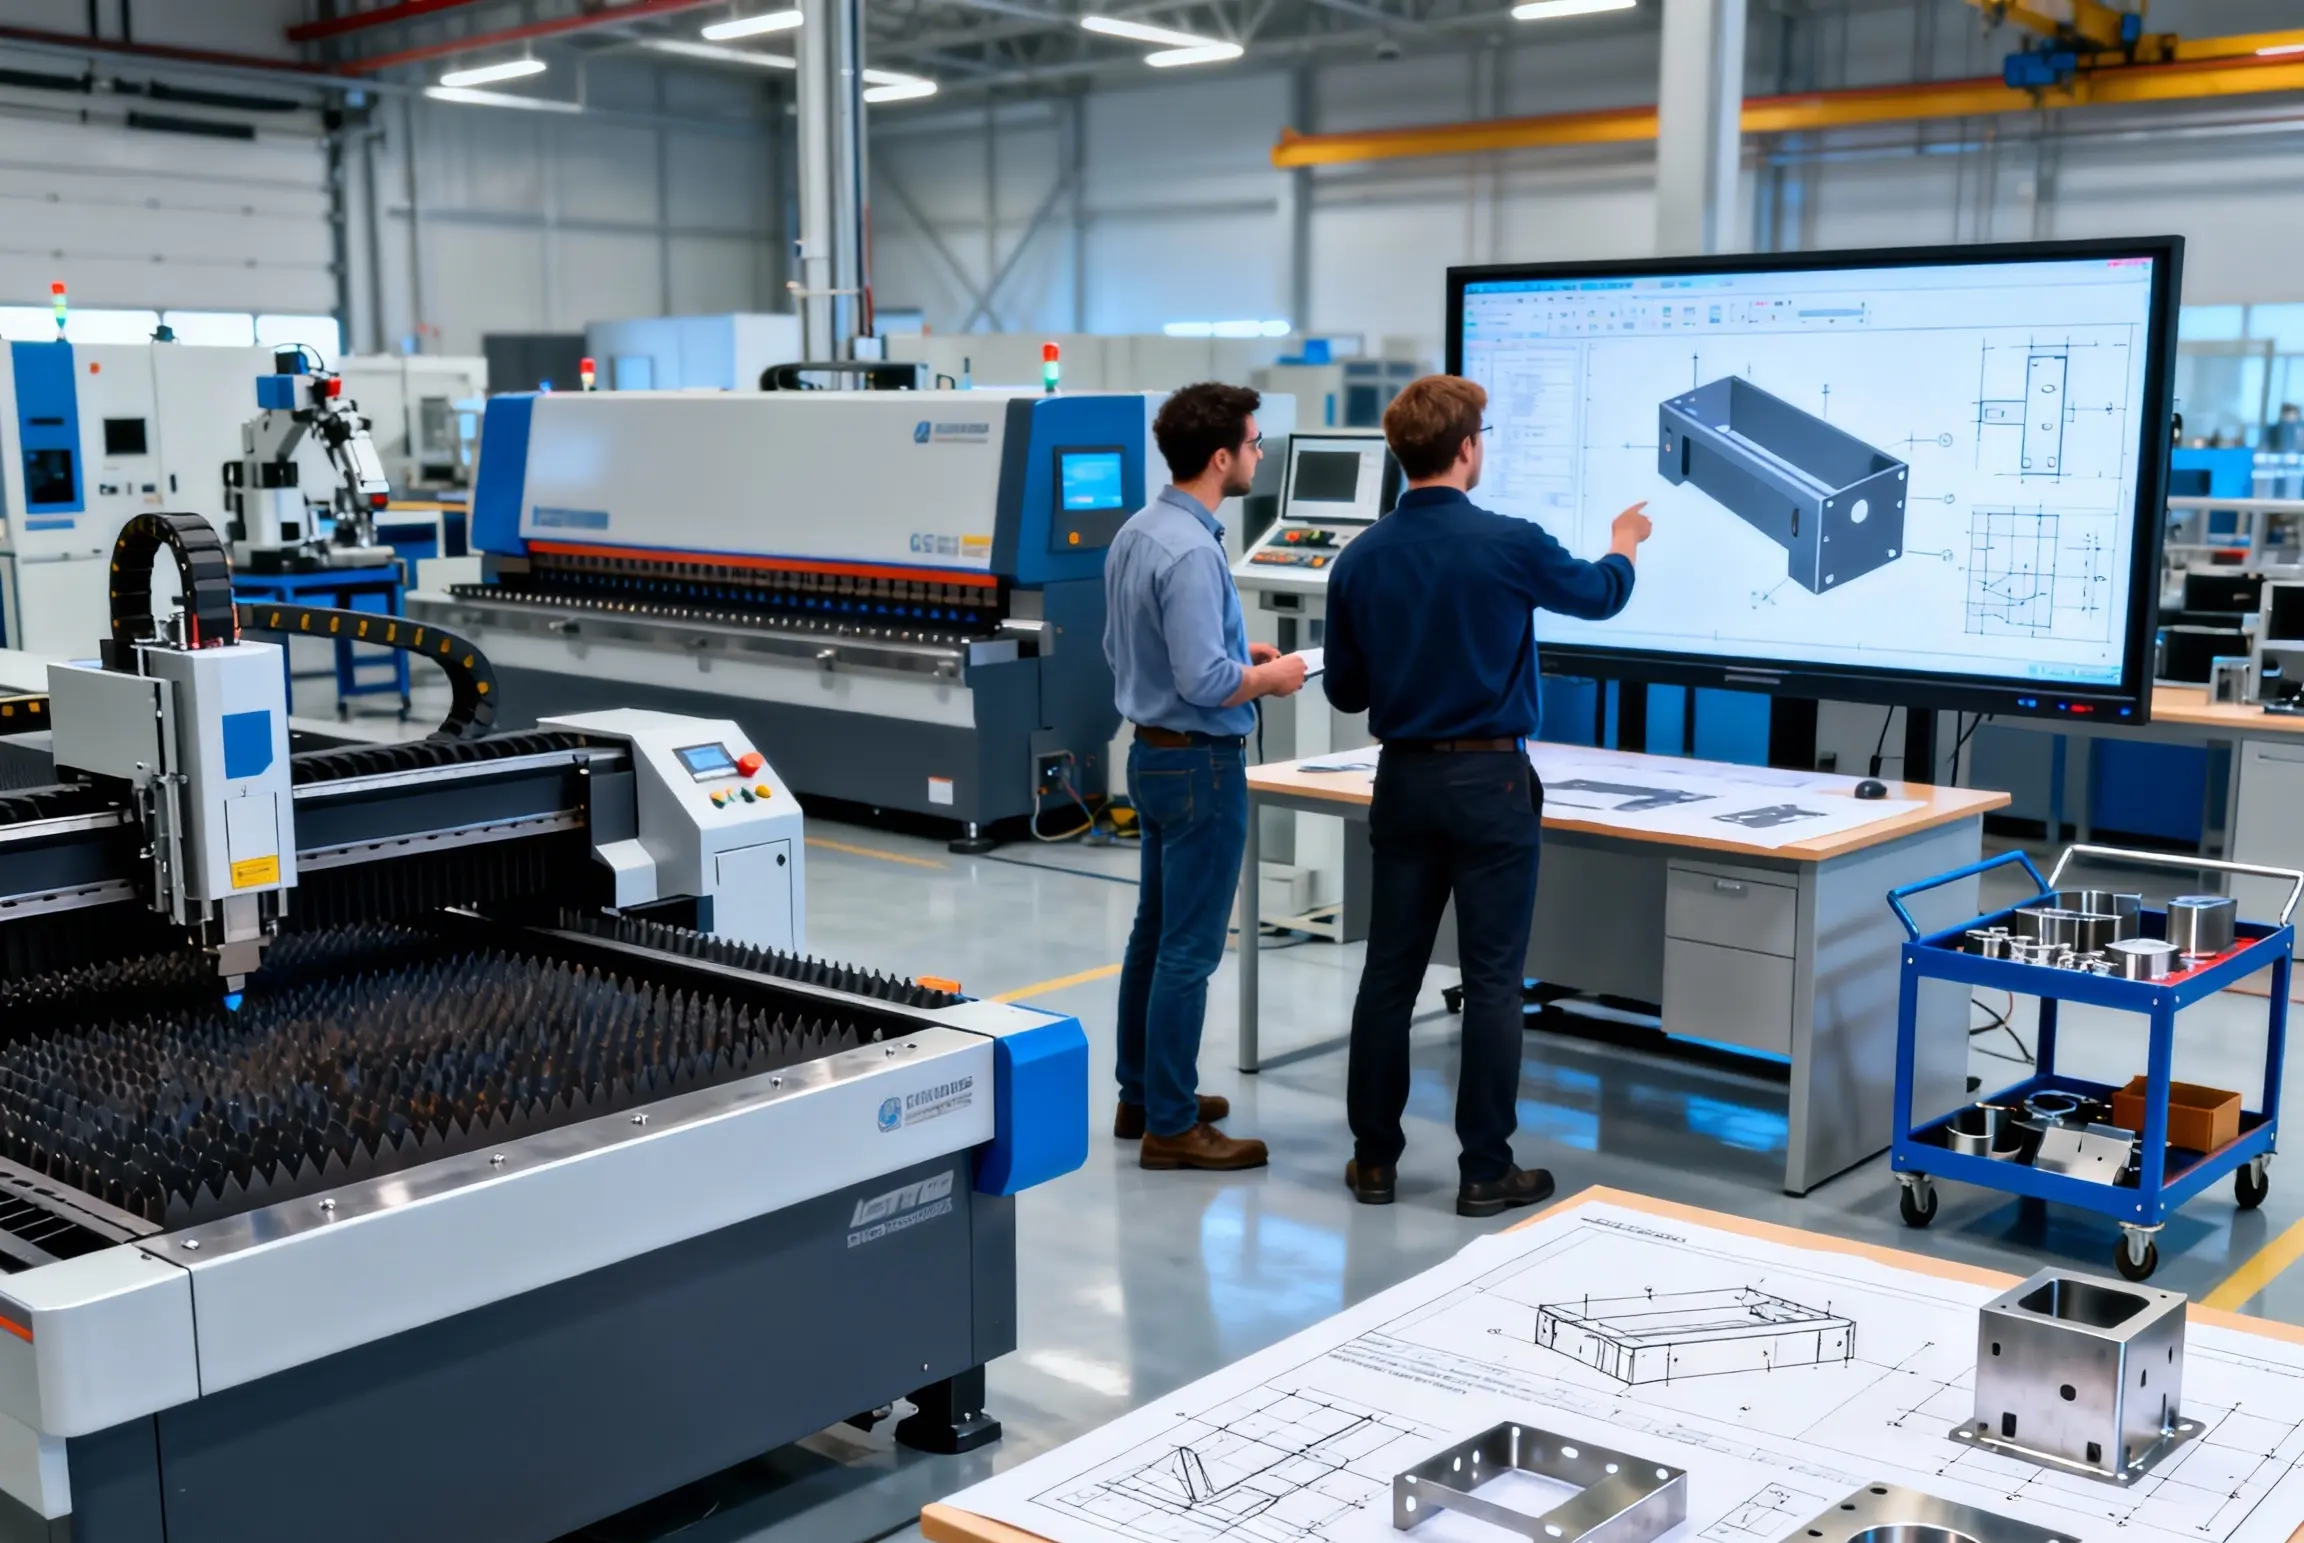
How We Control Laserschneiden Genauigkeit
Laserschneiden Quality Assurance Workflow
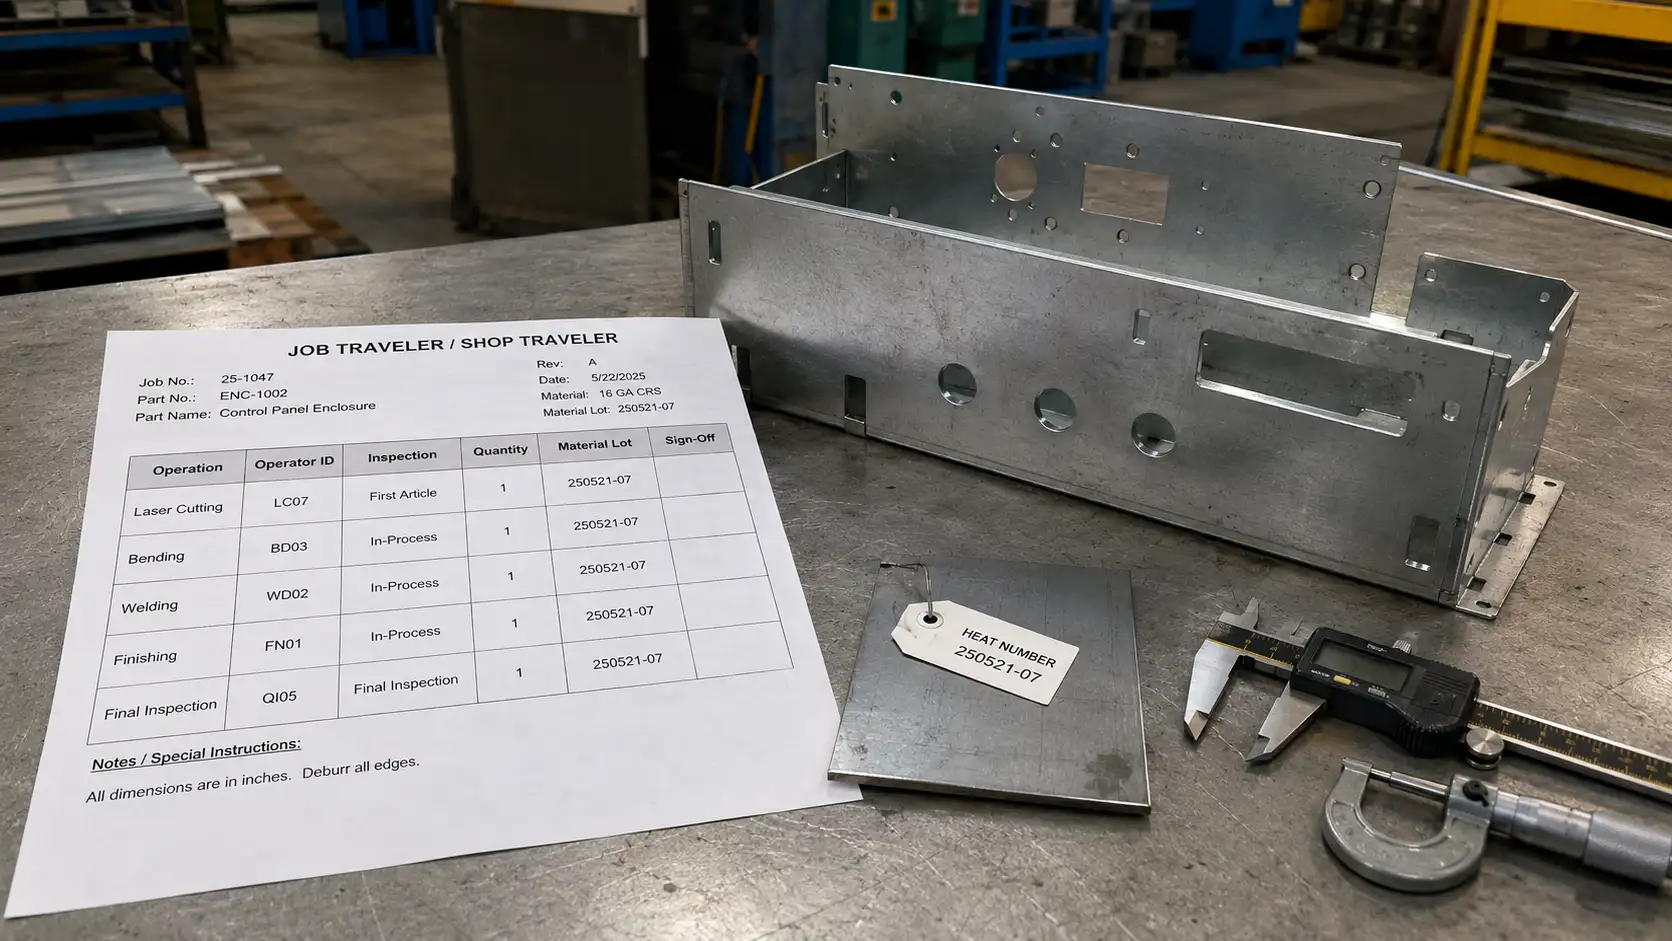
To ensure each batch meets the same high standard, SR MFG breaks laser cutting quality control into multiple stages, with traceable data points at each phase, ensuring consistent laser cutting precision und repeatable quality. This ensures that every laser-cut part, from the first to the last, remains consistent.
We run FAI at the start of every new order or material batch to verify key dimensions, edge quality, and plate thickness against our process window, ensuring the setup is ready for mass production.
We sample parts during production and apply SPC on critical features to detect dimensional drift, edge overheating, or equipment issues early—keeping the entire batch under control, not just a few good pieces.
Final dimensional checks, flatness and hole-position verification, plus protective packaging and random unpacking inspections ensure that parts arrive ready for bending, welding, or final assembly without rework.
DFM Review Before Laser Cutting
We don’t just “cut to print.” SR MFG works with you from CAD data to mass production, using DFM and engineering support to reduce redesigns, stabilize quality, and keep costs under control.
Upfront DFM Review
We review every CAD file for manufacturability, catching issues in holes, slots, ribs, and bend areas before the first sheet is cut.
01.Design Review
Check material, thickness, holes, slots, bend areas, and tolerance risks.
02.Prototype Validation
Use samples to verify fit, function, and process parameters before batch production.
03.Risk Control
Identify warping, burrs, tolerance stack-up, and edge-quality risks early.