
Kaltgewalztes Kohlenstoffstahlblech
& Enge Toleranzen
& Schweißeignung
& Leistung
Kaltgewalztes Kohlenstoffstahlblech verstehen: Die Grundlagen
Kaltgewalztes Kohlenstoffstahlblech existiert, weil Hersteller engere Toleranzen und gleichbleibendere Leistung wünschen. Es beginnt typischerweise mit warmgewalztem Coil, das gebeizt wird, um Walzhaut und Oberflächenoxide zu entfernen, dann kaltverfestigt auf die Zielstärke, und schließlich geglüht , um die Duktilität wiederherzustellen und das Material zu stabilisieren.
Im Vergleich zu warmgewalztem Stahl liefert kaltgewalztes Blech eine deutlich glattere Oberfläche, bessere Maßgenauigkeit, gleichmäßigere Dicke und konsistentere mechanische Eigenschaften—was es für anspruchsvolle Prozesse wie Stanzen und Präzisionsbiegen bestens geeignet macht.
Einfach gesagt: warmgewalzter Stahl ist “schruppbearbeitet”, während kaltgewalzter Stahl “präzisionsfertigbearbeitet” ist.” Wenn Aussehen und Genauigkeit wichtig sind, ist kaltgewalzter Stahl in der Regel die bessere Wahl.
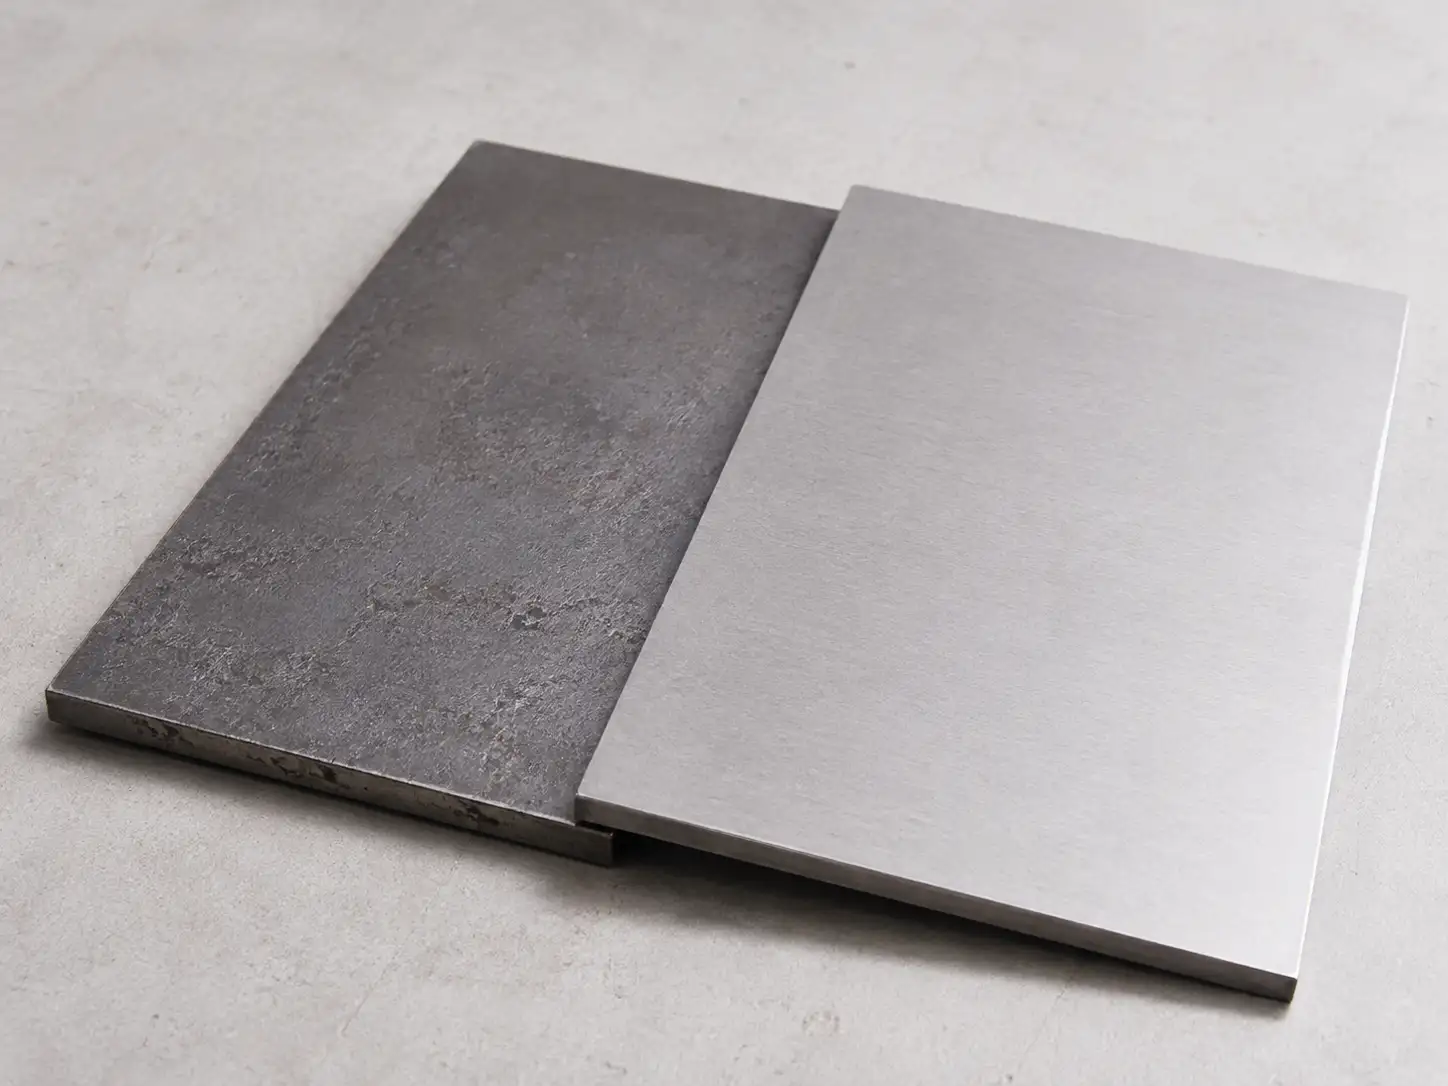
Hauptmerkmale von kaltgewalztem Kohlenstoffstahlblech
Normenrahmen
Kaltgewalztes Kohlenstoffstahlblech wird unter verschiedenen nationalen und regionalen Normen spezifiziert, jede mit ihrem eigenen Gütenbezeichnungssystem. Die wichtigsten Systeme, die im globalen Einkauf am häufigsten verwendet werden, umfassen China (GB/T), Japan (JIS), die Vereinigten Staaten (ASTM), Europa (EN) und alte deutsche DIN-Güten. Obwohl die Gütenbezeichnungen unterschiedlich sind, werden sie oft querverwiesen, um internationale Beschaffung und technische Kommunikation zu unterstützen.
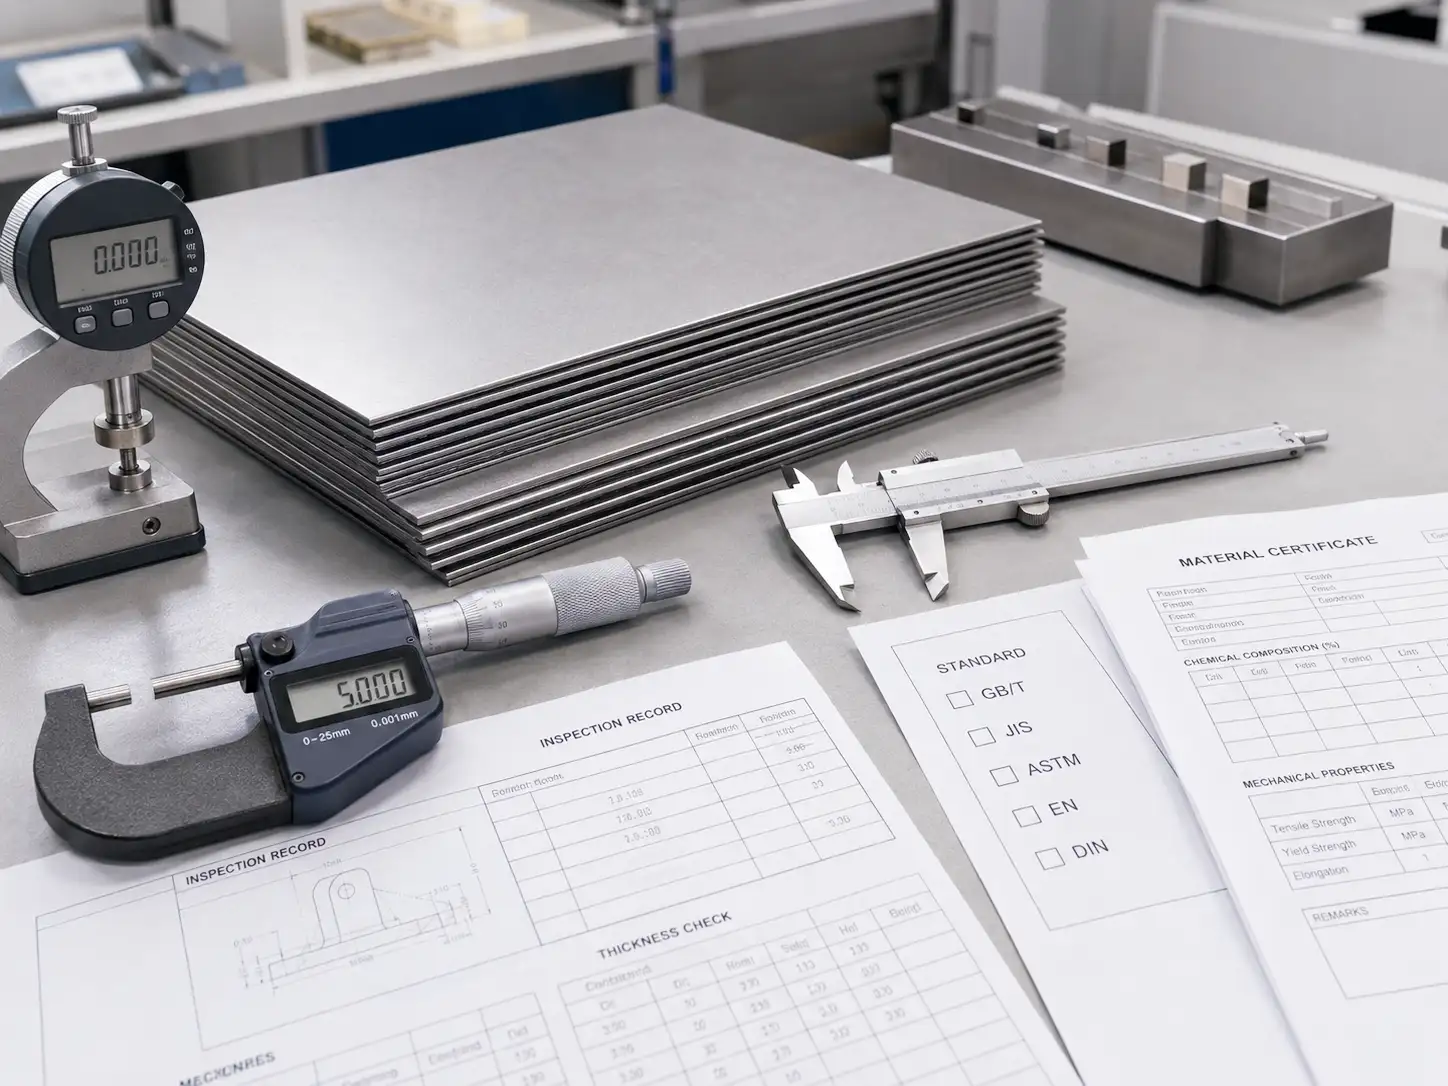
Internationale Güten-Querverweistabelle
Kaltgewalzte Kohlenstoffstahlgüten werden über Normen hinweg unterschiedlich benannt, aber die Äquivalenzbeziehungen werden weithin als praktische Referenz für globalen Einkauf und technische Diskussionen verwendet.
| Anwendungsklasse | Japan (JIS G3141) | China (GB/T) | Europa (EN 10130) | Deutschland (DIN 1623) | USA (ASTM A1008) |
|---|---|---|---|---|---|
| Handelsqualität (CQ) | SPCC | DC01 / Q195 | DC01 | St12 | CS Typ A/B/C |
| Ziehqualität (DQ) | SPCD | DC03 | DC03 | St13 | DS Typ A/B |
| Tiefziehqualität (DDQ) | SPCE | DC04 | DC04 | St14 | DDS |
| Extra-Tiefziehqualität (EDDQ) | SPCF | DC05 | DC05 | St15 | EDDS |
| Super-Extra-Tiefziehqualität (SEDDQ) | SPCG | DC06 | DC06 | St16 | EDDS |
Hinweise
- CQ = Handelsqualität
- DQ = Ziehqualität
- DDQ = Tiefziehqualität
- EDDQ = Extra-Tiefziehqualität
So wählen Sie die richtige Güte für die Blechbearbeitung
Auswahl basierend auf dem Umformprozess
| Verfahren | Empfohlene Güten | Warum sie gut geeignet ist |
|---|---|---|
| Einfaches Biegen, Stanzen | SPCC / DC01 | Kosteneffizient und ausreichend für allgemeine Umformanforderungen. |
| Mäßiges Biegen, leichtes Ziehen | SPCD / DC03 | Bessere Duktilität, geringeres Rissrisiko während der Umformung. |
| Tiefziehen, komplexe Umformung | SPCE / DC04 | Starke Tiefziehleistung, typischerweise mit höheren r-Werten für die Ziehfähigkeit. |
| Ultra-Tiefziehen, sehr komplexe Teile | SPCG / DC06 | Oft verbunden mit interstitial-free (IF) steel practice—best-in-class formability for demanding draws. |
Choose based on the end-use application
| Anwendung | Empfohlene Güten | Typical products |
|---|---|---|
| Electrical enclosures, chassis | SPCC / SECC | PC cases, electrical distribution boxes |
| Automotive outer panels (doors, hoods) | SPCE / DC04 / O5-grade | Passenger-car exterior panels |
| Appliance panels | SPCD / DC03 | Refrigerator door panels, washing machine panels |
| Oil pans, deep-drawn components | SPCE / DC06 | Automotive oil pans, filter housings |
| General structural parts | SPCC | Brackets, reinforcement plates |
| High-strength structural parts | HSLAS series (grade per spec) | Automotive structural parts |
Hinweis: If you’re not sure which grade fits your design and forming route, reach out to SR MFG—our engineers can help you choose the most suitable material and specification.
Key Specifications for Kaltgewalztes Kohlenstoffstahlblech
Chemische Zusammensetzung
The chemical makeup of cold-rolled carbon steel sheet has a direct impact on both mechanical properties and formability, so each grade is controlled within specified composition limits.
Typical Chemical Composition Limits (by Grade)
| Güte | C (%) | Mn (%) | P (%) | S (%) | Al (%) | Si (%) |
|---|---|---|---|---|---|---|
| SPCC / DC01 | ≤0.15 | ≤0.60 | ≤0.035 | ≤0.025 | — | ≤0.05 |
| SPCD / DC03 | ≤0.10 | ≤0.50 | ≤0.030 | ≤0.025 | ≥0.015 | ≤0.05 |
| SPCE / DC04 | ≤0.08 | ≤0.45 | ≤0.025 | ≤0.020 | ≥0.015 | ≤0.05 |
| SPCF / DC05 | ≤0.06 | ≤0.45 | ≤0.025 | ≤0.020 | ≥0.020 | ≤0.05 |
| SPCG / DC06 | ≤0.02 | ≤0.25 | ≤0.020 | ≤0.020 | — | ≤0.05 |
| CS Type B | 0.02–0.15 | ≤0.60 | ≤0.030 | ≤0.035 | — | — |
| DS Type B | ≤0.06 | ≤0.50 | ≤0.030 | ≤0.035 | — | — |
| DDS | ≤0.06 | ≤0.50 | ≤0.020 | ≤0.030 | — | — |
| EDDS | ≤0.04 | ≤0.40 | ≤0.020 | ≤0.025 | — | — |
How composition affects performance (what the elements do)
- Carbon (C): Lower carbon generally improves ductility and drawability. For example, SPCG (DC06) is often specified with very low carbon (≤0.02%), making it well suited for ultra-deep drawing applications.
- Manganese (Mn): Helps increase strength and toughness, but excessive Mn can reduce formability.
- Phosphorus (P) & Sulfur (S): Typically treated as harmful impurities—the lower, the better. Higher levels can increase brittleness (cold brittleness and hot shortness).
- Aluminum (Al): Commonly used as a deoxidizer to improve steel cleanliness and ductility. It can also help suppress strain aging, reducing the risk of property shifts after forming.
Mechanische Eigenschaften
Typical Mechanical Property Reference (ASTM A1008)
| Güte | Yield Strength (MPa) | Tensile Strength (MPa) | Elongation (%) | Hinweise |
|---|---|---|---|---|
| CS Type B (SPCC) | 140–275 | ≥270 | 28–40 | General-purpose; moderate strength |
| DS Type B (SPCD) | 140–240 | ≥270 | 30–42 | Drawing grade; better ductility |
| DDS (SPCE) | 115–200 | ≥270 | 38–42 | Deep drawing; higher r-value |
| EDDS (SPCG) | 105–170 | ≥270 | ≥40 | Extra-deep drawing; higher n-value |
| SS Grade 36 | ≥250 | 360 | 20–28 | Structural use; higher strength |
| HSLAS Grade 50 | ≥345 | ≥450 | ≥22 | High-strength low-alloy steel |
ASTM A1008 is a common reference for cold-rolled sheet and includes requirements related to yield strength, tensile strength, and elongation testing.
Elongation by Thickness (SPCC Reference)
| Nominal thickness (mm) | 0.25–0.30 | 0.30–0.40 | 0.40–0.60 | 0.60–1.0 | 1.0–1.6 | ≥1.6 |
|---|---|---|---|---|---|---|
| Elongation (%) | 25 | 28 | 31 | 34 | 36 | 37 |
What These Properties Mean
- Yield strength: The stress at which the material begins permanent (plastic) deformation. In general, lower yield strength forms more easily.
- Tensile strength: The maximum stress the material can withstand before fracture—an overall indicator of strength.
- Elongation: How much the material can stretch before breaking. Higher elongation generally means better formability; deep-drawn parts often target ≥40%.
- r-value (plastic strain ratio / Lankford coefficient): A measure of through-thickness thinning resistance during forming—higher r typically indicates better deep-draw performance.
- n-value (strain hardening exponent): Indicates how well the material can deform uniformly—higher n generally supports better stretch formability and reduces localized thinning.
Dimensional Specifications
General Size Range
| Parameter | Range | Common sizes | Hinweise |
|---|---|---|---|
| Dicke | 0.12–3.50 mm | 0.5 / 0.8 / 1.0 / 1.2 / 1.5 / 2.0 mm | Below 0.3 mm typically requires custom sourcing |
| Width | 400–1850 mm | 1000 / 1219 / 1250 / 1500 mm | Custom widths available per request |
| Sheet length | 1000–6000 mm | 2000 / 2438 / 3000 mm | 2438 mm = 8 ft |
| Coil weight | 3–20 tons | 5–15 tons | Custom coil weights available |
| Coil ID | 508 mm / 610 mm | 508 mm | Standard inner diameter |
Thickness Selection Guidelines
| Anwendung | Recommended thickness (mm) | Why |
|---|---|---|
| Appliance housings | 0.5–0.8 | Lightweight while meeting strength needs |
| PC chassis / enclosures | 0.6–1.0 | Good balance of stiffness and cost |
| Automotive door panels | 0.7–0.8 | Supports deep draw requirements and surface quality |
| Automotive oil pans | 1.5–2.0 | Thicker wall for higher strength |
| Structural parts | 1.5–3.0 | Higher stiffness for load-bearing use |
Dimensional Tolerances
Thickness Tolerance Standard
| Thickness range | Standard precision (PL.A) | Higher precision (PL.B) | Typical use |
|---|---|---|---|
| 0.3–0.4 mm | ±0.04 mm | ±0.03 mm | Precision stamped parts |
| 0.4–0.6 mm | ±0,05 mm | ±0.04 mm | Appliance panels |
| 0.6–1.0 mm | ±0.06 mm | ±0,05 mm | General structural parts |
| 1,0–2,0 mm | ±0.08 mm | ±0.06 mm | Thicker-gauge parts |
| 2.0–3.5 mm | ±0.10 mm | ±0.08 mm | Structural sheet |
Width Tolerance
| Edge condition | Width range | Permissible deviation | Hinweise |
|---|---|---|---|
| Slit edge (EC) | <1200 mm | 0 to +3 mm | Higher precision |
| Slit edge (EC) | 1200–1500 mm | 0 to +4 mm | Higher precision |
| Slit edge (EC) | >1500 mm | 0 to +5 mm | Higher precision |
| Mill edge (EM) | 730–1850 mm | 0 to +8 mm | Standard precision |
Length Tolerance (Sheets)
| Nominal length L | Standard precision (PL.A) | Higher precision (PL.B) |
|---|---|---|
| ≤2000 mm | 0 to +6 mm | 0 to +3 mm |
| >2000 mm | 0 to +0.003L | 0 to +0.0015L |
Flatness Requirement
| Flatness class | Flatness per meter | Typical use |
|---|---|---|
| Standard (PF.A) | ≤5 mm/m | General structural parts |
| Higher precision (PF.B) | ≤3 mm/m | Appliance housings, automotive parts |
Hardness Grades
Cold-rolled carbon steel sheet is commonly supplied in different temper (hardness) conditions depending on the annealing and temper-rolling route.
| Temper grade | HRB | HV | Characteristics | Typical applications |
|---|---|---|---|---|
| 1/8 Hard (8) | 50–71 | 95–130 | Relatively soft; suitable for light forming | Simple bent parts |
| 1/4 Hard (4) | 65–80 | 115–150 | Medium hardness with decent formability | General stamped parts |
| 1/2 Hard (2) | 74–89 | 135–185 | Harder with higher strength | Structural parts |
| Hard (1) | ≥85 | ≥170 | High hardness; limited formability | High-strength structural parts |
| Annealed (S) | — | 85–110 | Soft condition; best ductility | Tiefgezogene Teile |
| Full Hard (FH) | HRB ≥ 90 | HV ≥ 185 | Full hard; typically requires re-annealing for forming | Used for further rolling / as a substrate (e.g., for coated products) |
How to choose a hardness/temper
- Für Tiefziehen, use the Annealed (S) condition.
- Für general stamping, 1/4 Hard is often a practical choice.
- Für structural parts, consider 1/2 Hard oder Hard depending on forming needs.
- Full Hard material is typically selected as a base for downstream processing (and is generally not intended for forming unless re-annealed).
Surface Quality of Cold-Rolled Carbon Steel Sheets
Surface Finish Classification
Cold-rolled carbon steel sheets are typically classified into three finish levels based on surface quality requirements:
| Bezeichnung | Finish Level | Beschreibung | Typische Anwendungen |
|---|---|---|---|
| FB / O3 | Commercial Finish | Minor surface imperfections are permitted, provided they do not affect formability or coating adhesion. These may include light scratches, roll marks, shallow dents, minor pitting, or slight discoloration. | General structural components, internal parts, equipment frames |
| FC / O4 | Drawing Quality Finish | Of the two surfaces, the better side must be free of visible defects to the naked eye. The reverse side must at least meet FB requirements. | Appliance housings, automotive interior panels, enclosure exteriors |
| FD / O5 | Exposed Quality Finish | Of the two surfaces, the better side must be completely free of defects that could affect the appearance after painting or electroplating. The reverse side must at least meet FB requirements. | Automotive exterior panels (doors, hoods, trunk lids), high-end appliance panels |
Finish Selection Guidelines:
- O3 (FB): Suitable for structural components, internal equipment parts, or parts that will undergo powder coating or painting in subsequent processes where surface appearance is not critical.
- O4 (FC): Recommended for parts with moderate appearance requirements, such as appliance casings, automotive interior trim, and visible cabinet surfaces.
- O5 (FD): Required for automotive exterior panels with high appearance standards. In China, only a limited number of steel mills can consistently produce stable O5-grade material, including Shougang Cold Rolling, HBIS Handan, and Shougang Jingtang.
Surface Condition
| Code | Surface Type | Roll Treatment | Erscheinungsbild | Typische Anwendungen |
|---|---|---|---|---|
| D | Mattes Finish | Shot-blasted rolls | Uniform, fine-textured matte surface | Appliance panels, automotive outer panels |
| B | Bright Finish | Ground and polished rolls | Smooth, bright surface with high reflectivity | Precision components, electroplating substrates |
| — | Standard Finish | Standard rolls | Conventional mill finish | General-purpose applications |
Recommended Surface Combinations (for reference; final selection should be based on actual application requirements):
- Appliance exterior parts: D surface + FC/FD grade
- Automotive outer panels: D surface + FD grade
- General structural parts: Standard surface + FB grade
- Electroplating substrate: B surface + FC grade
Oberflächenrauheit
Surface roughness is a critical parameter in evaluating sheet metal surface quality, as it directly affects subsequent surface treatment performance.
| Anwendung | Recommended Ra | Inspektionsmethode |
|---|---|---|
| Cold-rolled substrate | ≤ 1.6 μm | Surface roughness tester |
| Deep drawing grade (DC04 and above) | ≤ 0.8 μm | Surface roughness tester |
| O5 automotive panels | ≤ 0.6 μm | Surface roughness tester |
| Laser-cut edge | ≤ 12.5 μm | Surface roughness tester |
| Bent surface | ≤ 6.3 μm | Surface roughness tester |
Impact of Improper Surface Roughness on Subsequent Processing
- Excessive roughness: May cause orange peel or sagging during powder coating and can reduce plating adhesion.
- Insufficient roughness: Can lead to poor coating adhesion and potential peeling.
- Rough laser-cut edges: May negatively affect appearance and create localized stress concentrations.
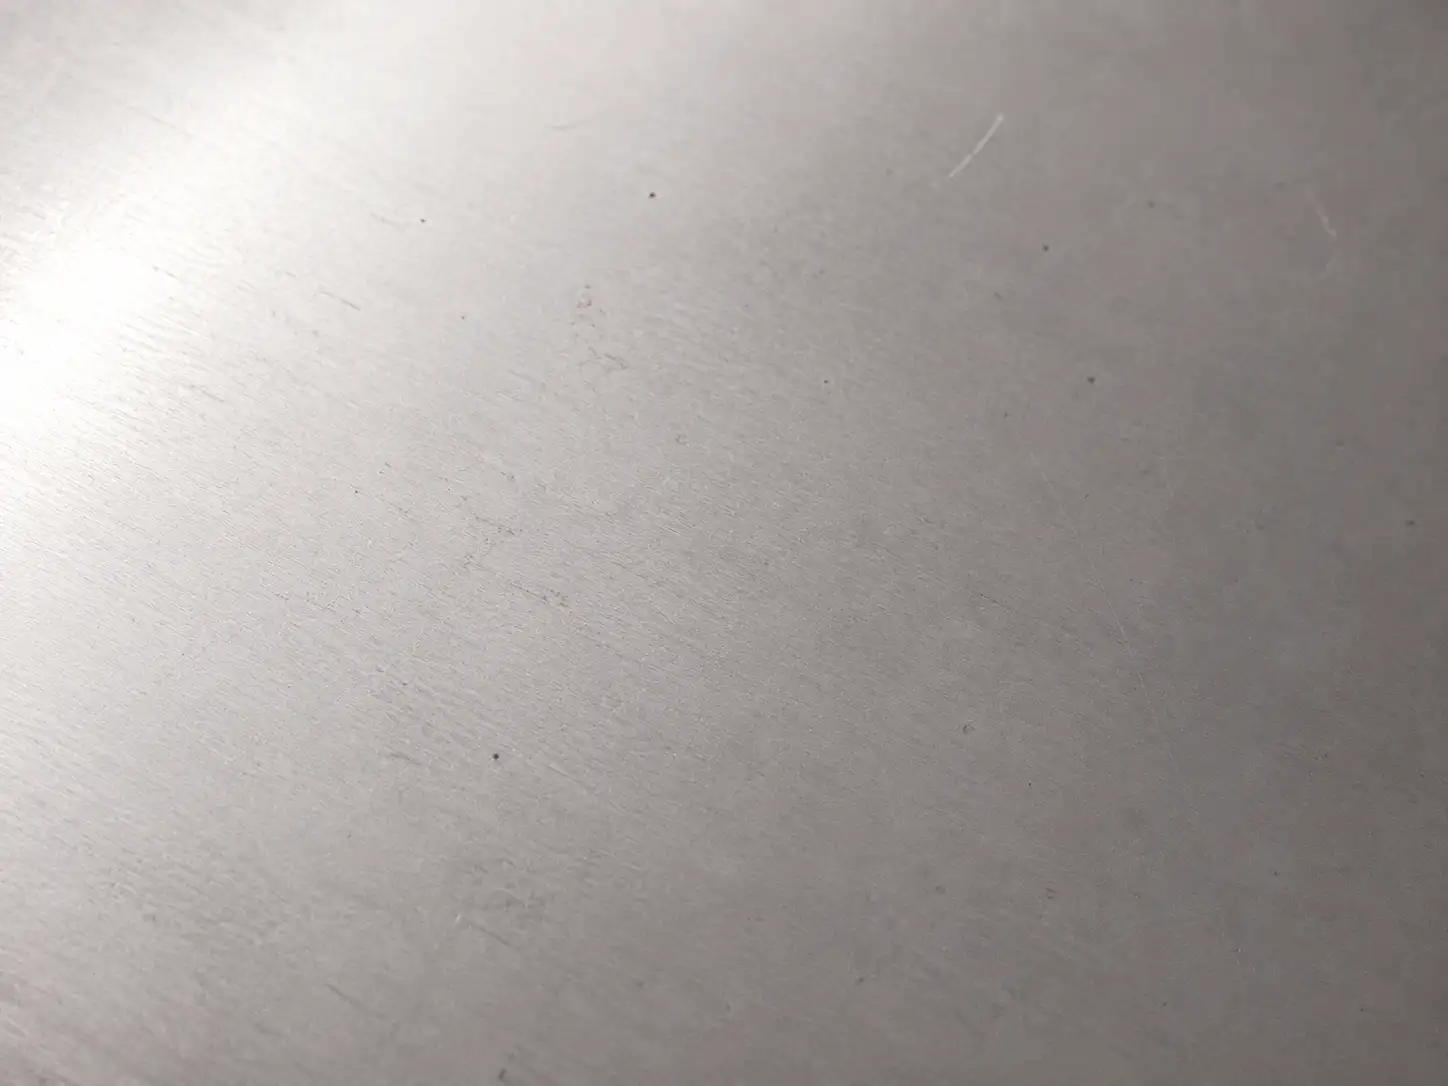
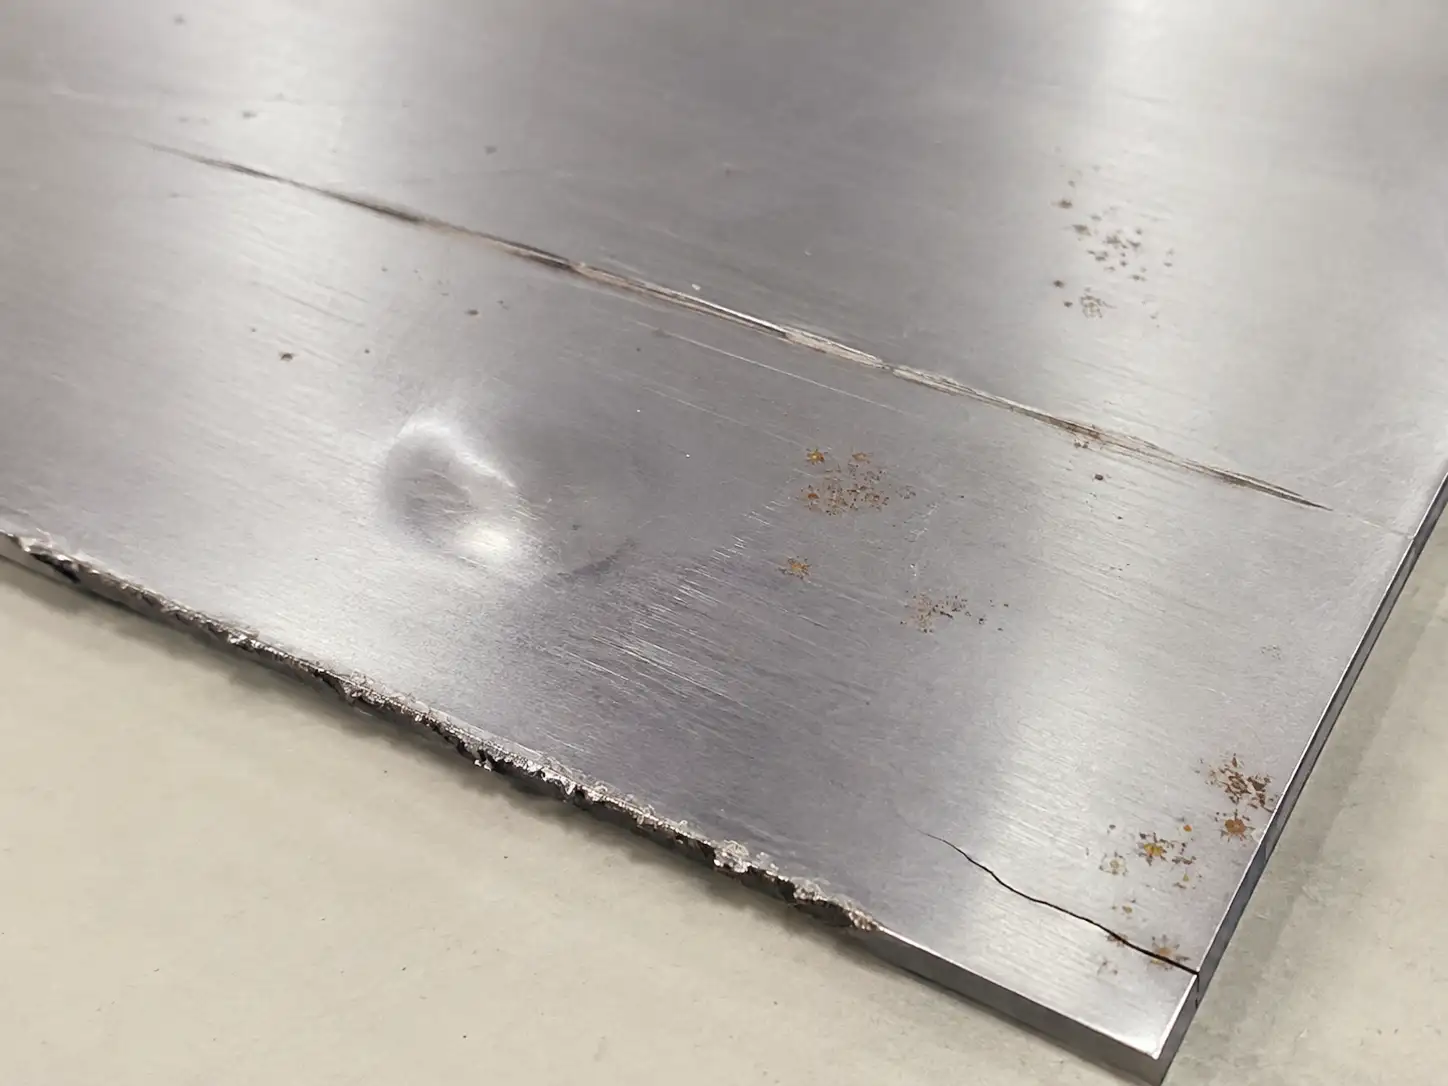
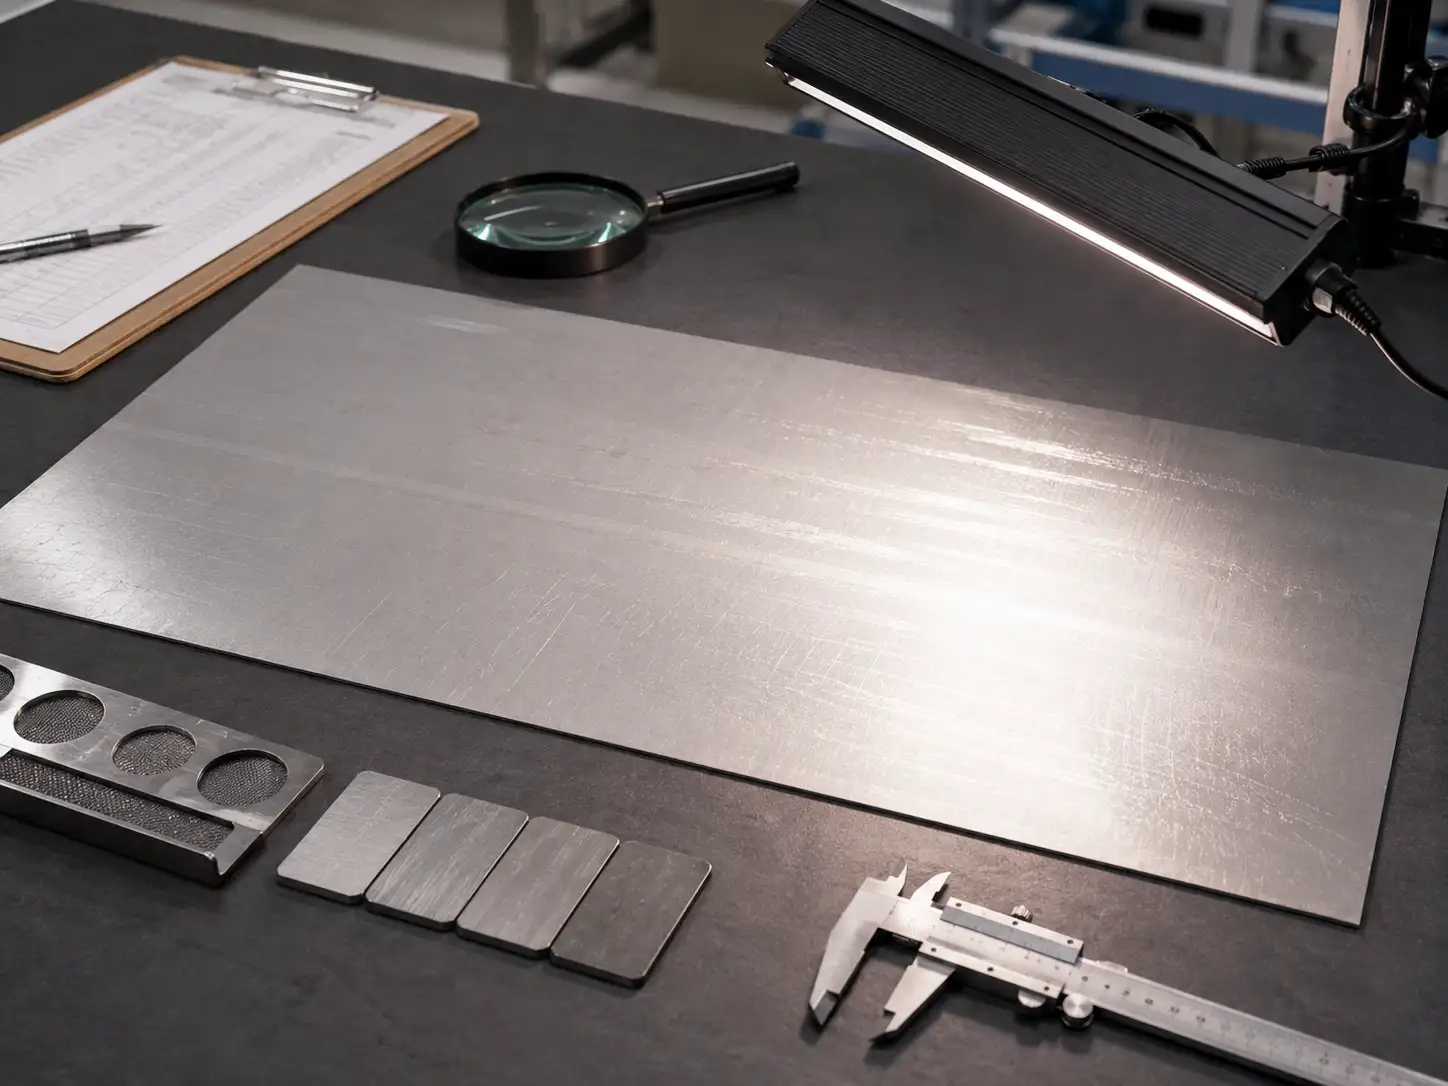
Surface Defect Control
Forming Processes
Cold-rolled carbon steel offers excellent formability, making it suitable for components with varying levels of geometric complexity.
Biegen
Biegen is one of the most widely used sheet metal operations, and cold-rolled steel performs reliably in press brake forming.
| Parameter | Recommended Value | Hinweise |
|---|---|---|
| Minimum bend radius | ≥ 1.0t (t = sheet thickness) | Too small a radius can cause cracking. |
| Minimum flange length | ≥ 1.5t + bend radius | If the flange is too short, clamping becomes difficult and bending may fail. |
| Springback compensation | 1–3° | Adjust based on material grade and bend angle. |
| V-die opening (V-width) | 6–10 × sheet thickness | Select die size based on sheet thickness. |
Stanzen
Cold-rolled steel sheet is one of the most suitable materials for Stanzen. Select the appropriate grade based on product complexity, then apply the required stamping operations.
| Stamping Type | Recommended Grade | Key Parameters |
|---|---|---|
| Simple blanking | SPCC / DC01 | Blanking clearance: 0.05–0.08t |
| General forming | SPCD / DC03 | Draw ratio ≥ 0.7 |
| Deep drawing | SPCE / DC04 | Draw ratio ≥ 0.6 |
| Extra-deep drawing | SPCG / DC06 | Draw ratio ≥ 0.55 |
Schweißverfahren
Cold-rolled carbon steel sheet offers good weldability and supports a variety of welding methods, as shown below.
| Schweißverfahren | Suitability | Weld Quality | Typische Anwendungen |
|---|---|---|---|
| GTAW (TIG) | Very good | Clean, attractive welds; minimal distortion | Precision parts, appearance-critical parts |
| CO₂ shielded welding | Gute | High efficiency, low cost | Structural parts, mass production |
| Punktschweißen | Gute | Ideal for lap joints on thin sheet | Automotive bodies, home appliances |
| Laserstrahlschweißen | Ausgezeichnet | High precision, small heat-affected zone | Precision components |
| MIG welding | Very good | High welding speed | Medium-thickness sheet |
Common Welding Issues and Fixes
| Issue | Cause | Solution |
|---|---|---|
| Porosity | Insufficient shielding gas flow; oil/contamination on surface | Increase shielding gas flow; clean the joint area |
| Undercut | Current too high; travel speed too fast | Reduce current; slow down travel speed |
| Hot cracking | Carbon content too high; cooling too fast | Use low-carbon steel; control the cooling rate |
| Excessive distortion | Poor weld sequence; too much heat input | Optimize weld sequence; use skip/segment welding |
Surface Finishing Processes
Cold-rolled carbon steel sheet does have a downside: its corrosion resistance isn’t very strong. In most cases, a surface treatment is needed to extend service life.
Phosphate Coating
| Parameter | Anforderung |
|---|---|
| Beschichtungsdicke | 2–5 μm |
| Erscheinungsbild | Uniform gray film |
| Haftung | Cross-hatch test: Class 1 |
| Korrosionsbeständigkeit | Neutral salt spray ≥ 24 hours |
Electrostatic Powder Coating
| Parameter | Anforderung |
|---|---|
| Beschichtungsdicke | 60–120 μm |
| Erscheinungsbild | No runs/sags, no pinholes, no orange peel |
| Härte | HV ≥ 400 |
| Korrosionsbeständigkeit | Neutral salt spray ≥ 72 hours |
| Haftung | Cross-hatch test: Class 1 |
E-Coating (Electrophoretic Deposition)
| Parameter | Anforderung |
|---|---|
| Beschichtungsdicke | 15–30 μm |
| Erscheinungsbild | Uniform and smooth |
| Härte | Better than powder coating |
| Korrosionsbeständigkeit | Neutral salt spray ≥ 240 hours |
Electro-Galvanizing
| Parameter | Anforderung |
|---|---|
| Beschichtungsdicke | 5–10 μm |
| Erscheinungsbild | Uniform silver-gray finish |
| Korrosionsbeständigkeit | Neutral salt spray ≥ 48 hours |
| Elektrische Leitfähigkeit | Ausgezeichnet |
Hot-Dip Galvanizing (SGCC)
| Parameter | Anforderung |
|---|---|
| Beschichtungsdicke | 8–15 μm |
| Erscheinungsbild | Spangle pattern or bright silver finish |
| Korrosionsbeständigkeit | Neutral salt spray ≥ 96 hours |
Quick Guide for Choosing a Surface Finish
Industry Application Examples for Cold-Rolled Carbon Steel Sheet
Home Appliance Industry
| Produkt | Recommended Material | Dickenbereich | Oberflächenbehandlung | Key Requirements |
|---|---|---|---|---|
| Refrigerator door panel | SPCC / DC03 | 0.5–0.6 mm | Powder coating / pre-painted | High surface quality; good flatness |
| Refrigerator side panel | SECC / SGCC | 0.5–0.8 mm | Pulverbeschichtung | Strong corrosion resistance |
| Washing machine inner tub | SPCD / SECC | 0.8–1.2 mm | Galvanizing + plastic coating | Good deep-draw performance |
| Washing machine cabinet | SPCC / SGCC | 0.8–1.0 mm | Pulverbeschichtung | Good appearance |
| Air conditioner housing | SPCC / SGCC | 0.8–1.5 mm | Pulverbeschichtung | Corrosion protection + appearance |
| Microwave oven housing | SECC | 0.6–0.8 mm | Powder coating / as-is | Korrosionsbeständigkeit |
| PC chassis | SECC | 0.6–1.0 mm | Powder coating / as-is | EMI shielding |
| TV back panel | SPCC | 0.5–0.8 mm | Pulverbeschichtung | Low cost |
Automobilindustrie
| Component | Recommended Material | Dicke | Oberflächenqualität | Key Performance Requirements |
|---|---|---|---|---|
| Inner door panel | DC03 / DC04 | 0.7–1.0 mm | FB/FC | Deep drawability |
| Outer door panel | DC04 / O5 grade | 0.7–0.8 mm | FD | High surface quality |
| Hood | DC04 / O5 grade | 0.8–1.0 mm | FD | Appearance + dent resistance |
| Decklid (trunk lid) | DC06 | 0.7–0.9 mm | FD | Extra-deep drawability |
| Roof panel | DC04 / O5 grade | 0.7–0.8 mm | FD | Flatness over large areas |
| Outer side panel | DC04 / O5 grade | 0.7–0.9 mm | FD | Large-radius / complex curvature forming |
| Floor pan | High-strength steel | 1,2–2,0 mm | FB | High strength |
| Oil pan | DC06 | 1.5–2.0 mm | FB | Extra-deep drawability + leak resistance |
| Seat frame | High-strength steel | 1.5–3.0 mm | FB | Strength + safety |
Telecom Equipment Industry
| Produkt | Recommended Material | Dicke | Oberflächenbehandlung | Key Requirements |
|---|---|---|---|---|
| Server cabinet | SPCC / SGCC | 1.5–2.5 mm | Pulverbeschichtung | Strength + corrosion resistance |
| Power distribution cabinet | SGCC | 1,2–2,0 mm | Pulverbeschichtung | Corrosion resistance + safety |
| Network cabinet | SPCC / SGCC | 1,0–2,0 mm | Pulverbeschichtung | Strength + appearance |
| Battery cabinet | SGCC | 1.5–2.5 mm | Heavy-duty powder coating | High corrosion resistance |
| Outdoor base station | SGCC | 2.0–3.0 mm | Heavy-duty powder coating | Weather resistance |
| Equipment frame | SPCC | 1.0–1.5 mm | Phosphate + powder coating | Strength + cost |
Building and Architectural Applications
| Produkt | Recommended Material | Dicke | Oberflächenbehandlung | Key Requirements |
|---|---|---|---|---|
| Metal ceiling panels | SPCC | 0.5–0.8 mm | Powder coating / pre-painted | Flatness + appearance |
| Curtain wall panels | SPCC / SGCC | 1.0–2.5 mm | Powder coating / fluorocarbon coating | Weather resistance |
| Metal partitions | SPCC | 0.8–1.2 mm | Pulverbeschichtung | Appearance + strength |
| Railings and handrails | SPCC / SGCC | 1.5–2.5 mm | Powder coating / galvanizing | Safety + corrosion resistance |
Hardware and Metal Products
| Produkt | Recommended Material | Dicke | Oberflächenbehandlung | Key Requirements |
|---|---|---|---|---|
| Toolbox | SPCC / SECC | 0.8–1.5 mm | Powder coating / electro-galvanizing | Flatness + appearance |
| Metal enclosure/case | SECC / SGCC | 0.8–1.2 mm | Electro-galvanizing | Weather resistance |
| Filing cabinet | SECC | 0.6–1.0 mm | Pulverbeschichtung | Appearance + strength |
| Shelving | SPCC / SGCC | 1,0–2,0 mm | Pulverbeschichtung | Safety + corrosion resistance |
| Hardware parts | SPCC | 0.5–1.5 mm | Electro-galvanizing | Precision + corrosion resistance |
Cost Breakdown for Cold-Rolled Carbon Steel Sheet
Material Costs
- 1
Raw materials: 60–70% of total cost
- 2
Pricing is heavily affected by fluctuations in steel billet und warmgewalztem Coil prices
- 3
Typical grade pricing trend: SPCC < SPCD < SPCE
Processing Costs
- 1
Cold rolling: 10–15%
- 2
Annealing, temper rolling (skin-pass), and oiling: 5–10%
- 3
Cut-to-length and slitting: 3–5%
Packaging and Transportation
- 1
Packaging: 2–3%
- 2
Domestic transportation: 1–2%
- 3
Ocean freight: Not included in FOB pricing; included in CIF pricing
Overhead and Profit
- 1
Administrative overhead: 3–5%
- 2
Financing costs: 2–3%
- 3
Profit margin: 5–10%
Key Factors That Affect Pricing
| Faktor | Impact Level | Hinweise |
|---|---|---|
| Raw material prices | Hoch | Driven by swings in iron ore and coke prices |
| Market supply and demand | Mäßig | Prices typically rise during peak seasons |
