A Ein Folgeverbundwerkzeug für einen Automobilhalter kann fünf bis acht Korrekturschleifen durchlaufen, bevor es ein Teil produziert, das die Maßprüfung besteht. Ein einfaches Flachstanzwerkzeug benötigt möglicherweise nur eine.
Der Unterschied ist kein Zufall — es ist der Probebetriebsprozess, und wie gut jede Korrekturschleife ausgeführt wird, bestimmt, ob das Werkzeug mit Zuversicht oder mit Risiko in die Produktion geht.
Der Werkzeugprobebetrieb wird oft als abschließende Checkliste im Werkzeugentwicklungszeitplan behandelt. Das Werkzeug wird gebaut, es kommt auf die Presse, Teile kommen heraus, jemand gibt frei.
In der Realität ist der Probebetrieb eine iterative technische Validierung, bei der das Werkzeug unter realen Produktionsbedingungen getestet, gemessen, korrigiert und erneut getestet wird.
Das Ziel ist nicht, ein akzeptables Teil zu produzieren — es ist der Nachweis, dass das Werkzeug konsistent akzeptable Teile produzieren kann, Schicht für Schicht, bei der Tonnage und Geschwindigkeit, die die Produktion erfordert.
Was der Werkzeug-Probebetrieb tatsächlich validiert
Der Werkzeugprobebetrieb wird manchmal als “die ersten Teile fahren” beschrieben, aber das unterschätzt, was tatsächlich bewertet wird.
Ein strukturierter Probebetrieb validiert drei Dinge gleichzeitig: das Werkzeug, den Prozess und das Teil.
Das Werkzeug selbst muss korrekt funktionieren — Ober- und Unterteil fluchten, Schneidspalte sind gleichmäßig, Umformflächen haben ordnungsgemäßen Kontakt, und alle beweglichen Komponenten (Abstreifer, Heber, Druckpolster) funktionieren ohne Verklemmen oder übermäßigen Verschleiß.
Der Prozess muss stabil sein — Bandzuführung ist zuverlässig, Teiletransfer zwischen den Stationen ist konsistent, Zykluszeit ist erreichbar, und Pressentonnen bleibt innerhalb sicherer Grenzen.
Und das Teil muss der Spezifikation entsprechen — Abmessungen, Oberflächenqualität, Umformintegrität und Wiederholbarkeit über mehrere Läufe.
Wenn eine dieser drei Dimensionen versagt, ist das Werkzeug nicht produktionstauglich.
Ein Teil, das korrekt aussieht, aber um 0,3 mm zwischen den Läufen variiert, ist ein Prozessproblem.
Ein Werkzeug, das bei niedriger Geschwindigkeit gute Teile produziert, aber bei Produktionsgeschwindigkeit die Oberfläche markiert, ist ein Werkzeugproblem.
Der Probebetrieb ist der Ort, an dem diese Unterscheidungen sichtbar werden.
Die Probebetriebssequenz — Vom Pressenaufbau bis zu freigegebenen Mustern
Ein vollständiger Probebetrieb folgt einer strukturierten Sequenz.
Das Überspringen von Schritten oder deren überstürzte Durchführung ist die häufigste Ursache für Nacharbeit in späten Phasen.
Pressenaufbau und erster Hub
Das Werkzeug wird auf der Probepresse installiert, die der Zielproduktionspresse so nah wie möglich entsprechen sollte — gleiche Tonnagekapazität, Hubhöhe, Tischgröße und Polstertyp.
Presseneinstellungen (Einbauhöhe, Polsterdruck, Hubgeschwindigkeit) werden angepasst, um eine Grundlinie festzulegen.
Der erste Hub wird bei reduzierter Geschwindigkeit gefahren, um die grundlegende Werkzeugfunktion zu überprüfen — keine Interferenz, keine abnormalen Kraftspitzen, keine Fehlausrichtung.
Erstmusterprüfung
Der Der Erstmusterprüfungsprozess beginnt mit der visuellen und dimensionalen Prüfung der ersten Muster.
Die visuelle Prüfung erkennt offensichtliche Defekte — Risse, starke Falten, tiefe Kratzer, Grat an Schnittkanten.
Die dimensionale Prüfung verwendet KMG (Koordinatenmessgerät), 3D-Laserscanning oder Prüfvorrichtungen, um das Teil mit dem CAD-Modell zu vergleichen.
In dieser Phase, ist das Ziel nicht Perfektion — es ist, eine Karte zu erstellen, was korrigiert werden muss und wo.
Werkzeugeinpassung und Kontaktprüfung
Vor der Durchführung von Korrekturen muss der Werkzeugmacher das Kontaktmuster auf den Umformflächen verstehen.
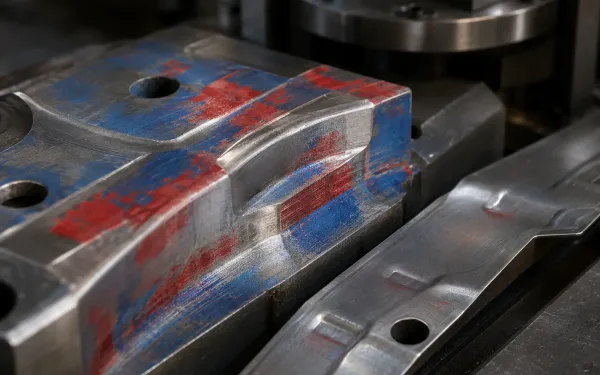
Rot und blau aufgetragene Tuschierpaste auf einer Werkzeugfläche zeigt ungleichmäßige Kontaktmuster — helle Übertragungsbereiche zeigen Hochdruckzonen an, während unberührte Bereiche unzureichenden Kontakt anzeigen, der korrigiert werden muss.
Rote oder blaue Tuschierpaste wird auf das Blech oder die Werkzeugfläche aufgetragen. Wenn das Werkzeug schließt, überträgt sich die Paste und zeigt Bereiche mit hohem und niedrigem Kontakt — Stellen, an denen der Druck konzentriert ist, und Stellen, an denen die Oberfläche keinen ordnungsgemäßen Kontakt herstellt.
Dieser Schritt ist besonders kritisch für Zieh- und Umformoperationen, bei denen der Oberflächenkontakt direkt den Materialfluss und die Teileform steuert.
Ausführung der Korrekturschleife
Dies ist der Kern des Probebetriebs.
Basierend auf Prüfdaten und Einpassungsergebnissen führt der Werkzeugmacher Korrekturen am Werkzeug durch.
Häufige Korrekturen umfassen:
- Grinding forming surfaces to adjust material flow or reduce springback in specific areas
- Adding shims under inserts or pressure pads to change local pressure distribution
- Welding and re-machining to add material where the die surface has been cut too deep
- Adjusting cutting clearances by re-grinding punch or die sections
- Modifying draw beads or stretchers to control metal flow into deep-draw areas
After each correction, the die is re-stamped and the new parts are inspected.
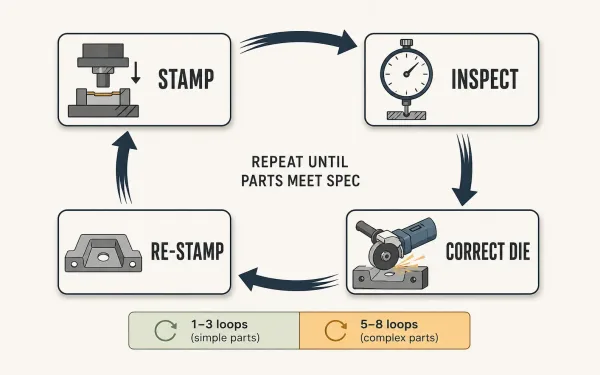
The core tryout correction loop cycles through four stages — stamp a part, inspect it against specification, correct the die, then stamp again — repeating until all dimensional and quality criteria are met.
This loop repeats — stamp, inspect, correct, stamp again — until the parts meet specification consistently.
For complex geometries, five to eight loops are typical. For simple parts, one to three may be enough.
The critical skill in this phase is knowing was to correct.
A dimensional deviation might be caused by springback (a material behavior), insufficient forming pressure (a process setting), or an incorrect die surface (a tooling error).
Each cause requires a different correction.
Misdiagnosing the root cause wastes loops and adds cost.
Final Validation and Approval
Once the die produces parts that meet all defined Fertigungsqualitätsanforderungen over a specified number of consecutive runs — typically 5 to 30 parts depending on project requirements — the tryout moves to final validation.
Samples go through a documented Qualitätskontroll- und Inspektionsprozess before they are submitted to the customer for approval.
Some projects require a formal PPAP (Production Part Approval Process) or equivalent sign-off.
Was geprüft wird — und wie
Tryout inspection is not a single pass — it is a layered process that catches different types of defects at different stages.
Forming Quality
Forming defects are the most visible and the most consequential.
Wrinkling indicates insufficient blank holder pressure or poor material flow control.
Thinning — measured by ultrasonic thickness gauges or sectioning — shows where the material has been stretched beyond its forming limit.
Cracking, the most severe failure, means the material has exceeded its elongation capacity in a specific area.
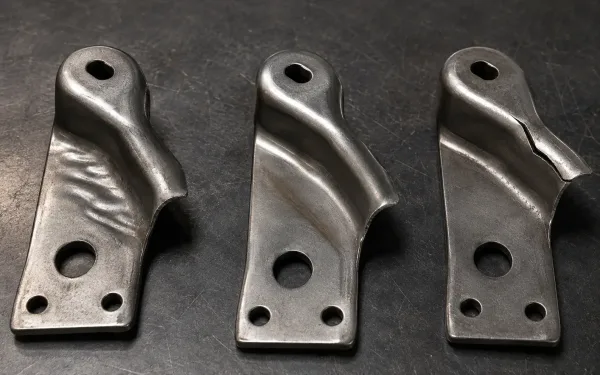
Three stamped parts from the same tryout run displaying common forming defects: (left) surface wrinkling from insufficient blank holder pressure, (center) thinning marks visible under raking light, (right) edge cracking at a tight-radius flange where material exceeded its elongation limit.
These defects often appear in combination.
A part might wrinkle in one area and crack in another, which points to a material flow imbalance rather than a simple pressure adjustment.
Dimensional Accuracy
CMM inspection measures the part against the CAD model at defined control points — hole positions, surface profiles, flange angles, and assembly reference features.
3D scanning provides a full-surface comparison, useful for identifying warpage or twist that point measurements might miss.
Checking fixtures offer a faster, production-oriented way to verify key features against go/no-go criteria.
Trim and Pierce Quality
Cut edge quality is evaluated by burr height, edge rollover, and shear band percentage.
Excessive burr usually indicates worn cutting clearances or misaligned punch-to-die alignment.
In progressive die metal stamping, trim and pierce stations are among the first to show wear, so their condition during tryout sets the baseline for tool life expectations.
Springback Behavior
Springback — the tendency of formed parts to spring back toward their original shape after the forming load is removed — is the most persistent challenge in die tryout.
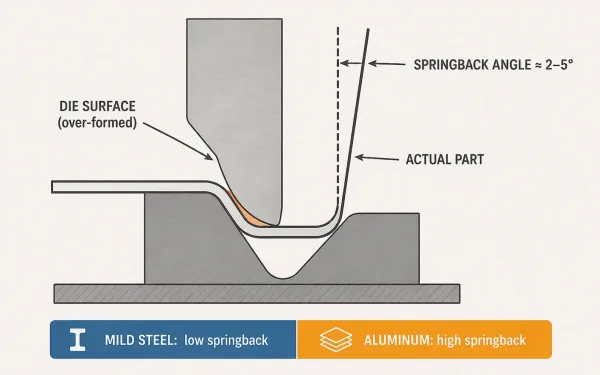
Cross-section view illustrating springback behavior: the dashed line shows the intended die shape, the solid outline shows the actual part after springback, and the orange zone indicates the over-form compensation built into the die surface to counteract material elastic recovery.
It is material-dependent, geometry-dependent, and process-dependent.
Aluminum alloys spring back more than mild steel. Tight-radius bends spring back more than gradual curves.
The toolmaker compensates by over-forming the die surface, but the exact amount requires iterative testing during tryout.
Wie Material und Dicke die Probebetriebsgleichung verändern
Not all materials behave the same during tryout, and this directly affects how long the process takes and how many correction loops are needed.
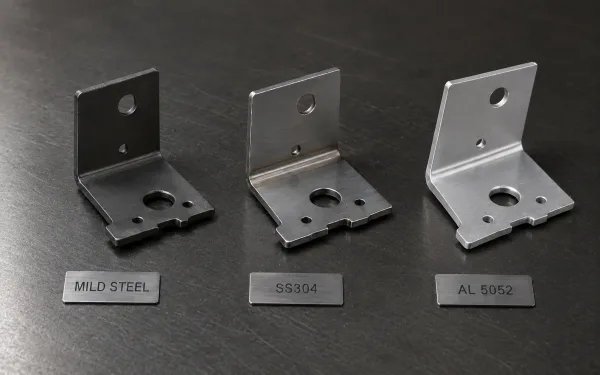
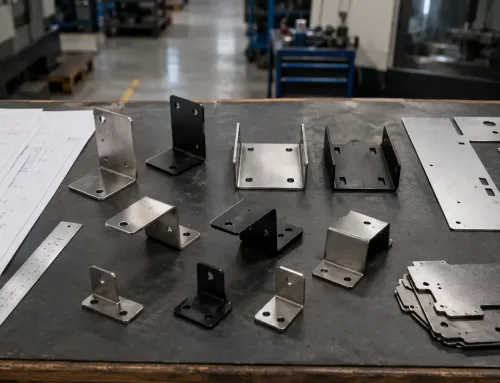
Three bracket parts stamped from the same die using different materials. Left: mild steel with minimal springback and close conformance. Center: stainless steel 304 with slight work-hardening marks. Right: aluminum 5052 with noticeable flange angle deviation due to higher springback.
Aluminum alloys (such as 5052-H32 or 6061-T6) have higher springback than carbon steel, which means the die surface needs more aggressive over-forming compensation.
Each correction loop may require smaller, more precise adjustments because the relationship between die geometry and part geometry is less predictable.
Stainless steel 304 work-hardens during forming, which means the forming surfaces must be tuned more carefully — over-correction in one area can create cracking in adjacent zones.
Sheet thickness matters as well.
Thin sheets (below 1.0 mm) are less forgiving of dimensional errors in the die because the material has less stiffness to resist minor variations in forming pressure.
Thick sheets (above 3.0 mm) require higher tonnage, which amplifies the effect of any misalignment in the die or press.
Material batch variation is another factor that is rarely discussed but practically significant.
Even within the same alloy specification, different coils can have slightly different yield strength and elongation properties.
A die that is validated on one material batch may need minor adjustments when the production material comes from a different supplier or heat number.
Experienced toolmakers account for this by running tryout with material from the same batch intended for production.
Prototypen-Werkzeugprobebetrieb vs. Produktions-Werkzeugprobebetrieb
Prototype and production tooling serve different purposes, and their tryout processes have different targets, different tolerances, and different risk profiles.
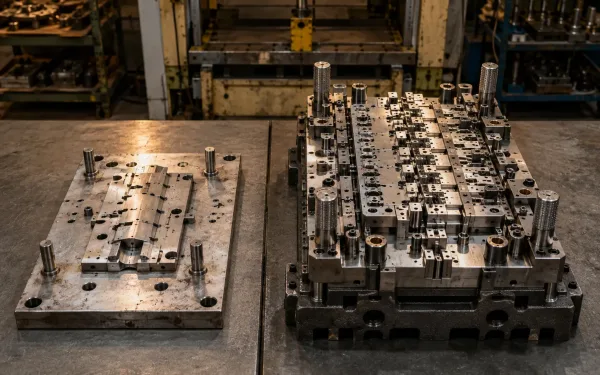
Left: a prototype die made from softer tool steel with simplified geometry, designed for part design validation with wider tolerances. Right: a production die built from hardened D2 tool steel with precision-ground forming surfaces, designed for hundreds of thousands of parts at tight tolerances.
A prototype die is built to validate part design and fit — not to prove long-term production capability.
Prototype tryout tolerances are typically 1.5 to 2 times wider than production tolerances.
The number of correction loops is lower (one to three), and the focus is on form and function rather than process stability.
The die may use softer tooling materials or simplified geometry to reduce lead time and cost.
A production die is built for volume.
Its tryout must prove that the die can produce hundreds of thousands of parts without dimensional drift, surface degradation, or unplanned downtime.
Production tryout requires tighter tolerances, more correction loops, and a formal validation protocol.
The die tooling is typically made from hardened tool steel (such as D2 or DC53), and the tryout must verify that cutting edges and forming surfaces maintain quality over extended runs.
The confusion between these two is a common source of problems.
A buyer who expects production-level consistency from a prototype die will be disappointed.
A buyer who accepts prototype-level validation for a production die is accepting risk that will surface during mass production.
Wann ist der Probebetrieb “abgeschlossen” — Abnahmekriterien
Tryout is complete when the die produces parts that meet all of the following conditions:
- Dimensional conformance: All critical dimensions are within tolerance on a defined number of consecutive parts (typically 5 to 30, depending on project requirements).
- Surface quality: No visible defects (cracks, deep scratches, severe wrinkling, excessive burr) on production-intent surfaces.
- Wiederholbarkeit: Part-to-part variation is within an acceptable range — usually specified as a percentage of the total tolerance band.
- Process stability: The die runs at target production speed without abnormal tonnage spikes, strip feeding issues, or part transfer failures.
- Tooling condition: After the validation run, the die shows no signs of abnormal wear, galling, or damage.
If the die meets these conditions, the toolmaker documents the tryout results, records the final press settings, and submits samples for customer approval.
If it does not meet them, the correction loop continues.
Wichtige Erkenntnisse
Die tryout is not a formality at the end of the tooling timeline — it is the phase where the die, the process, and the part are validated together under real production conditions.
The number and quality of correction loops during tryout directly determine how smoothly the die transitions into mass production.
Material choice, sheet thickness, and the distinction between prototype and production tooling all affect how long tryout takes and what “done” actually means.
For buyers, the most important question to ask a toolmaker is not “how fast can you finish tryout?” but “how do you run your correction loops, and what criteria do you use to decide the die is ready?”