AKlebebindung hat sich zu einer gängigen Fügemethode für Blechbaugruppen in der Automobil-, Elektronik-, Haushaltsgeräte- und Industriegehäuseindustrie entwickelt. Sie verteilt Spannungen gleichmäßig, erzeugt keine wärmebeeinflusste Zone und kann verschiedene Metalle verbinden. Diese Vorteile machen die Klebebindung zu einer wichtigen Blechmontagemethode und zu einer Alternative zum Punktschweißen und mechanischen Befestigen.
Die meisten Leitfäden beantworten jedoch nur, ob ein Teil geklebt werden kann. Sie gehen selten auf die Frage ein, die für Produktionseinkäufer und Ingenieure am wichtigsten ist:
Kann der Prozess die Hochvolumenproduktion unterstützen?
Die Antwort hängt weniger vom Klebstoff selbst ab, als viele annehmen. Die Produktionskapazität wird hauptsächlich durch drei Fertigungsfaktoren bestimmt:
- Aushärtungszyklus
- Dosierkonsistenz
- Vorrichtungswechsel
Dieser Artikel untersucht jeden Faktor, um Ihnen zu helfen, festzustellen, ob Klebebindung für Hochvolumen-Blechaufträge geeignet ist.
Was begrenzt die Klebebindungskapazität in der Blechproduktion?
In der Prototypen- oder Kleinserienproduktion ist die Klebebindung relativ einfach: Klebstoff auftragen, Teile spannen und auf die Aushärtung warten.
In der Hochvolumenproduktion kann jedoch jeder Schritt die Kapazität begrenzen.
Der tatsächliche Fertigungsprozessablauf für jedes Teil besteht aus vier Schritten:
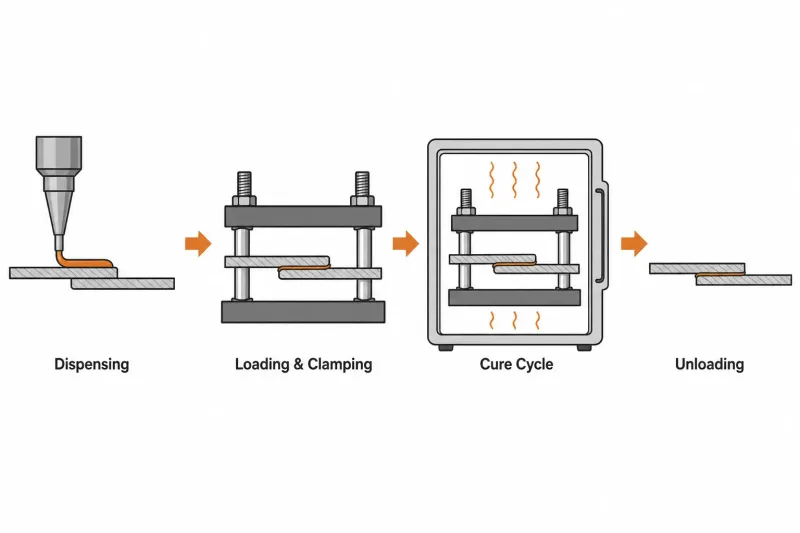
Die vier sequenziellen Schritte eines Klebebindungs-Produktionszyklus. Jedes Blechteil durchläuft Dosieren, Spannen, Aushärten und Entladen — der langsamste Schritt bestimmt die Gesamtlinienkapazität.
- Dosierzeit — die Zeit, die zum Auftragen von Klebstoff auf die Bindungsfläche erforderlich ist
- Ladezeit — die Zeit, die zum Positionieren und Spannen der Teile in der Vorrichtung erforderlich ist
- Aushärtungszeit — die Zeit, die der Klebstoff benötigt, um Handfestigkeit zu erreichen
- Entladezeit — die Zeit, die zum Entfernen der geklebten Baugruppe aus der Vorrichtung erforderlich ist
Der langsamste Schritt bestimmt die Kapazität der gesamten Produktionslinie.
Bei den meisten Blechbindungsprozessen ist die Aushärtungszeit der Hauptengpass. Es kann auch einen erheblichen Unterschied zwischen der im technischen Datenblatt des Lieferanten angegebenen Aushärtungszeit und dem tatsächlichen Produktionszyklus geben.
Deshalb kann ein Klebebindungsprozess, der in einer Prototypenwerkstatt gut funktioniert, zu einer ernsthaften Einschränkung werden, wenn die Produktion auf Tausende von Teilen erhöht wird.
Aushärtungszyklus — Ein oft übersehener Kapazitätsengpass
Die Aushärtungszeit ist der größte Faktor, der die Klebebindungskapazität beeinflusst. Die Aushärtungsmethode bestimmt, ob der Prozess mit dem Gesamtproduktionsplan Schritt halten kann.
Raumtemperatur-Aushärtung
Raumtemperaturhärtende Klebstoffe benötigen normalerweise 4–72 Stunden, um die volle Strukturfestigkeit zu erreichen.
Diese Methode ist für die Offline-Montage in kleinen Stückzahlen geeignet, jedoch nicht für Produktionslinien, die wöchentlich Tausende von Teilen versenden müssen.
Wärmehärtung
Wärmehärtende Klebstoffe werden üblicherweise in der Hochvolumenproduktion verwendet.
Bei Temperaturen von 120°C–180°C erreichen die meisten Strukturklebstoffe innerhalb von 15–30 Minuten Handfestigkeit, wodurch der Bindungszyklus näher an das Schweißen oder die mechanische Befestigung heranrückt.
Die Aushärtungsausrüstung beeinflusst auch die Produktionseffizienz:
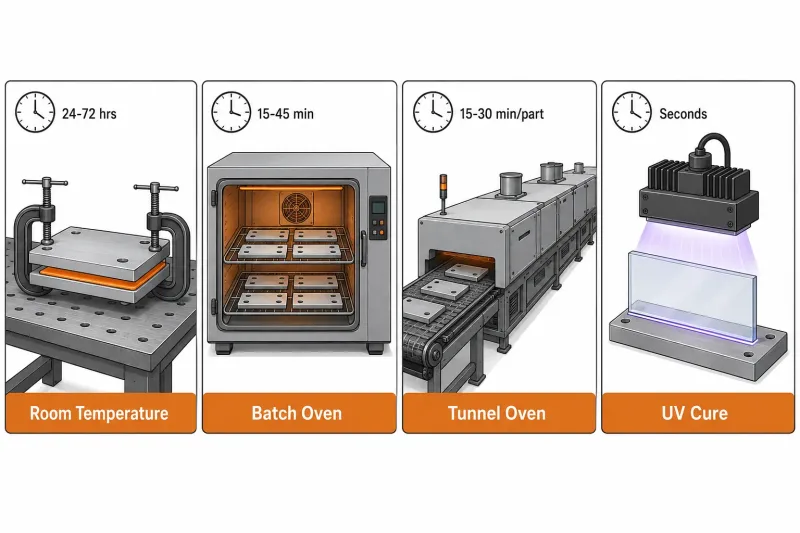
Vier Aushärtungsmethoden im Vergleich nach Zykluszeit und Produktionsumfang. Für Hochvolumenaufträge sind in der Regel Batch- oder Durchlauföfen erforderlich, um die Produktionspläne einzuhalten.
| Aushärtungsmethode | Typischer Zyklus | Geeignet für | Einschränkung |
|---|---|---|---|
| Raumtemperatur-Aushärtung | 4–72 Stunden | Prototypen, Reparaturen und Kleinserienproduktion | Kann Hochvolumenproduktionspläne nicht einhalten |
| Batch oven | 15–45 minutes per batch | Medium-volume production (500–2,000 parts/day) | Batch loading and unloading reduce flexibility |
| Continuous tunnel oven | 15–30 minutes per part | High-volume production (over 2,000 parts/day) | Higher equipment investment |
| UV curing for thin bond lines | Seconds | Transparent materials or very thin substrates | Limited to specific adhesive types and part geometries |
For most high-volume sheet metal projects, heat curing in a dedicated oven is a basic requirement, not an optional equipment upgrade.
Adhesive Bonding vs. Welding in High-Volume Production
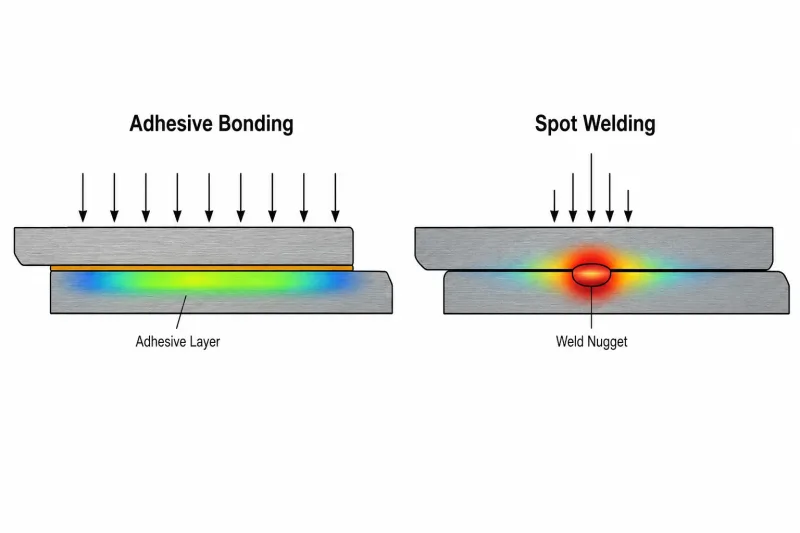
Cross-section comparison showing how adhesive bonding distributes stress across the entire bond area, while spot welding concentrates stress at individual weld points — a key factor in joint design decisions.
When comparing adhesive bonding with Blechschweißen, the real question is not which process is better, but:
At what production volume does each process make more sense?
The table below compares the two processes across key production factors:
| Faktor | Adhesive Bonding | Punktschweißen |
|---|---|---|
| Equipment investment | Fixtures and curing oven | Spot welder and electrodes |
| Unit cost at high volume | Lower; no skilled welder is required at every station | Higher, including labor and electrode wear |
| Production cycle | Depends on the curing method; heat curing usually takes 15–30 minutes | Very fast per weld, usually 2–5 seconds |
| Stress distribution | Evenly distributed across the bonded area | Concentrated at the weld points |
| Joint design | Best suited to lap joints | Suitable for lap joints and some T-joints |
| Dissimilar metals | Suitable for aluminum-to-steel and coated-metal joints | More difficult due to galvanic corrosion and metallurgical issues |
| In-line quality inspection | More difficult because the bond line is usually hidden | Easier because the weld nugget can be inspected or measured |
| Distortion risk | No heat input and little risk of distortion | Thin sheet metal is more likely to distort |
| Minimum practical volume | About 500–1,000 parts to justify fixture investment | Suitable for any volume |
Adhesive bonding begins to show a cost advantage when order volume can justify the fixture investment and the joint has sufficient overlap.
- Below 500 parts: Welding is usually easier to implement and faster to launch.
- Above 1,000 parts: The unit-cost advantage of adhesive bonding gradually increases.
This advantage becomes more significant when reduced distortion, the elimination of post-weld grinding, and the prevention of galvanic corrosion between dissimilar metals are also considered.
Surface Preparation for Scaled Production
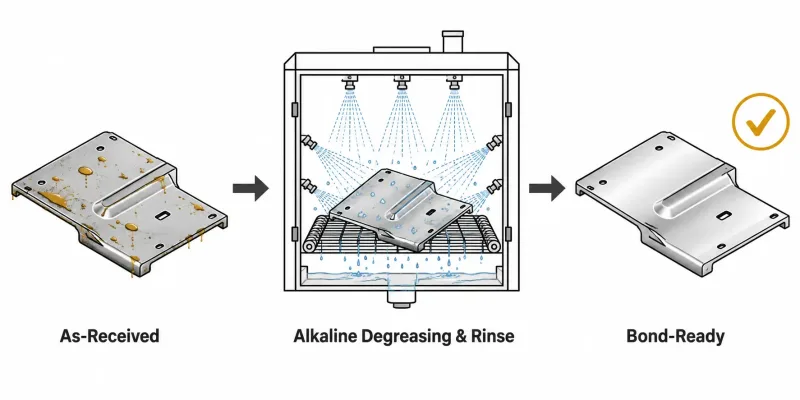
The surface preparation workflow for high-volume adhesive bonding: incoming parts with stamping oil undergo alkaline degreasing and rinsing before arriving at the bonding station clean and ready for adhesive application.
Surface preparation is one of the most common failure points in high-volume adhesive bonding.
When sheet metal parts arrive at the bonding station, their surfaces may contain:
- Stamping oil
- Drawing oil
- Rust-preventive oil
These contaminants are among the most common causes of adhesive bond failure, but they are easily overlooked during design reviews.
In low-volume production, operators can wipe each part with a solvent.
In high-volume production, however, surface preparation must be integrated into the production process. The three common methods are:
In-Line Degreasing
A spray washer or immersion cleaning system is installed before the bonding station.
This is the most common method for steel and aluminum sheet metal parts. The parts pass through alkaline cleaning, rinsing, and drying before entering the bonding station.
Offline Solvent Wiping
Parts are wiped manually or automatically using acetone or isopropyl alcohol.
This method is simple but labor-intensive. Consistency depends on operator technique, making it difficult to achieve the same result across thousands of parts.
Plasma or Corona Treatment
This method activates the metal surface at the molecular level and improves adhesive wetting.
It is particularly suitable for aluminum and stainless steel because their natural oxide layers may affect bonding performance. Although it requires additional equipment investment, it can significantly improve bond reliability.
Surface Preparation for Different Metals
The correct method depends on the base material.
Low-carbon steel has moderate surface energy and usually bonds well after degreasing alone.
Aluminum and stainless steel generally require additional surface activation, such as plasma treatment or chemical primers, because their surface oxide layers affect adhesive wetting.
In practice, most high-volume sheet metal bonding lines use a degreasing and primer combination.
Although this adds another process step, it improves consistency across different shifts and operators.
Fixture Design and Production Efficiency
Fixture design is often underestimated when adhesive bonding is scaled from prototyping to mass production.
Fixtures remain occupied during adhesive curing and cannot be reused until the bonded assembly is removed.
This creates a direct relationship between:
- Aushärtungszeit
- Number of fixtures
- Production efficiency
The calculation is straightforward:
If the cure time is 20 minutes and each fixture holds one assembly, one fixture can produce only three parts per hour. To produce 60 parts per hour, 20 fixtures are required.
Fixture investment is a real cost and must be included in the project cost calculation.
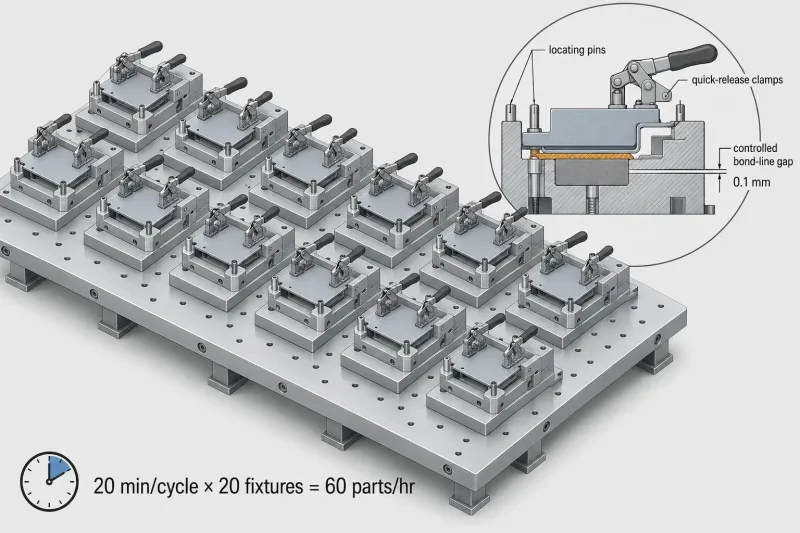
When curing time is 20 minutes per part, producing 60 assemblies per hour requires 20 fixtures operating in parallel. The inset shows key fixture features: locating pins, quick-release clamps, and controlled bond-line thickness.
The main factors to consider when designing production fixtures include:
- Loading and unloading speed — quick-release clamps and locating pins reduce auxiliary production time outside the curing cycle
- Fixture material — aluminum fixtures heat and cool faster in curing ovens but wear more quickly; steel fixtures are more durable but have greater thermal mass
- Clamping force — excessive force squeezes out the adhesive and creates an insufficient bond line; insufficient force leaves gaps and voids
- Tolerance control — fixtures must maintain consistent bond-line thickness across all positions, usually within 0.05–0.2 mm
For very high production volumes, multi-station fixtures can bond 4, 8, or 16 assemblies per cycle, reducing the fixture cost allocated to each part.
However, this also increases the complexity of adhesive dispensing and quality inspection.
Quality Control for High-Volume Bonded Assemblies
Quality control for bonded assemblies is fundamentally different from quality control for welded assemblies.
Spot welds can be inspected visually or with simple gauges. Adhesive bond lines are hidden inside the joint, and many failure modes cannot be found without destructive testing.
A structured inspection plan for high-volume production usually uses several layers of control:
Full First-Article Inspection
The first bonded product from each shift or batch is subjected to a destructive peel or tensile test to confirm that the process is under control.
Periodic Destructive Sampling
One sample is tested to failure every 50 or 100 parts, and the failure mode is recorded.
- Cohesive failure: The adhesive tears within itself, indicating good bond quality.
- Adhesive interface failure: The adhesive separates completely from the metal surface, indicating a surface-preparation problem.
In-Process Monitoring
The following parameters should be continuously recorded:
- Dispensing pressure
- Adhesive bead width
- Oven temperature profile
Sichtprüfung
Inspect for:
- Adhesive squeeze-out on visible surfaces
- Uneven bond lines
- Air bubbles along the edges of the bond line
Common Adhesive Bonding Defects
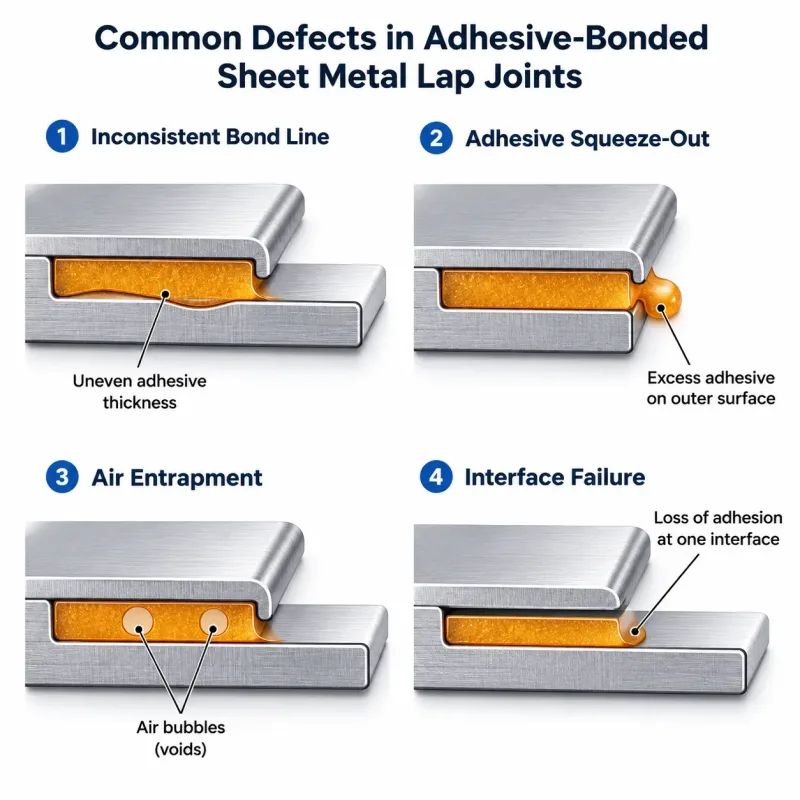
Four typical defects in high-volume adhesive bonding shown in cross-section. Identifying these failure modes early — through first-article testing and periodic sampling — is essential for maintaining consistent bond quality.
The most common defects in high-volume sheet metal bonding include:
- Inconsistent bond-line thickness — usually caused by fixture wear or inconsistent part dimensions
- Adhesive squeeze-out — adhesive appears on cosmetic surfaces, usually because of excessive clamping force or excessive adhesive
- Air entrapment — trapped air creates voids and reduces bond strength, usually because the adhesive is applied as a continuous bead rather than an intermittent pattern
- Interface failure — the adhesive separates completely from the metal surface, almost always because of inadequate surface preparation
Is Adhesive Bonding Suitable for Your Order Volume?
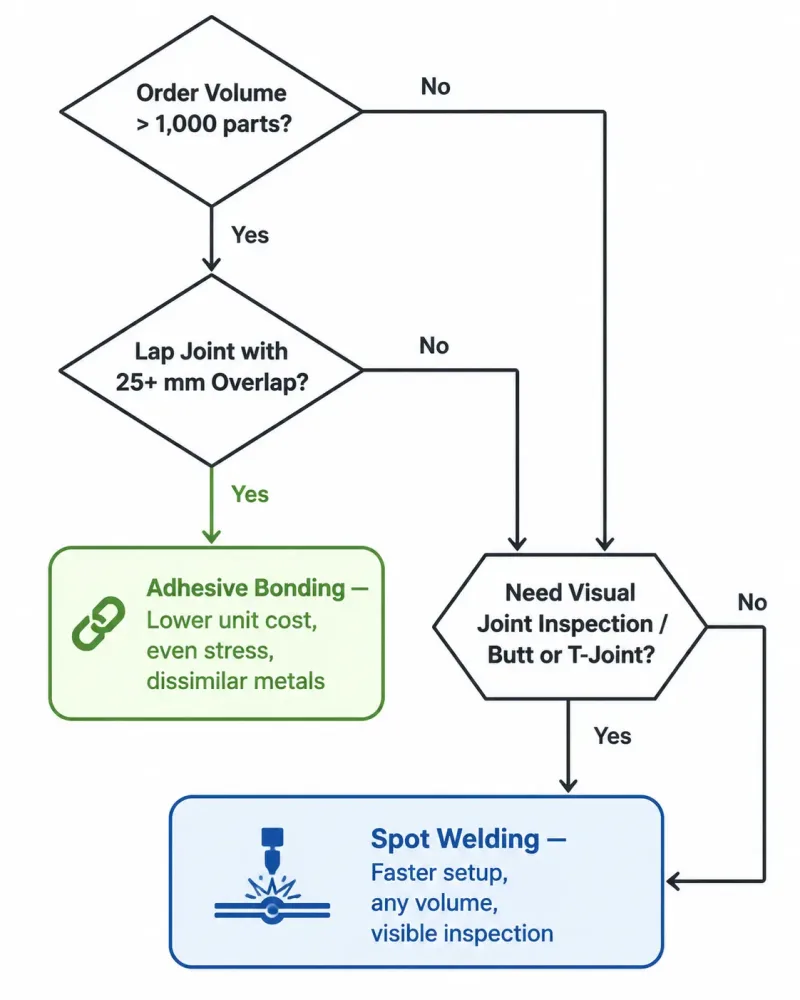
A simplified decision guide for selecting between adhesive bonding and spot welding. The key factors are order volume, joint geometry, and whether in-process visual inspection is required.
Adhesive bonding is not always better or worse than welding or mechanical fastening.
Its suitability depends on a combination of:
- Production strategy and order volume
- Joint design
- Supplier production capacity
The following conditions can help you decide.
Adhesive Bonding Is Suitable When
- Order volume exceeds 500–1,000 parts, enough to justify fixture and oven investment
- The joint uses a lap design with at least 25 mm of overlap
- Different metals must be joined, such as aluminum to steel or coated to uncoated metal
- Cosmetic appearance is important and weld marks or heat distortion are unacceptable
- The part requires structural joining and sealing in the same operation
- The sheet metal is no thicker than 1.5 mm, and welding may cause burn-through or warping
Welding Is Still More Suitable When
- The joint must withstand high peel loads or dynamic fatigue loads
- The assembly uses butt joints or T-joints unsuitable for adhesive bonding
- Order volume is too low to justify fixture and curing equipment costs
- In-process visual inspection of the joint is required
- Production frequently changes between different part numbers
If the supplier has heat-curing capacity and the parts use lap joints suitable for bonding, adhesive bonding can provide stable quality in Sie findet statt, bevor die Fabrik von der Prototypen- oder Pilotproduktion auf while achieving a lower unit cost than welding once the production line is established.
Next Steps for a High-Volume Adhesive Bonding Project
If you are evaluating adhesive bonding for a high-volume sheet metal order, begin with the following steps:
- Confirm joint design suitability
Confirm that the overlap is at least 25 mm and that the bond-line gap can be controlled within 0.05–0.2 mm. - Discuss the curing method with the supplier
Confirm the supplier’s heat-curing capacity through an equipment review or Werksbesichtigung, and determine the actual production cycle. - Request a production process control plan
The plan should include first-article inspection standards, sampling frequency, and defect definitions. - Run a pilot batch
Use rapid sheet metal prototyping to produce an initial batch of 50–100 parts and verify process repeatability before starting full-scale production.
SR-MFG works with engineering and procurement teams to plan adhesive bonding processes for high-volume sheet metal orders, including joint design reviews and production ramp-up.
If you are evaluating adhesive bonding for your next project, contact our team to discuss your order volume and production schedule.