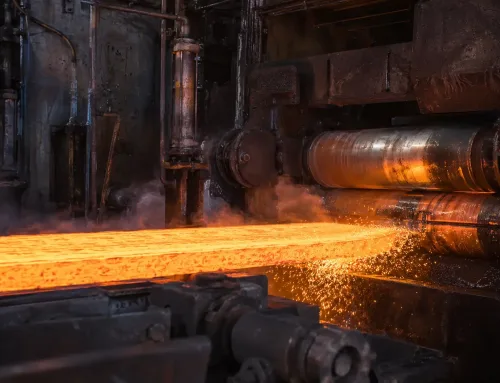
The same steel can perform very differently depending on how it is heat treated. Annealing softens it, quenching increases hardness, tempering improves toughness, and carburizing strengthens the surface. With so many processes involved, it is easy to mix them up.
SR MFG hat eine praktische Referenztabelle zusammengestellt, die die wichtigsten Punkte von Glühen, Normalglühen, Härten, Anlassen, Vergüten, Auslagern, thermochemischer Behandlung und Brünieren abdeckt. Sie fasst übersichtlich zusammen, wie jedes Verfahren funktioniert, welches Ziel es verfolgt und was Konstrukteure bei der Festlegung von Wärmebehandlungshinweisen in Fertigungszeichnungen.
Horizontal wischen, um die vollständige Tabelle anzuzeigen →
| Behandlung | Wärmebehandlungsverfahren | Zweck |
|---|---|---|
| Glühen | Das Stahlteil auf eine festgelegte Temperatur erwärmen, für einen bestimmten Zeitraum halten und dann langsam auf Raumtemperatur abkühlen lassen. |
|
| (1) Vollglühen | Das Stahlteil auf 30–50 °C über der kritischen Temperatur erwärmen. 710–750 °C, und kann bei bestimmten legierten Stählen 800–900 °C erreichen. | Die Kornstruktur verfeinern, das Gefüge homogenisieren, die Härte reduzieren und innere Spannungen vollständig abbauen. 0.8%, sowie für entsprechende Schmiedeteile und Stahlgussteile. |
| (2) Kugelglühen | Das Stahlteil auf 20–30 °C über der kritischen Temperatur, 500 °C abkühlen, bevor es aus dem Ofen entnommen und an Luft abgekühlt wird. | Härte reduzieren und Zerspanbarkeit verbessern sowie das Material für das nachfolgende Härten vorbereiten. 0.8%. |
| (3) Spannungsarmglühen | Das Stahlteil auf 500–650 °C,. | Innere Spannungen abbauen, die durch Schmieden, Kaltrichten und Zerspanung entstehen,. |
| Normalglühen | Das Stahlteil auf 40–60 °C über der kritischen Temperatur,. |
|
| Härten | Das Stahlteil auf die Härtetemperatur erwärmen, für einen bestimmten Zeitraum halten. |
|
| (1) Einschicht-Härten | Das Stahlteil auf die Härtetemperatur erwärmen, auf Temperatur halten 5–8 mm, wird Sole oder Wasser zum Härten verwendet,. | |
| (2) Zweischicht-Härten | Das Stahlteil auf die Härtetemperatur erwärmen und auf Temperatur halten. 300–400 °C,abkühlen,. | |
| (3) Flammhärten | Use an oxy-acetylene flame to rapidly heat the surface of the part to the quenching temperature, then immediately spray the heated surface with water. Flame hardening is suitable for single-piece or small-batch production of large medium-carbon steel and medium-carbon alloy-steel components that require a hard, wear-resistant surface while also withstanding impact loads, such as crankshafts, gears, and guideways. | |
| (4) Induction Hardening | Place the steel part inside an induction coil. An alternating current of a specified frequency generates a magnetic field, which induces electrical current in the steel part and rapidly heats its surface to the quenching temperature within approximately 2–10 min. The surface is then immediately water-quenched. After induction hardening, the surface becomes hard and wear-resistant while the core retains good strength and toughness. This process is suitable for medium-carbon steels and medium-alloy steels. | |
| 4. Tempering | Heat the quenched steel part to a temperature below the critical temperature, hold it for a specified period, and then cool it in air or oil. Tempering is normally carried out immediately after quenching and is generally the final stage of heat treatment. |
|
| (1) Low-Temperature Tempering | Heat the hardened steel part to 150–50°C, hold it at this temperature for a specified period, and then cool it in air. Low-temperature tempering is commonly used for cutting tools, measuring tools, dies and molds, rolling bearings, and carburized parts. | Relieve internal stresses generated during quenching. |
| (1) Medium-Temperature Tempering | Heat the quenched steel part to 350–450°C, hold it for a specified period, and then allow it to cool. This process is commonly used for various types of springs and hot-work dies. | Provide the steel with high elasticity together with a suitable combination of toughness and hardness. |
| (1) High-Temperature Tempering | Heat the quenched steel part to 500–650 °C, hold it at temperature, and then cool it. This process is mainly used for critical structural parts requiring both high strength and high toughness, such as spindles, crankshafts, cams, gears, and connecting rods. | Provide a good overall combination of mechanical properties, including high strength, good toughness, and sufficient hardness, while relieving internal stresses caused by quenching. |
| 5. Quenching and Tempering (Q&T) | After quenching, temper the steel part at a high temperature of 500–600°C. This treatment is commonly used for important structural components such as shafts, gears, and connecting rods, and is generally carried out after rough machining. | Refine the grain structure and provide the steel with high toughness and sufficient strength, resulting in a well-balanced combination of mechanical properties. |
| 6. Aging Treatment — (1) Artificial Aging | Heat the quenched steel part to 100–160°C, hold it at temperature for an extended period, and then allow it to cool. | Relieve internal stresses, minimize distortion, and stabilize dimensions. This treatment is particularly important for precision components. |
| (2) Natural Aging | Place castings outdoors. Parts such as long shafts and lead screws may be placed in seawater, suspended for an extended period, or lightly tapped. Parts requiring natural aging should preferably undergo rough machining beforehand. | |
| 7. Thermochemical Treatment | Place the steel part in a chemical medium containing active elements such as carbon, nitrogen, or chromium. Through heating, holding, and cooling, these elements diffuse into the surface layer of the steel, changing its surface chemical composition and giving the surface specific properties. | |
| (1) Carburizing | Introduce carbon atoms into the surface layer of the steel part. Commonly used for wear-resistant parts subjected to impact loads, such as wheels, gears, shafts, and piston pins. | Provide the surface with high hardness of approximately HRC 60–65 and excellent wear resistance, while maintaining high toughness in the core. |
| (2) Nitriding | Introduce nitrogen atoms into the surface layer of the steel part. Commonly used for important components such as bolts, nuts, and pins. | Improve surface hardness, wear resistance, and corrosion resistance. |
| (3) Cyaniding | Introduce both carbon and nitrogen atoms into the surface layer of the steel part. Suitable for low-carbon steels, medium-carbon steels, alloy steels, and certain high-speed steel cutting tools. | Improve surface hardness and wear resistance. |
| 8. Black Oxide Treatment | Immerse the metal parts in a highly concentrated alkaline oxidizing solution and heat them to form a magnetite (Fe₃O₄) film on the surface. This treatment is commonly used for low-carbon steels and low-carbon alloy tool steels. Depending on the material and process conditions, the oxide layer may appear blue-black, black, reddish-brown, or brownish-black, with a typical thickness of 0.6–0.8 μm. | Provide corrosion protection, improve the appearance and surface luster of the metal, and relieve stresses generated during quenching. |