YSie haben ein Angebot für ein Kleinserienprojekt im Blechbereich erhalten. Der Stückpreis erscheint angemessen, aber die NRE-Positionen sind vage—in einer einzigen Zahl zusammengefasst, ohne Aufschlüsselung. Sie sind sich nicht sicher, welche Kosten standard sind, welche verhandelbar sind und welche später als Überraschungskosten auftauchen könnten.
Dies ist eine häufige Situation für Ingenieure und Beschaffungsteams, die 50 bis 500 Blechteile bestellen. Bei diesem Volumen, können nicht wiederkehrende Engineering-Kosten (NRE) einen erheblichen Anteil am Gesamtprojektbudget ausmachen—manchmal übersteigen sie die Stückkosten für die gesamte Serie. Anders als bei der Großserienproduktion, bei der Werkzeugkosten über Tausende von Teilen amortisiert werden, erfordern Kleinserienprojekte eine sorgfältigere Prüfung jeder NRE-Position, bevor Sie genehmigen.
Diese Checkliste führt Sie durch sechs Schritte zur Überprüfung von Werkzeug- und NRE-Kosten bei jedem Kleinserien-Blechangebot. Verwenden Sie sie, bevor Sie unterschreiben, und Sie werden Probleme erkennen, die sonst Ihr Projekt um Wochen verzögern oder Ihr Budget um Tausende aufblähen könnten.
Warum Kleinserienprojekte einen anderen NRE-Ansatz erfordern
In der Großserienproduktion im Blechbereich—1.000 Teile und mehr—werden NRE-Kosten auf eine große Basis verteilt. Ein $5.000 Folgeverbundwerkzeug fügt bei 10.000 Einheiten nur $0,50 pro Teil hinzu. Die Rechnung geht auf.
Bei 50 bis 500 Teilen ändert sich die Rechnung vollständig. Dasselbe $5.000 Werkzeug fügt nun $10 bis $100 pro Teil hinzu. Bei vielen Projekten, können die NRE allein die gesamten Teilekosten übersteigen. Deshalb erfordert die Kleinserien-Blechfertigung eine andere Werkzeugstrategie: Soft-Tooling, geteiltes Tooling und in manchen Fällen gar kein kundenspezifisches Tooling.
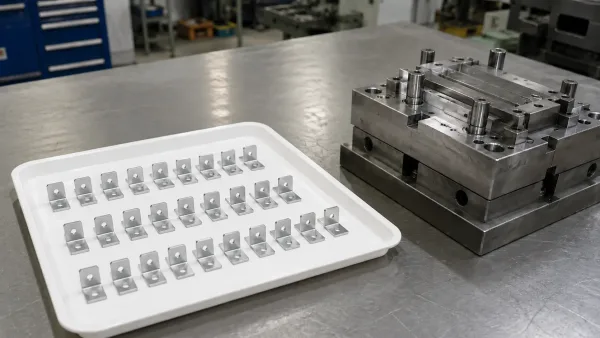
Eine kleine Produktionsserie von Blechhalterungen neben dem zum Stanzen erforderlichen Stanzwerkzeug — veranschaulicht, warum die NRE pro Teil bei kleinen Stückzahlen hoch ist.
Die Herausforderung besteht darin, dass viele Angebote diese Unterscheidung nicht klar machen. Ein Lieferant kann kundenspezifisches Tooling für eine 100-Teile-Serie anbieten, obwohl Soft-Tooling oder Standard-Tooling genauso gut funktionieren würden. Oder er versteckt Rüstkosten, Programmierkosten und Vorrichtungskosten in einer vagen “NRE”-Position. Ohne eine strukturierte Überprüfung wissen Sie nicht, wofür Sie bezahlen—oder ob Sie zu viel bezahlen.
Diese Checkliste ist für dieses Szenario konzipiert. Sie ist kein allgemeiner DFM-Leitfaden. Sie ist ein Schritt-für-Schritt-Prüfrahmen speziell für die Werkzeug- und NRE-Positionen in einem Kleinserien-Blechangebot.
Schritt 1 — Werkzeugaufschlüsselung prüfen
Werkzeugbau ist in der Regel die größte einzelne NRE-Position in einem Blechangebot. Bevor Sie die Zahl bewerten, müssen Sie verstehen, was sie umfasst.
Was als Werkzeug in einem Blechangebot zählt
In der Blechfertigung kann sich “Werkzeug” auf verschiedene Positionen beziehen:
- Stanzwerkzeuge — kundenspezifisch geschnittene Werkzeuge zum Stanzen, Umformen oder Lochen. Werden eingesetzt, wenn Teile eine konsistente, wiederholbare Umformung in Serie erfordern.
- Biegewerkzeuge — kundenspezifische Stempel- und Matrizensätze für Gesenkbiegen. Standard-V-Matrizen-Sätze decken die meisten Biegeradien und Winkel ab, aber enge Biegeradien oder ungewöhnliche Profile können kundenspezifische Sätze erfordern.
- Vorrichtungs- und Spannkosten — Werkstückhaltevorrichtungen, die beim Schweißen, Montieren oder bei Sekundäroperationen verwendet werden. Jede einzigartige Teilegeometrie kann eine dedizierte Vorrichtung erfordern.
- Laser- oder Stanzprogrammierung — die Kosten für die Programmierung von CNC-Laserschneidern oder Revolverstanzen für Ihre Teilegeometrie. Dies sind einmalige Rüstkosten.
Bitten Sie Ihren Lieferanten, jede Werkzeugposition separat aufzulisten. Eine einzelne “Werkzeug”-Position, die all dies zusammenfasst, macht es unmöglich zu bewerten, was wesentlich und was optional ist.
Standard vs. Soft vs. Custom Tooling
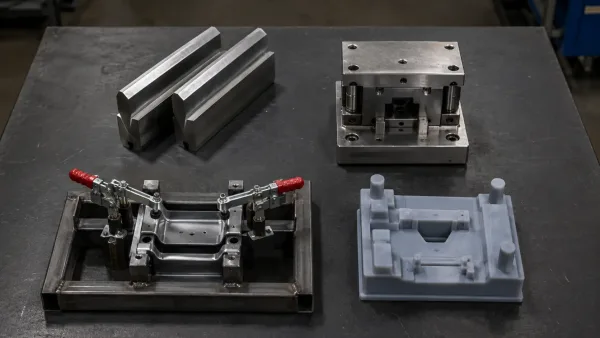
Four common tooling types in sheet metal fabrication: standard V-dies, a custom stamping die, a welding fixture, and a 3D-printed soft tooling die.
Not all tooling is created equal. For low-volume projects, the type of tooling has a direct impact on NRE:
| Tooling Type | Typical NRE Range | Am besten geeignet für | Einschränkungen |
|---|---|---|---|
| Standard tooling | $0–$500 | Parts that use common bend radii, standard hole sizes, and no custom forming | Limited to geometries that match existing tool sets |
| Soft tooling (temporary or 3D-printed dies) | $500–$3,000 | Prototype runs, 50–200 parts, geometries that do not require tight tolerances | Shorter lifespan, less consistent across large runs |
| Sonderwerkzeuge (hardened steel dies) | $3,000–$20,000+ | Production runs of 500+, parts with tight tolerances or complex forming | High upfront cost, long lead time (4–8 weeks) |
For a 100-part run, standard or soft tooling is almost always the right choice. If your vendor is quoting custom tooling for a low-volume order, ask why—and whether a softer alternative would work.
What to Ask Your Vendor
- Is this tooling reusable for future orders, or is it project-specific?
- What is the tooling lifespan (number of hits or cycles)?
- Can you offer soft tooling or standard tooling as an alternative?
- Is there an amortization plan if I increase the order quantity later?
Schritt 2 — Versteckte NRE-Positionen identifizieren
Tooling is visible. Many NRE charges are not. Low-volume sheet metal quotes often include setup and engineering fees that are easy to overlook—and easy to contest.
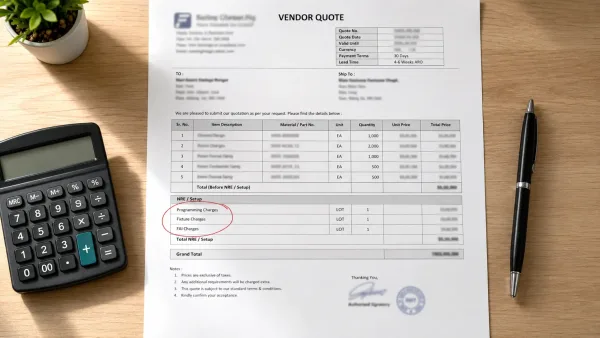
A vendor quote with NRE and setup line items circled — identifying hidden charges that are easy to overlook during quote review.
Common Hidden NRE Charges
The following items frequently appear in sheet metal quotes but are not always labeled clearly:
- CNC programming — the cost to generate laser or punch programs from your CAD files. Typically $100–$500 per part number.
- Erstmusterprüfung (FAI) — the cost to produce and inspect the first part against your drawing specifications. Common in aerospace and medical projects. $200–$800 per part.
- Fixture design and fabrication — custom workholding for welding, bending, or assembly. $300–$2,000 per fixture.
- Surface treatment setup — plating, powder coating, or anodizing lines often require a “setup charge” or “minimum lot charge” for small batches. $150–$600 per batch.
- Packaging design — custom packaging for fragile or precision parts. $100–$400.
- Material sourcing surcharge — if your specified material is not in the vendor’s standard inventory, they may charge a sourcing premium for small-quantity purchases.
Which Charges Are Negotiable, Which Are Fixed
Not all NRE charges carry the same flexibility:
| Charge Type | Negotiable? | Hinweise |
|---|---|---|
| CNC programming | Somewhat | Ask if the vendor can reuse programs from similar parts |
| First Article Inspection | Rarely | Often required by spec (AS9102, PPAP); hard to waive |
| Fixture costs | Ja | Ask if a simpler fixture or manual setup is possible for low volume |
| Surface treatment setup | Somewhat | Some vendors waive setup if you batch multiple parts in one lot |
| Packaging design | Ja | Standard packaging often works for non-critical parts |
| Material sourcing surcharge | Ja | Ask if you can supply material directly, or if a standard substitute exists |
Use the checklist below when reviewing your quote. For each NRE line item, confirm whether it is listed, whether it is itemized, and whether your vendor has explained what it covers.
Schritt 3 — Material und Blechdicke auf NRE-Auswirkungen prüfen
Material selection affects more than per-part cost. It directly influences NRE through sourcing complexity, machinability, and tooling requirements.
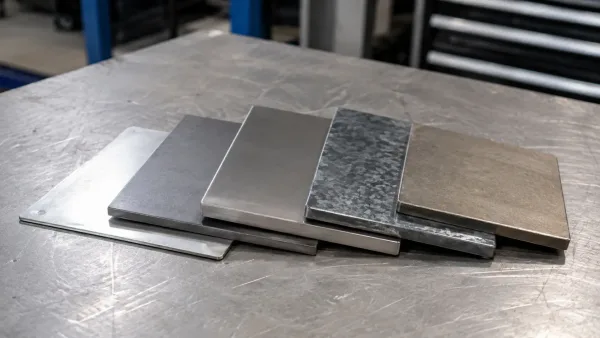
Sheet metal material samples varying in alloy and gauge — material selection directly impacts NRE through sourcing, tooling, and processing requirements.
Standard vs. Non-Standard Materials
Common sheet metal material grades, such as cold-rolled steel (CRS), 304 stainless steel, 5052 aluminum, and galvanized steel, are typically stocked by sheet metal vendors and usually do not add NRE.The vendor already has them in stock, and the tooling is calibrated for their thickness and hardness.
Non-standard materials can increase NRE in several ways:
- Minimum order quantities from mills — if your vendor does not stock Inconel, 17-4 PH stainless, or thick-gauge aluminum (0.25″ and above), they may need to purchase a full mill sheet (4×8 ft or larger) even if you only need a few parts.
- Specialized tooling — harder materials may require coated or carbide tooling, which costs more and wears faster.
- Processing adjustments — materials with high springback (e.g., titanium, high-strength steel) may need iterative forming trials, adding to setup time and cost.
Gauge and Thickness Considerations
Sheet metal gauge and thickness affect both tooling selection and processing:
- Very thin material (26–30 gauge) requires tighter punch-to-die clearances and may need special handling to avoid wrinkling or tearing.
- Very thick material (3/16″ and above) requires higher-tonnage equipment and larger bend radii, which can increase tooling costs.
- Non-standard thicknesses (e.g., 0.090″ aluminum instead of the standard 0.063″ or 0.125″) may require custom V-die sets.
Review Checklist
- Is the specified material in the vendor’s standard inventory?
- If not, what is the minimum purchase quantity, and how is that cost allocated?
- Does the material require specialized tooling or processing adjustments?
- Would a standard material substitute reduce NRE without affecting part function?
Schritt 4 — Designmerkmale bewerten, die NRE erhöhen
Certain design features on your drawing can drive up tooling complexity and NRE—even if the features seem minor. Identifying these before you approve the quote gives you the option to simplify.
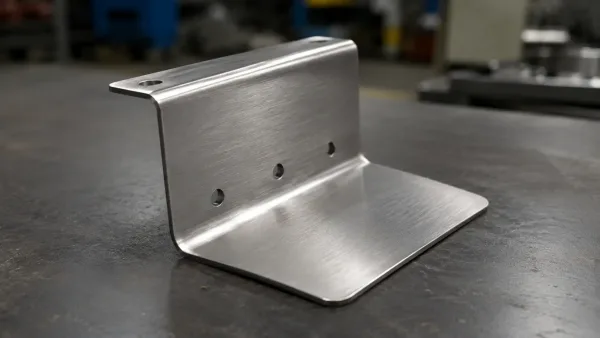
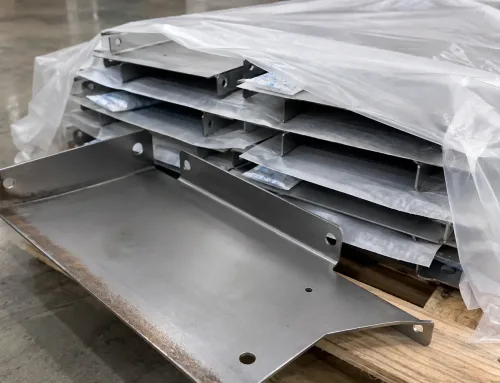
A sheet metal bracket exhibiting design features that drive up NRE — narrow flanges, tight bend radii, and holes positioned close to bend lines.
Design Features That Increase Tooling Complexity
The following features are common NRE drivers in low-volume kundenspezifische Blechfertigung:
- Narrow flanges — flanges shorter than 4× the material thickness require special bend tooling or may not be formable at all.
- Tight bend radii — bend radii smaller than the material thickness increase springback and may need custom punch tooling.
- Deep drawn features — any depth exceeding 2× the material width typically requires progressive forming stages and custom dies.
- Close-tolerance holes near bends — holes positioned within 2× the material thickness of a bend line tend to distort during forming, requiring post-bend reaming or secondary machining.
- Complex external contours — intricate profiles cut by laser add programming time and may require slower cut speeds, increasing per-part cost even if the NRE is fixed.
DFM Adjustments That Reduce NRE Without Changing Function
Many of these features can be simplified with minor design changes:
- Increase flange length to 4× material thickness or more where possible.
- Use standard bend radii (typically 1× material thickness for air bending).
- Move holes at least 2× material thickness away from bend lines.
- Replace deep drawn features with brake-formed channels or welded assemblies.
If you are unsure whether a feature is driving NRE, ask your vendor to flag any design elements that require custom tooling or non-standard processing. A good vendor will identify these during the quoting stage.
Schritt 5 — Dokumentations- und Toleranzanforderungen verifizieren
Incomplete or overly tight documentation is one of the most common—and most avoidable—sources of NRE on low-volume sheet metal projects.
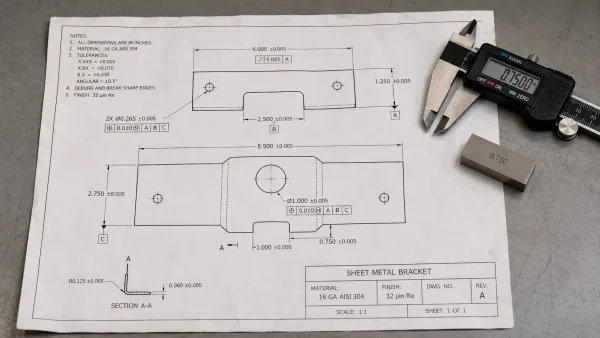
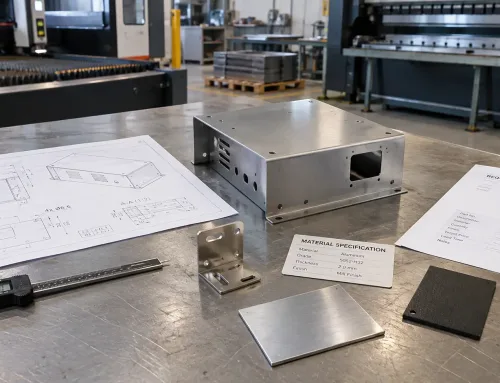
A sheet metal engineering drawing with GD&T callouts and tolerance specifications — incomplete or overly tight tolerances are a common source of avoidable NRE.
How Tolerances Affect NRE
Standard sheet metal tolerances (±0.010″ to ±0.020″ for most features) can be held with standard tooling and process control. Tighter tolerances—±0.005″ or below—increase NRE in several ways:
- Additional fixturing — to hold tight tolerances during forming or welding, dedicated fixtures may be required.
- Secondary machining — features that cannot be held to tolerance on the brake or laser may need post-process milling or grinding.
- Increased inspection — tight tolerances often require 100% inspection rather than sampling, adding labor cost.
If your drawing specifies tight tolerances on non-critical features, consider relaxing them to standard tolerances. This alone can reduce NRE by hundreds of dollars.
Documentation Completeness Checklist
Before your vendor begins production, confirm that the following are clearly defined on your drawing or in your purchase order:
- Drawing revision level — ensure the vendor is quoting to the correct revision.
- Materialspezifikation — alloy, temper, and gauge must be explicitly stated (e.g., “5052-H32, 0.063″”).
- Anforderungen an die Oberflächenbeschaffenheit — specify Ra value or finish type (e.g., “mill finish,” “brushed,” “powder coat to RAL 9005”).
- GD&T callouts — if you use geometric dimensioning and tolerancing, ensure datums and feature control frames are complete.
- Inspection criteria — specify whether FAI is required, what sampling plan applies, and which standard governs acceptance (e.g., AS9102, ISO 2768).
- Weld requirements — if welding is involved, specify weld type, size, and any applicable standard (e.g., AWS D1.1, ISO 5817).
Incomplete documentation forces the vendor to make assumptions. Those assumptions become change orders, and change orders become NRE.
Schritt 6 — Angebote mithilfe eines NRE-Scorecards vergleichen
If you are evaluating quotes from multiple vendors, comparing NRE line items side by side is essential. A lower per-part price paired with a higher NRE can cost more in the long run—especially at low volumes.
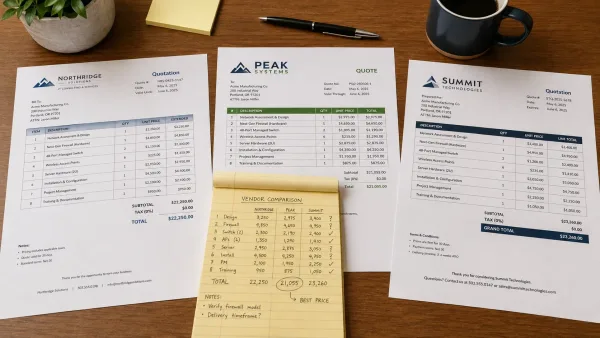
Three vendor quotes compared side by side — comparing NRE line items across vendors reveals differences in tooling strategy, hidden charges, and total project cost.
NRE Scorecard Framework
Use this framework to compare quotes on an equal basis:
| Evaluation Criteria | Vendor A | Vendor B | Vendor C |
|---|---|---|---|
| Total NRE ($) | |||
| Tooling breakdown (itemized?) | Yes / No | Yes / No | Yes / No |
| Soft tooling option offered? | Yes / No | Yes / No | Yes / No |
| NRE amortization plan available? | Yes / No | Yes / No | Yes / No |
| Hidden charges identified? | List: | List: | List: |
| Material sourcing included in NRE? | Yes / No | Yes / No | Yes / NRE |
| FAI / documentation charges included? | Yes / No | Yes / No | Yes / No |
| Total project cost (NRE + parts) | $ | $ | $ |
Common Pitfalls When Comparing Quotes
- Low NRE, high per-part price — some vendors shift NRE into per-part pricing. Calculate total project cost (NRE + per-part × quantity) to compare fairly.
- Missing line items — if one vendor’s NRE is significantly lower, check whether they have omitted charges that other vendors include. Ask for a line-by-line breakdown.
- Different tooling strategies — one vendor may quote custom tooling while another quotes soft tooling. Ensure you are comparing equivalent tooling quality and lifespan.
The goal is not to find the cheapest NRE. It is to find the most transparent and appropriate NRE for your project’s volume, complexity, and quality requirements.
FAQs
Nächste Schritte
For the best results, use this checklist before you approve any tooling or NRE charge. A few minutes of review can save weeks of delays and thousands in unexpected costs. If you are planning a low-volume sheet metal project and want a second set of eyes on your quote, our engineering team can provide a DFM and NRE review within 24 hours.