Vollständiger Leitfaden für elektrogalvanisierten Stahl (EG)
Ideal für sichtbare Blech-
und Metallteile
Geeignet zum Biegen
und Stanzen
Hervorragende Basis für Pulver-
beschichtung und Lackierung
Elektrolytisch verzinkter Stahl: Die Grundlagen
Elektroverzinkter Stahl, oft bezeichnet als EG oder EGI, wird typischerweise hergestellt unter Verwendung von kaltgewalztem Stahl als Substrat, mit einer Zinkbeschichtung, die durch ein elektrolytisches Abscheideverfahren. aufgebracht wird. EG bezieht sich speziell auf die Elektroplattierung mit Zink als Beschichtungsmaterial, und es wird weit verbreitet in Anwendungen eingesetzt, die eine verbesserte Korrosionsbeständigkeit erfordern. Die abgeschiedene Beschichtung liegt üblicherweise im Bereich von 5–20 μm , ist aber hochgradig gleichmäßig und weist eine geringe Porosität.
auf. Da die Zinkbeschichtung auf elektrogalvanisiertem Stahl relativ dünn, präzise gesteuert und glatt ist, bewahrt sie einen Großteil der ursprünglichen Oberflächentextur des kaltgewalzten Substrats. Das macht sie besonders geeignet für Komponenten mit strengen Anforderungen an das Erscheinungsbild.
Der Unterschied zwischen EG und “allgemeiner Elektroplattierung” besteht darin, dass die Zielanwendung viel spezifischer ist. Allgemeine Elektroplattierung kann auf eine breite Palette von Materialien angewendet werden, während elektrogalvanisierter Stahl sich speziell auf Zink-Elektroplattierung auf Stahlblech. bezieht. Mit anderen Worten, Elektrogalvanisierung ist ein spezifisches Verfahren innerhalb der breiteren Kategorie der Galvanisieren.
Kernmaterialeigenschaften von elektrogalvanisiertem Stahl (EG)
Normen und Gütesysteme für elektrogalvanisierten Stahl (EG)
Verschiedene Länder und Regionen haben eigene Normen für elektrogalvanisierten Stahl (EG). entwickelt. Obwohl sich die Systeme in Namenskonventionen und Gütebezeichnungen unterscheiden, sind sie in ihrer Struktur weitgehend ähnlich. Die am häufigsten verwendeten Normen, Namensformate und Güten sind unten aufgeführt.
Vergleich gängiger Normensysteme und Bezeichnungen
| Normensystem | Gängiges Bezeichnungsformat | Typische Güten / Beispiele | Anwendungshinweise |
|---|---|---|---|
| JIS G 3313 (Japan) | SECC, SECD, SECE, usw. | SECC (Allgemeine Verwendung), SECD (zum Stanzen), SECE (zum Tiefziehen) | Basierend auf kaltgewalzten Stahlsubstraten wie SPCC, SPCD und SPCE; weit verbreitet in Haushaltsgeräten, Büroausstattung und Automobil-Stanzteilen |
| EN 10152 (Europa) | DC01+ZE, DC03+ZE, DC04+ZE, usw. | DC01+ZE (allgemeine Kaltumformung), DC03+ZE (Tiefziehen), DC04+ZE (extratiefes Tiefziehen) | Basierend auf kohlenstoffarmem kaltgewalztem Stahl der DC-Serie; ZE kennzeichnet eine elektrogalvanische Zinkbeschichtung |
| ASTM A879/A879M (U.S.) | ZE coating, with coating mass expressed in g/m² | ZE 20/20, ZE 40/40 (equal coating); ZE 30/60 (differential coating) | Used where coating mass on each side must be specified; the coating is smooth and free of visible spangle |
| GB/T 15675 (China) | DC01+ZE, DC03+ZE, etc. | DC01+ZE, DC03+ZE, DC04+ZE | Closely aligned with the EN system; ZE indicates a pure zinc coating, while ZN indicates a zinc-nickel alloy coating |
Common Grades and Formability Levels
| Güte | Typische Verwendung | Umformbarkeit | Typische Anwendungen |
|---|---|---|---|
| SECC / DC01+ZE | General forming and simple stamping | Norm | Appliance housings, office equipment covers, internal brackets, general structural parts |
| SECD / DC03+ZE | Stamped parts | Gute | Appliance panels, office equipment housings, general stamped components |
| SECE / DC04+ZE | Tiefgezogene Teile | Very good | Appliance inner liners, automotive inner panels, complex deep-drawn parts |
| SECF / DC05+ZE | Extra deep-drawn parts | Ausgezeichnet | Deep-drawn appliance housings, complex automotive inner panels |
| SECIF / DC06+ZE | Special deep-drawn parts | Ausgezeichnet | Automotive outer panels, high-appearance parts requiring complex forming |
Hinweis: Designations such as SECC, SECD, and SECE do not indicate different coating types. They identify different formability grades und application categories. The base material is SPCC, SPCD, or SPCE, which correspond to the JIS G 3141 standard for cold-rolled steel.
How Electro-Galvanized Steel (EG) Differs from Cold-Rolled Steel and Hot-Dip Galvanized Steel
Put simply, EG, CR, and HDG represent a range of material options that run from no corrosion protection, to heavy-duty corrosion protection, to a more balanced combination of high surface quality und moderate corrosion resistance.
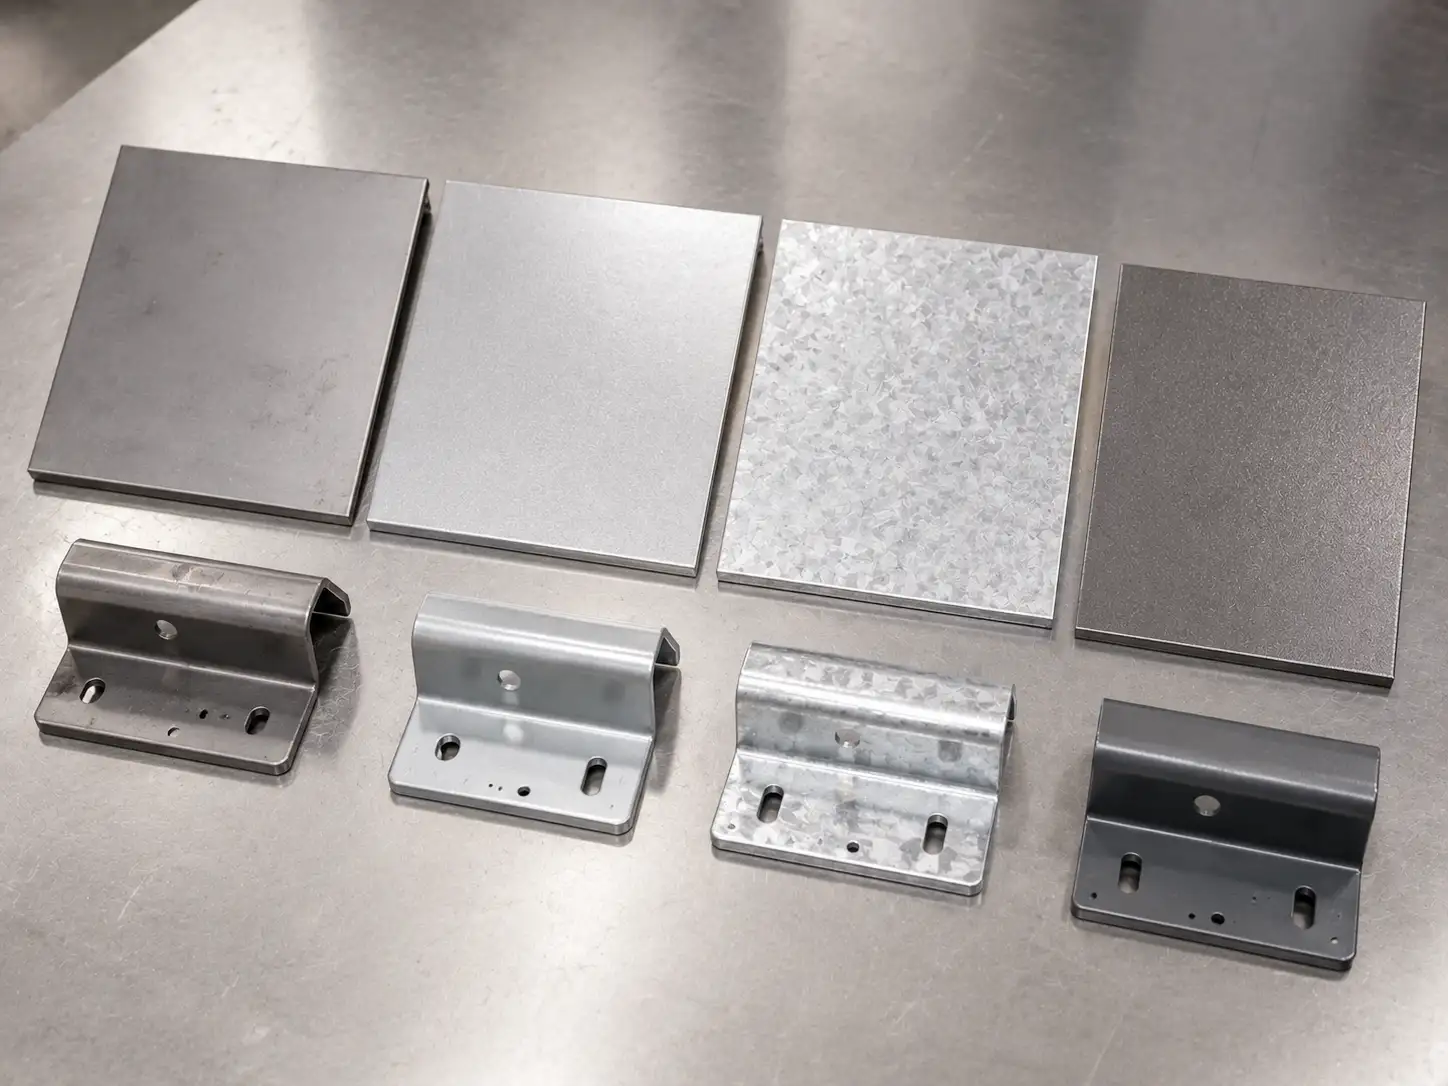
Comparison Table: EG, CR, and HDG
| Materialtyp | Oberflächenqualität | Korrosionsbeständigkeit | Umformbarkeit | Schweißbarkeit | Paintability | Typische Anwendungen |
|---|---|---|---|---|---|---|
| CR Cold-Rolled Steel | High, with a clean and smooth surface | Low, requires additional rust protection | Gute | Weldable under normal conditions | Can be coated, but the pre-treatment and corrosion protection system must be fully built out | Indoor parts, fully painted components, cost-sensitive applications |
| EG Electro-Galvanized Steel | Very high, with a uniform coating | Mäßig, better than CR | Good to very high, with grades available for deep drawing | Well suited to spot welding and laser welding, though parameters must be controlled | Very paint-friendly, ideal for powder coating, painting, and visible parts | Home appliances, office equipment, electronic enclosures, visible panels, inner and outer equipment panels |
| HDG Hot-Dip Galvanized Steel | Fair to good, though ultimate surface appearance is not usually the main priority | Hoch, with stronger long-term corrosion protection | Depends on the grade and coating weight | Weldable, but the process window differs from EG | Can be coated, but fine surface preparation is often needed for high-appearance finishes | Construction, structural parts, humid environments, long-term exposed applications, heavy-duty corrosion protection scenarios |
Surface Conditions and Post-Treatment Options for Electro-Galvanized Steel (EG)
Common EG Surface Conditions and Typical Applications
| Surface Condition / Post-Treatment | Function | Suitable for Painting or Coating | Typische Anwendungen |
|---|---|---|---|
| Passivierung | Provides temporary protection and reduces the risk of Weißrost | Generally acceptable as a pre-treatment condition for later processes | Standard storage and transportation, general equipment parts |
| Chrome-free / Cr-VI-free passivation | Provides similar temporary protection while meeting environmental compliance requirements | Depends on the downstream coating system, but is usually more coating-friendly | Home appliances, electronic equipment, and projects with stricter environmental requirements |
| Oiling | Improves protection during storage and transport, while also enhancing forming lubrication | Usually requires degreasing before painting | Stamped parts, general storage and transportation |
| Phosphatieren | Improves temporary resistance to white rust and provides a better bonding base for organic coatings | Ja | Powder-coated parts, painted parts, appearance components |
| Phosphating + passivation + oiling | Provides stronger storage and transport protection while also supporting formability | Still depends on the downstream coating system | Projects with longer supply chain cycles or more demanding transportation conditions |
Hinweis: A phosphate layer can serve as an effective bonding base for subsequent organic coatings, while also providing temporary protection against Weißrost during storage and transportation.
In der Blechfertigung, elektrogalvanisierten Stahl (EG) is a very commonly used material—and for many applications, an especially practical one. Most forming processes commonly used for bare steel sheet are also suitable for EG, and it performs particularly well in Tiefziehen. That said, factors such as tool condition, lubrication, und surface cleanliness still have a major impact on processing results, so proper process control remains essential.
Common EG Fabrication Processes and Key Control Points
| Verfahren | Process Compatibility | Häufige Probleme | Control Recommendations |
|---|---|---|---|
| Laserschneiden | Gute | Exposed cut edges, insufficient edge protection after localized heating | Consider it together with the downstream painting or edge-sealing strategy |
| CNC punching / stamping | Good to very high | Scratches, indentations, localized tearing, die pickup | Pay close attention to lubrication, tool condition, und matching the right material grade |
| Biegen | Gute | Surface damage on the outer bend radius, springback control | Plan the direction of visible surfaces and use protective film or pads where needed |
| Deep drawing | Fairly good to high | Surface damage under extreme forming conditions, narrower process window | Choose a higher-formability grade and validate both lubrication and tooling |
| Spot welding / resistance welding | Gute | Weld inconsistency, spatter, reduced electrode life | Adjust welding current and maintain electrodes with regular dressing |
| Pre-treatment before powder coating / painting | Essential | Direct painting may cause unstable adhesion or inconsistent appearance | Determine the required degreasing, phosphating, or other pre-treatment based on the supplied surface condition |
Typical Applications for elektrogalvanisiertem Stahl (EG)
Because of its strong overall performance, elektrogalvanisierten Stahl (EG) is widely used in the following industries and product categories:
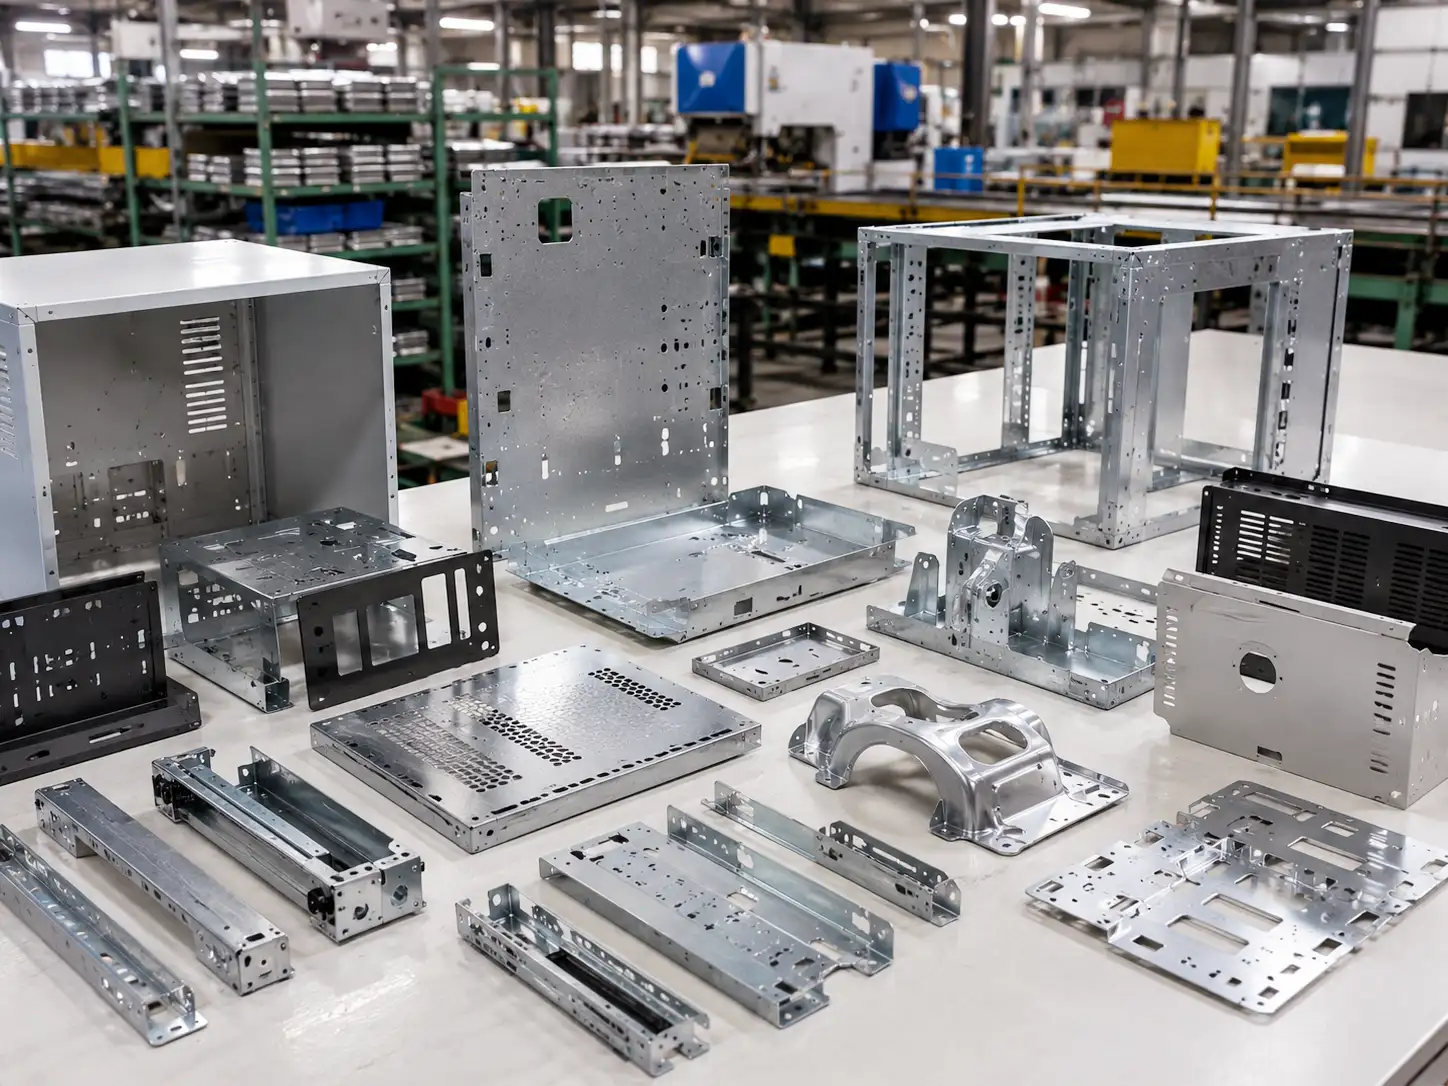
Application Scenarios and Recommended Material Selection Logic
| Anwendung | Oberflächenanforderung | Corrosion Requirement | Is EG Recommended? | Grund |
|---|---|---|---|---|
| Appliance housings (visible surfaces) | Hoch | Mäßig | Empfohlen | Smooth surface, well suited to painting, and sufficient corrosion resistance for indoor use |
| Automotive inner panels (non-visible parts) | Mäßig | Mäßig | Empfohlen | Good formability, good weldability, and corrosion resistance suitable for interior vehicle components |
| Office equipment housings | Hoch | Mäßig | Empfohlen | Excellent paint compatibility with a good balance of appearance and corrosion resistance |
| Outdoor structural parts | Mäßig | Hoch | Not recommended (HDG is a better choice) | EG has a thinner coating and does not provide enough long-term corrosion protection for outdoor exposure |
| Equipment used in high-humidity environments | Mäßig | Relatively high | Use with caution (enhanced post-treatment is required) | Can be used if passivation and coating are properly applied; otherwise HDG should be considered |
| Complex deep-drawn parts (such as appliance inner liners) | Mäßig | Mäßig | Empfohlen | Excellent formability, especially suitable for Tiefziehen applications |
How to Choose the Right elektrogalvanisiertem Stahl (EG) for Your Project
When reviewing a new project, material selection should be evaluated across five key factors:
service environment → appearance requirements → fabrication method → cost target → delivery requirements
EG Material Selection Guide
| Project Condition | Material Recommendation | Is EG or Another Material More Suitable? | Hinweise |
|---|---|---|---|
| Dry indoor environment, standard appearance requirements | CR or EG | EG is the better option | EG offers better corrosion resistance than CR, with moderate cost |
| Indoor humid environment with some corrosion-resistance requirements | EG | EG | EG provides better corrosion resistance than CR, while costing less than HDG |
| Outdoor exposure or heavily corrosive environment | HDG / zinc-aluminum-magnesium | EG is not recommended | EG has a thinner coating and does not offer sufficient long-term corrosion resistance outdoors |
| High appearance requirements with painting or coating | EG | EG | Smooth surface and good coating adhesion make it ideal for painted parts |
| Deep drawing or complex stamping | EG | EG | The thin coating has minimal effect on formability, and EG performs well in deep-drawing applications |
| Simple bending, low-strength parts | CR or EG | EG is the better option | EG provides better corrosion resistance while still keeping cost under control |
| High-strength structural parts (thick gauge) | HDG or structural steel | EG is not recommended | EG is typically used for thin sheet; thicker structural applications are usually better suited to HDG |
| Limited budget, short service life | CR | CR is more suitable for short-term use | If budget is tight and the operating environment is dry, CR can be a practical choice |
Common Issues Often Overlooked in Procurement and Drawing-Based Custom Manufacturing
In real-world projects, the following issues are often overlooked, which can lead to quality problems oder fit-up issues after delivery:
It is strongly recommended that the technical agreement und drawings clearly specify the following: material grade, coating weight, surface condition, appearance grade, post-treatment requirements, packaging, and storage/transport conditions.